Municipal Sewage Sludge Carbonization Feasibility: Heavy Metal Treatment, Moisture Requirements, and End-Product Utilization
Municipal sewage sludge carbonization is a potential solution for reducing sludge volume, recovering carbon-rich materials, and improving waste management efficiency. However, its feasibility depends on several critical factors, including heavy metal behavior, feedstock moisture content, energy consumption, and the final destination of the carbonized product. Before investing in a carbonization project, operators need to evaluate both technical performance and environmental compliance.
1. How Does Municipal Sewage Sludge Carbonization Work?
Municipal sewage sludge is generated during wastewater treatment and typically contains organic matter, inorganic minerals, water, and potentially hazardous contaminants. Carbonization uses controlled heating under oxygen-limited conditions to convert part of the organic matter into a carbon-rich solid product.
Compared with conventional disposal methods, carbonization can reduce the volume of sludge requiring further management and may recover useful energy from volatile compounds. Depending on the feedstock and operating conditions, the process can also produce combustible gases and condensable vapors that require appropriate collection and treatment.
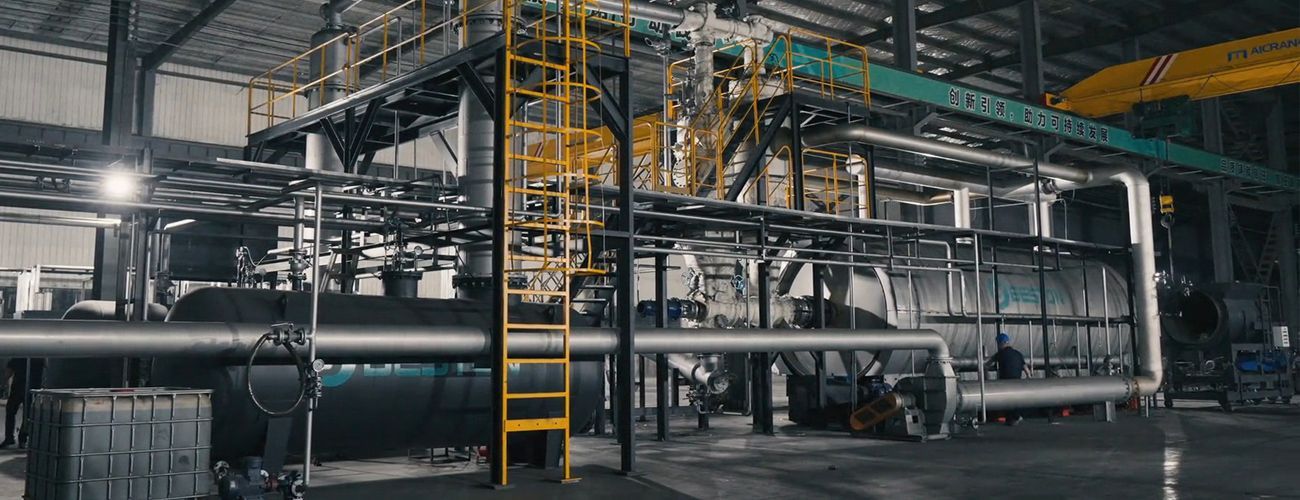
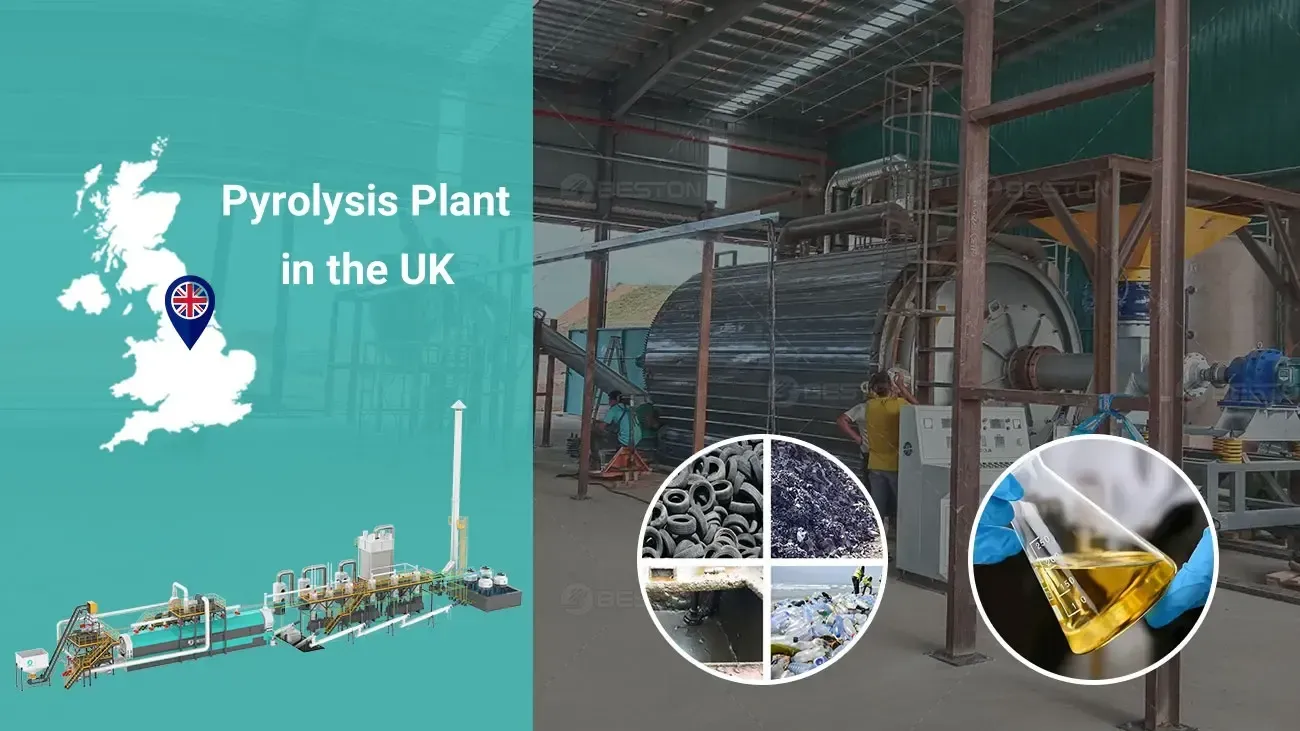
A complete sewage sludge treatment plant may include sludge dewatering, drying, carbonization, gas treatment, and product handling systems. Integrating these processes helps improve operational stability and provides a clearer basis for evaluating overall project economics.
2. Heavy Metal Treatment: A Critical Feasibility Factor
Heavy metals are one of the main concerns when converting municipal sewage sludge into carbonized products. Sludge may contain lead, cadmium, chromium, mercury, nickel, copper, and zinc, depending on the wastewater sources and treatment processes.
Carbonization does not automatically eliminate heavy metals. Many metals remain in the solid residue, and their concentrations may increase as organic matter and water are removed. Changes in temperature and chemical composition can also affect metal speciation, mobility, and leachability. Certain volatile elements, particularly mercury and some metal compounds, may transfer into the gas phase and require effective emission controls.
Therefore, feasibility studies should include several important measures.
- Feedstock testing: Analyze representative sludge samples for total heavy metal concentrations and other relevant contaminants.
- Process evaluation: Assess how carbonization temperature, residence time, and feedstock composition influence contaminant distribution.
- Emission control: Design suitable gas collection, particulate removal, and exhaust treatment systems based on the expected pollutants.
- Product testing: Evaluate heavy metal concentrations, leaching characteristics, and compliance with the intended end-use standards.
If the carbonized product is intended for agricultural use, soil improvement, or other beneficial applications, compliance must be demonstrated under the applicable local regulations. If contaminant levels exceed permitted limits, controlled disposal or further treatment may be necessary.
3. What Moisture Content Is Required Before Carbonization?
Moisture content directly affects the energy demand and operating cost of sludge carbonization. Fresh municipal sewage sludge often contains substantial amounts of water, making direct thermal treatment energy-intensive. A large proportion of the available heat may otherwise be consumed by water evaporation rather than by the carbonization process.
Mechanical dewatering is generally the first step in reducing moisture content. Equipment such as filter presses or centrifuges can remove part of the water before thermal drying. A drying system can then reduce the moisture level to a range suitable for the selected carbonization equipment.
There is no universal moisture requirement for every project. The appropriate inlet moisture content depends on reactor design, feedstock characteristics, heat source, and the availability of waste heat. Many thermal carbonization systems benefit from drying sludge to approximately 10%–20% moisture before feeding, but this range should be confirmed with equipment specifications and process testing.
Feasibility calculations should compare the energy required for drying with the recoverable energy from process gases and other available heat sources. Waste heat recovery, efficient insulation, and automated temperature control may reduce operating costs. However, the energy balance must be calculated using actual sludge properties rather than theoretical assumptions alone.
4. Where Can the Final Carbonized Product Go?
The commercial value of municipal sludge carbonization depends heavily on whether the final product has a safe and legally acceptable destination. Potential pathways include the following.
- Construction materials: Subject to technical testing and regulatory approval, treated sludge-derived solids may be evaluated as components in selected building materials.
- Land application: Agricultural or soil-related use requires strict assessment of heavy metals, organic contaminants, stability, and applicable product standards. Carbonization alone does not establish suitability.
- Industrial applications: Certain products may be considered for mineral-based or carbon-containing industrial uses if their properties meet the required specifications.
- Controlled disposal: Material that fails safety or quality requirements may need to be managed at an authorized disposal facility.
Before selecting a destination, project developers should consult potential end users and regulatory authorities. Product testing should cover not only contaminant levels but also relevant physical and chemical properties, such as calorific value, ash content, and stability.
5. How to Evaluate Project Feasibility
A reliable feasibility study should combine technical, environmental, and financial assessments. Key inputs include daily sludge throughput, initial and target moisture content, organic matter content, heavy metal concentrations, energy prices, and local disposal fees.
Capital expenditure should account for dewatering and drying equipment, the carbonization reactor, exhaust treatment, material handling, and safety systems. Operating costs should include electricity, supplementary fuel, maintenance, laboratory testing, and residue management. Revenue from recovered energy or carbonized products should only be included when supported by realistic market demand and regulatory approval.
Pilot testing is particularly valuable when sludge composition varies significantly or when the intended product has strict quality requirements. It helps verify drying performance, energy consumption, contaminant behavior, product quality, and the suitability of the proposed treatment process.
Conclusion
Municipal sewage sludge carbonization can offer a practical route for sludge volume reduction and resource recovery, but it is not automatically a safe or profitable solution. Heavy metal behavior, moisture control, energy efficiency, and final product utilization must be assessed together. By conducting feedstock analysis, process testing, environmental evaluations, and market research before investment, project developers can make better-informed decisions and establish a treatment system that meets local requirements.