Sludge Oil Recycling Pyrolysis Plant
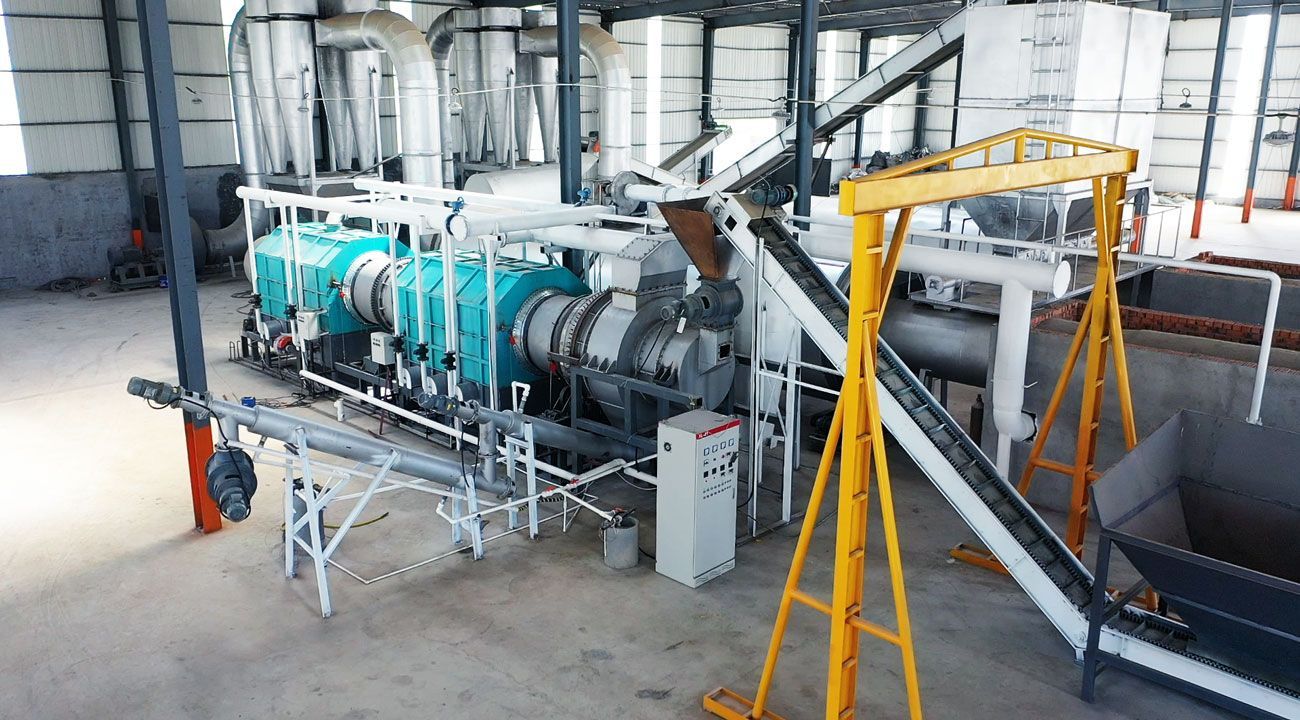
A sludge oil recycling plant
is one of those purchases which takes any business to new heights. It's about knowing which to obtain and paying the correct amount for doing it. This is one of the best plants in the marketplace, and you might get it to get a fair rate.
Exactly what are the causes of this being a heralded option?
Let's have a look for those who need to enhance their facility and need to ensure it really is a great option based upon their underlying business requirements. This may fit these and this is why.
Powerful: The energy you will need while producing oil is probably the details that could often go missed. You don't want a plant that is certainly getting in how as it cannot generate enough power. The key reason why you are likely to wish to use this plant offers quite a bit concerning the ability that is certainly offered. It is going to generate ample, and you will enjoy the value which comes out of it ultimately.
The strength will probably woo you together with is actually a significant plus point.
Safe: Safety factors are something you will need with a plant that is certainly producing oil. You are not going to learn that to become problem here simply because this is one of the safest pyrolysis plants
on the market. You are going to realize it is certified and prepared to use the moment it is put for the test. It will almost certainly hold up well and take part in the part it must. For individuals who want to generate enough oil and make sure it doesn't boil over should have this option set up.
An easy task to Operate: This really is a plant that will be simple to function, that is critical when you are longing for substantial results in the facility. Nobody wants a plant that will occupy efforts and not work efficiently as a result of how hard it really is to operate. This may be frustrating at one time where it is centered on pacing things and ensure you are moving along with a fair pace. People who don't aim to achieve this are the types who hate their setup and don't see results.
The oily sludge treatment plant
is amongst the biggest and finest investments an individual may make. You are likely to see significant value as a result, and it is gonna still do well in the long-term. You will are aware of the oil will work in your favor and yes it will be as pure as you want it to be. Other solutions usually are not able to take care of this, and that may be annoying. However, this is the ideal plant then one you may put your unwanted weight behind due to advantages it gives you.
Emission treatment is an essential component of a coconut shell charcoal machine, particularly when carbonization operates at commercial scale. Thermal decomposition of coconut shells generates particulate matter, condensable vapors, and combustible gases that require appropriate collection, treatment, or controlled combustion. The composition and volume of these emissions depend on feedstock moisture, carbonization temperature, reactor configuration, and operating conditions. An effective treatment system must address each emission stream while maintaining thermal efficiency, operational safety, and compliance with applicable environmental requirements. Dust Collection During Feedstock Handling and Charcoal Discharge Dust can arise during coconut shell crushing, screening, conveying, carbonization residue handling, and finished charcoal packaging. Fine particles may become airborne during material transfer, creating housekeeping challenges and increasing the risk of dust accumulation around mechanical equipment. Source capture is generally more effective than relying exclusively on general ventilation. Enclosed conveyors, covered transfer points, and appropriately positioned extraction hoods can limit the dispersion of particulate matter. Depending on particle characteristics and gas conditions, cyclones or bag filters may be incorporated into the dust collection system. Cyclones separate particles through centrifugal force and are often used as a preliminary collection stage. Bag filters capture finer particulates by passing gas through porous filter media. Their suitability depends on gas temperature, humidity, particle loading, and the potential presence of combustible dust. Several operating considerations are important: Temperature control: Gas entering a filter must remain within the filter media's permissible temperature range. Moisture management: Excessive humidity can cause particle agglomeration or filter blinding. Pressure-drop monitoring: Increasing pressure drop may indicate dust accumulation or restricted airflow. Fire prevention: Charcoal fines and hot particles require appropriate isolation, housekeeping, and fire-protection measures. Dust collection equipment should be selected according to the actual gas stream. Hot, dust-laden process gas may require cooling or preliminary separation before fine filtration. Managing Pyrolysis Vapors and Condensable Compounds During carbonization, the organic constituents of coconut shells decompose and release vapors containing water vapor and various organic compounds. As these vapors cool, some components condense into liquid fractions, while others remain gaseous. The vapor-treatment arrangement must account for this changing composition. In systems designed to recover condensable products, heat exchangers or condensers lower the vapor temperature, allowing suitable compounds to be separated from the gas stream. The resulting liquids may contain mixtures of water and organic substances, depending on the process configuration and feedstock characteristics. Uncondensed gases require further management. Sending untreated vapor directly to the atmosphere can result in odorous emissions and the release of organic pollutants. A properly engineered system may route combustible non-condensable gases to a controlled combustion chamber, provided that the gas composition, heating value, and operating conditions are suitable. Condensation performance depends on cooling capacity, gas flow, temperature, and the properties of the vapor mixture. Fouling can reduce heat-transfer efficiency, while inadequate condensate drainage may impair separation. Routine inspection and accessible cleaning arrangements are therefore important design considerations for a coconut shell charcoal machine . Combustion Gas Treatment and Heat Utilization Combustion gases are generated when fuel or recovered combustible gas is burned to provide process heat. Their composition depends on the fuel, combustion temperature, oxygen availability, burner design, and operating stability. Potential pollutants include particulate matter, carbon monoxide, nitrogen oxides, and other compounds associated with the feedstock and combustion conditions. Sulfur-containing compounds may also require consideration where relevant to the incoming material. Combustion control is the first line of emission management. Adequate mixing, appropriate residence time, sufficient oxygen, and stable temperature help promote more complete oxidation of combustible compounds. Secondary treatment may be necessary to meet site-specific emission limits. Depending on the measured emissions and applicable regulations, the treatment train may include particulate filtration, wet scrubbing, or other pollutant-specific controls. Wet scrubbers can remove certain soluble gases and particulates, but they generate wastewater that must be managed appropriately. Heat recovery can improve the thermal efficiency of a coconut shell charcoal machine. Suitable exhaust heat may be used for feedstock drying or combustion-air preheating, subject to temperature constraints, corrosion risks, and the requirements of the emission-control system. Heat recovery should not compromise adequate combustion or downstream pollutant removal. Monitoring and Integrated System Design Emission treatment performs most reliably when collection, condensation, combustion, and exhaust purification are designed as an integrated system. Poor coordination can create pressure fluctuations, inadequate gas flow, excessive condensation in unsuitable locations, or unstable burner operation. Temperature sensors, pressure gauges, gas-flow measurements, and periodic exhaust testing help operators identify deviations. Monitoring should focus on parameters relevant to the actual process and local environmental requirements. Maintenance schedules should address filter cleaning, condenser inspection, condensate removal, and combustion-system verification. Ultimately, emission management for a coconut shell charcoal machine requires more than installing a single filtration device. Dust, condensable vapors, and combustion gases have different physical and chemical properties, so each stream needs an appropriate treatment strategy. A coordinated design can reduce uncontrolled emissions, support stable carbonization, improve heat utilization, and strengthen the plant's environmental performance.
Recovered carbon black (rCB) is emerging as a valuable material in the tire recycling industry. Produced during waste tire pyrolysis, raw carbon black contains carbonaceous residues, inorganic ash, residual oils, and sulfur-containing compounds. In its untreated form, this material often has inconsistent quality and limited applications, resulting in a lower market value than virgin commercial carbon black. However, through grinding, classification, pelletizing, and appropriate purification or surface modification, recovered carbon black can be upgraded into a more consistent industrial filler for rubber and plastic products. 1. Why Raw Carbon Black Has Limited Market Value During waste tire pyrolysis plant , rubber polymers decompose under oxygen-limited conditions, producing pyrolysis oil, non-condensable gas, steel wire, and a solid carbon-rich residue. This solid residue is commonly called raw pyrolysis char. Unlike virgin carbon black, which is manufactured under controlled conditions to achieve specific particle characteristics, raw pyrolysis char retains some of the original tire components. Its properties depend on the tire composition, pyrolysis temperature, residence time, and reactor design. Several factors limit its direct use in industrial manufacturing: High ash content: Silica, zinc compounds, and other inorganic residues from tire additives can reduce the proportion of usable carbon. Residual oil and volatile matter: Incomplete removal of organic compounds can affect processing behavior and product consistency. Sulfur-containing compounds: Sulfur originating from tire vulcanization may remain in the recovered material and influence certain applications. Uneven particle size: Agglomerated particles and coarse residues can cause dispersion problems in rubber compounds. Variable reinforcing performance: Surface chemistry, aggregate structure, and particle characteristics may differ substantially from those of virgin carbon black. These limitations explain why raw carbon black generally sells at a discount. To unlock its commercial potential, producers must focus on improving material quality rather than simply increasing the amount of char recovered from each ton of waste tires. 2. Grinding and Classification Improve Material Consistency Grinding is one of the first steps in upgrading raw pyrolysis char. The objective is to reduce oversized particles, break down agglomerates, and produce a more uniform powder suitable for downstream processing. Industrial milling systems can include impact mills, pin mills, or other grinding equipment selected according to the characteristics of the feed material. Classification equipment separates particles according to size, helping manufacturers maintain consistent product specifications. However, finer grinding does not automatically produce better reinforcing performance. Carbon black's behavior in rubber also depends on aggregate structure, surface area, surface chemistry, and dispersion. Excessive grinding can increase energy consumption without delivering a proportional improvement in final product performance. Magnetic separation and screening may also be necessary to remove residual steel fragments and coarse contaminants before milling. For commercial production, particle size distribution should be monitored alongside ash content, moisture, and other relevant properties. These measurements help establish repeatable product quality and reduce the risk of inconsistent performance during compounding. 3. Pelletizing Improves Handling and Transportation Fine recovered carbon black powder can create dust during conveying, storage, and feeding. It may also have poor flowability, making accurate dosing more difficult in industrial production lines. Pelletizing addresses these handling problems by compressing or agglomerating the powder into small granules. Depending on the formulation and intended application, the process may use water, binders, or other processing aids. The main benefits include: Reduced dust generation during handling. Improved flowability and feeding consistency. Easier storage, packaging, and transportation. More convenient integration into automated rubber and plastic compounding systems. Pellet quality is important. Pellets that are too hard may disperse poorly during mixing, while those with insufficient strength may break apart and generate dust. Binder selection and dosage must also be controlled because they can affect moisture content, mixing behavior, and the properties of the finished compound. Pelletizing primarily improves handling characteristics. It does not independently remove ash, reduce sulfur content, or guarantee that recovered carbon black meets a particular industrial grade. 4. Purification and Modification Increase Commercial Value After physical processing, additional treatments may be required to improve the chemical and functional properties of recovered carbon black. De-oiling and volatile matter removal Residual organic compounds can be reduced through suitable thermal treatment, extraction, or other purification processes. The appropriate method depends on the initial char composition and the target product specifications. Better control of volatile matter can improve product consistency, although treatment conditions must be carefully selected to avoid unnecessary energy consumption or changes to desirable carbon characteristics. Ash reduction and desulfurization Ash reduction can involve chemical treatment, washing, or other separation methods. Desulfurization may use thermal, chemical, or combined processes, depending on the sulfur compounds present. These treatments can improve the suitability of recovered carbon black for selected applications, but they also introduce additional costs and potential environmental challenges. Chemical treatment may generate wastewater or secondary residues that require appropriate management. Producers should evaluate the improvement in product performance against the costs of reagents, energy, wastewater treatment, and material losses. Surface modification Surface treatment can alter the interactions between recovered carbon black and the surrounding polymer matrix. Depending on the treatment, it may improve compatibility, dispersion, or selected mechanical properties. The best modification strategy should be determined through laboratory testing and application-specific trials rather than assumed to work equally well for every recovered carbon black product. 5. Can Recovered Carbon Black Replace N330 or N660? Recovered carbon black can replace part of the virgin carbon black used in certain rubber compounds, but substitution depends on the application and the quality of the recovered material. N330 is commonly used in tire treads and other applications requiring relatively strong reinforcement. N660 is generally associated with lower reinforcement and lower hysteresis requirements than N330 in many rubber formulations. These grades have defined performance characteristics. Matching their particle size alone is insufficient because reinforcing behavior also depends on surface area, structure, surface chemistry, and dispersion. A practical evaluation should consider: Iodine adsorption or other surface-area indicators. Oil absorption or structure-related measurements. Ash, sulfur, moisture, and volatile matter. Particle size distribution and dispersion quality. Tensile strength, elongation, hardness, abrasion resistance, and other application-specific properties of the finished compound. Rather than claiming that all recovered carbon black can directly replace N330 or N660, manufacturers should establish substitution ratios through controlled trials. In some formulations, rCB may partially replace virgin carbon black while maintaining acceptable performance. Other demanding applications may require additional purification, modification, or blending with virgin grades. 6. Applications in Rubber and Plastic Manufacturing The commercial opportunities for upgraded recovered carbon black extend beyond tire recycling. In rubber products, potential applications include conveyor belts, rubber mats, hoses, molded components, and selected automotive rubber parts. The appropriate use depends on mechanical requirements, product safety standards, and the consistency of the recovered material. In plastics, recovered carbon black may be incorporated into selected masterbatches and polymer compounds where its color, dispersion, contamination level, and processing behavior meet customer specifications. Testing is especially important for products requiring consistent appearance, electrical performance, or stringent mechanical properties. Market entry generally begins with less demanding applications before progressing toward products requiring higher reinforcement and tighter quality control. Conclusion Recovered carbon black offers tire pyrolysis operators an opportunity to move beyond selling low-value raw char. Grinding and classification improve physical consistency, pelletizing facilitates handling, and targeted purification or surface modification can expand the range of potential applications. The key to commercial success is not simply producing more recovered carbon black, but developing a consistent material that meets measurable customer requirements. By combining appropriate post-processing equipment, quality control, and application-specific testing, producers can improve product value, reduce dependence on virgin raw materials, and strengthen the economics of waste tire pyrolysis.
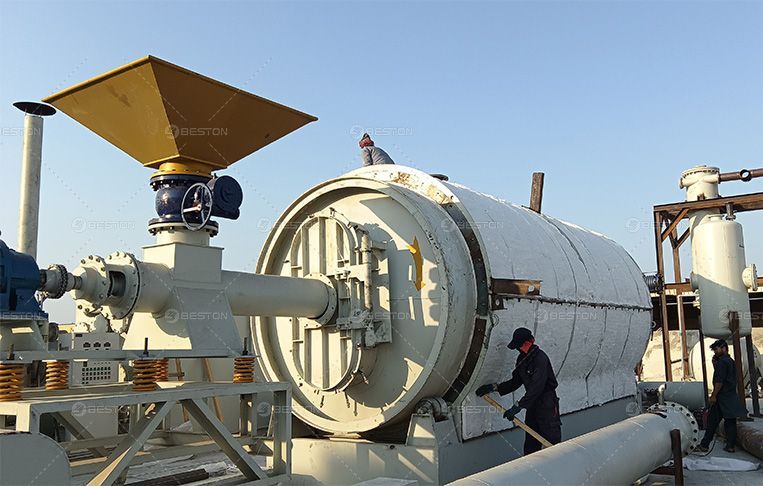
Water management is a critical engineering consideration in an oil sludge pyrolysis project. Cooling systems support vapor condensation, control equipment temperatures, and help maintain stable process conditions, while wastewater management addresses contaminated water generated during feedstock handling, gas condensation, and equipment cleaning. An effective design must balance thermal performance, water consumption, environmental protection, and operational reliability. These factors should be evaluated early when assessing an oil sludge pyrolysis plant for sale , because the cooling configuration and wastewater infrastructure can significantly influence installation requirements and operating costs. Cooling Circuit Design and Heat Transfer An oil sludge pyrolysis plant typically uses cooling equipment to condense pyrolysis vapors into liquid products and maintain suitable temperatures in downstream process equipment. Cooling-water circulation, heat-exchanger capacity, and temperature control directly affect condensation efficiency. A recirculating cooling circuit can reduce freshwater consumption by returning warmed water to a cooling tower, air cooler, or other heat-rejection system. The appropriate configuration depends on ambient conditions, available utilities, process heat loads, and local water availability. Heat exchangers must be sized according to the expected vapor flow rate, inlet temperature, condensation characteristics, and required outlet conditions. Undersized equipment may reduce liquid recovery, whereas poorly controlled cooling can contribute to unstable operation. Deposits, suspended solids, and scale can also impede heat transfer over time. Temperature sensors, flow meters, and pressure indicators help operators identify abnormal conditions. A decline in cooling-water flow, for example, may indicate pump deterioration, filter blockage, or a developing leak. Automated alarms can prompt corrective action before cooling performance deteriorates substantially. Water Quality and Cooling System Maintenance The quality of circulating water influences equipment longevity and thermal efficiency. Dissolved minerals can precipitate on heat-transfer surfaces, while suspended solids may accumulate in pipelines and strainers. Microbiological growth can also become a concern in cooling towers and other systems exposed to suitable environmental conditions. A water-treatment program should reflect the characteristics of the incoming water and the cooling-system design. Depending on these conditions, treatment may include filtration, scale control, corrosion inhibition, and microbiological management. Evaporation, drift, and blowdown contribute to water losses in cooling-tower systems. Blowdown removes a portion of circulating water to control the accumulation of dissolved solids. Its volume should be managed according to water chemistry and the applicable discharge or treatment requirements. Regular inspection is essential. Operators should monitor heat-exchanger performance, clean strainers, inspect pumps and seals, and assess corrosion at appropriate intervals. These measures help maintain predictable cooling capacity and reduce unplanned maintenance. Wastewater Sources and Contamination Risks Wastewater characteristics depend on the feedstock, process configuration, and operating practices. Potential sources include equipment washing, oily condensate, contaminated drainage, and water associated with certain gas-treatment or feedstock-preparation systems. Oil sludge may contain hydrocarbons, suspended solids, salts, and metals. Consequently, wastewater from associated operations should not be assumed suitable for direct discharge or reuse without characterization. A preliminary water balance helps identify each wastewater stream and estimate its expected volume. Separate collection is often beneficial because relatively clean cooling-tower blowdown may require a different treatment approach from oily process wastewater. Mixing all streams can increase treatment complexity and generate larger volumes of contaminated water. Segregation also helps prevent accidental releases and allows each stream to be managed according to its actual composition. Wastewater Treatment and Environmental Compliance Oily wastewater may require a combination of physical and chemical treatment processes. Depending on analytical results, these may include oil-water separation, settling, coagulation and flocculation, filtration, or additional treatment for dissolved contaminants. Free oil can often be removed through suitable separation equipment, but emulsified hydrocarbons may require more advanced treatment. Dissolved metals and other contaminants may also remain after conventional oil separation. Treatment should therefore be selected using representative wastewater samples and defined discharge or reuse targets. Parameters such as oil and grease, chemical oxygen demand, suspended solids, pH, and relevant metals may need to be monitored. Applicable regulatory limits vary by jurisdiction and discharge destination. Where feasible, treated water may be reused in appropriate non-contact applications, provided its quality meets the requirements of the intended use. Reuse can reduce freshwater demand, but contaminants must not accumulate to levels that compromise equipment or process stability. Evaluating Water Management When Selecting Equipment When comparing an oil sludge pyrolysis plant for sale, buyers should examine the complete water-management arrangement rather than focusing exclusively on the reactor and oil recovery system. Key considerations include: Cooling-water circulation capacity and expected makeup-water demand. Heat-exchanger specifications and cooling-system maintenance requirements. Identification and segregation of wastewater streams. Wastewater treatment capacity and sludge disposal arrangements. Instrumentation for flow, temperature, and water-quality monitoring. Provisions for leakage prevention, spill containment, and emergency drainage. Water availability, local discharge requirements, and site-specific wastewater characteristics should be established before finalizing the plant layout. Conclusion Effective water management integrates cooling-circuit design, water-quality control, wastewater segregation, and appropriate treatment technologies. For an oil sludge pyrolysis project, these systems help maintain condensation performance, protect equipment, and reduce environmental risks. Evaluating water requirements and wastewater treatment provisions during equipment selection provides a stronger basis for estimating operating costs and developing a reliable, environmentally responsible facility.
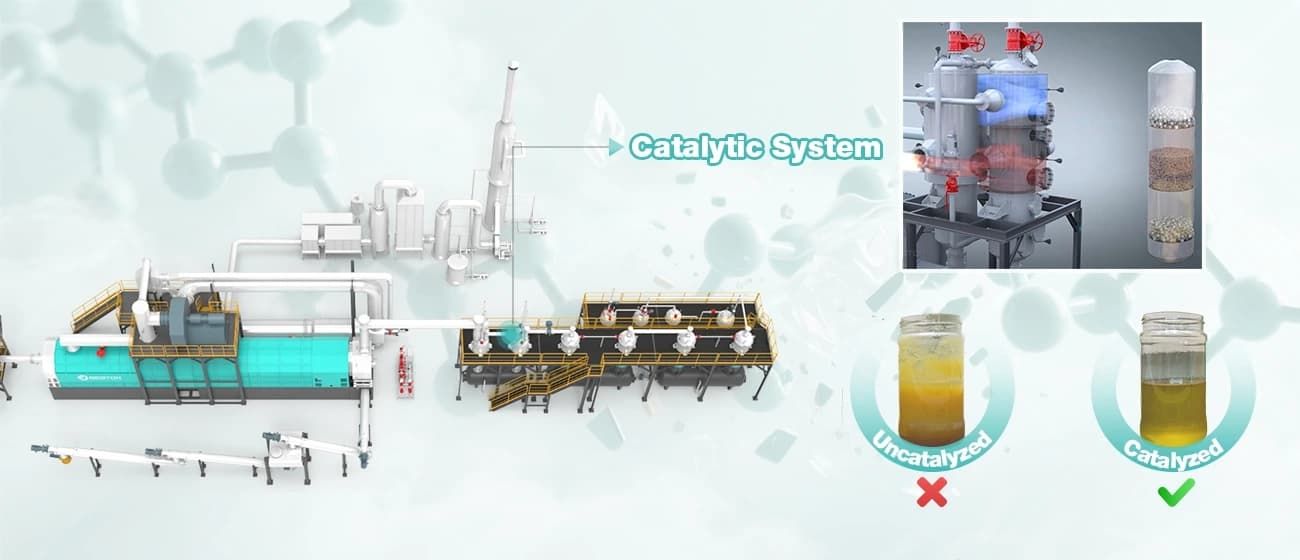
Plastic pyrolysis is an effective way to convert waste plastics into liquid oil, combustible gas, and solid residues. However, one common challenge in plastic pyrolysis is the formation of wax in the pyrolysis oil. High wax content can increase oil viscosity, cause blockages in pipelines, and complicate storage, transportation, and downstream refining. Catalytic pyrolysis offers a potential solution by promoting the breakdown of heavy hydrocarbon molecules into lighter compounds. By selecting suitable catalysts and optimizing operating conditions, plastic pyrolysis projects can improve oil fluidity and product quality. But how does catalytic pyrolysis work, and can it completely eliminate wax formation? 1. Why Does Plastic Pyrolysis Oil Contain Wax? Plastic pyrolysis involves heating plastics in an oxygen-free environment to break long polymer chains into smaller hydrocarbon molecules. The resulting products depend on the plastic type, reaction temperature, residence time, and reactor configuration. Polyethylene (PE) and polypropylene (PP) are particularly prone to producing waxy products because their molecular structures contain long hydrocarbon chains. When these polymers decompose, some of the resulting hydrocarbons remain relatively heavy and may condense into wax at lower temperatures. Several factors can contribute to wax formation: Low or insufficient reaction temperature: Some heavy hydrocarbons may not undergo sufficient cracking, leaving high-molecular-weight compounds in the product stream. Short vapor residence time: Heavy hydrocarbon vapors may leave the reactor before undergoing further thermal decomposition. Feedstock composition: PE and PP can produce substantial amounts of long-chain hydrocarbons under certain operating conditions. Cooling and condensation: Heavy hydrocarbons may condense or solidify as the vapor stream cools, causing wax accumulation in collection equipment and pipelines. Wax is not necessarily a contaminant introduced from outside the process. It is often a natural product of plastic decomposition. The challenge is controlling its formation and distribution to obtain oil with the properties required by the intended application. 2. How Does Catalytic Pyrolysis Reduce Wax Formation? Catalytic pyrolysis introduces a catalyst into the pyrolysis process to accelerate the breakdown of hydrocarbon molecules and influence product distribution. Unlike conventional thermal pyrolysis, which relies primarily on heat, catalytic pyrolysis uses active catalyst sites to facilitate additional cracking and other chemical reactions. This can help convert heavy hydrocarbons into lighter liquid hydrocarbons and non-condensable gases. Promoting the Cracking of Heavy Hydrocarbons Catalysts such as suitable zeolites, silica-alumina materials, and other catalytic formulations can promote the cracking of long-chain hydrocarbons into smaller molecules. For example, heavy hydrocarbon vapors generated from PE or PP may undergo further cracking before condensation. Under appropriate conditions, this can reduce the amount of heavy wax-forming compounds entering the oil collection system. Improving Hydrocarbon Product Distribution Catalysts can also change the relative proportions of different hydrocarbon fractions. Depending on the catalyst and process conditions, catalytic plastic pyrolysis machine may increase the production of lighter hydrocarbons, including gasoline-range compounds, while reducing heavy liquid fractions. However, stronger cracking does not always mean higher liquid oil yield. Some hydrocarbons may be converted into permanent gases, so the optimal catalyst depends on whether the project prioritizes liquid yield, oil fluidity, or a specific product composition. Reducing Wax-Related Operational Problems When catalytic cracking reduces the concentration of heavy hydrocarbons, the resulting oil may exhibit lower viscosity and improved flow characteristics. This can help reduce wax accumulation in downstream equipment. Nevertheless, the actual improvement depends on the feedstock, catalyst activity, reactor design, and temperature profile. Catalytic pyrolysis should therefore be evaluated through feedstock-specific testing rather than assumed to eliminate wax entirely. 3. Key Factors for Optimizing Catalytic Plastic Pyrolysis Adding a catalyst alone does not guarantee wax-free oil. Several process variables must be considered together. Catalyst selection: Different catalysts have different pore structures, acidity, cracking activity, and selectivity. Zeolite-based catalysts, for example, can promote the formation of lighter hydrocarbons, but excessive cracking may reduce liquid yield and increase gas production. Reaction temperature: Temperature influences both thermal and catalytic cracking. The appropriate range depends on the plastic feedstock, catalyst, and target products. Excessive temperatures can increase energy consumption and unwanted gas formation. Catalyst-to-feed ratio: The amount of catalyst affects contact between hydrocarbon vapors and active sites. An insufficient quantity may limit cracking, while excessive catalyst use can increase costs and complicate solids handling. Vapor residence time: Adequate contact time allows heavy hydrocarbons to undergo further cracking. However, overly severe cracking can shift valuable liquid products toward lighter gases. Condensation system design: Even when catalytic cracking reduces wax production, heavy compounds may remain. Proper temperature control, staged condensation, and appropriate pipeline heating can help prevent wax from solidifying in downstream equipment. 5. Is Catalytic Pyrolysis Oil Completely Wax-Free? Not necessarily. Catalytic pyrolysis can reduce wax formation, but the result depends on the catalyst, feedstock, and operating conditions. Some heavy hydrocarbons may remain in the oil, and wax may still form during cooling or storage. For projects requiring low-wax or wax-free oil, consider combining catalytic cracking with optimized condensation, filtration where appropriate, and downstream upgrading when necessary. Product testing should include viscosity, distillation characteristics, and relevant compositional analysis to determine whether the oil meets the intended application requirements. It is also important to distinguish between reducing wax formation inside the reactor and preventing wax deposition after the oil has been produced. These are related but different engineering challenges. Conclusion Wax formation is a common challenge in plastic pyrolysis, particularly when processing polyethylene- and polypropylene-rich feedstocks. Catalytic pyrolysis can help address this issue by promoting the cracking of heavy hydrocarbons into lighter compounds, potentially improving oil fluidity and reducing downstream wax accumulation. However, achieving the desired oil quality requires more than catalyst addition. Catalyst selection, reaction temperature, vapor residence time, and condensation system design must work together to balance wax reduction, liquid yield, and operating costs. For plastic recycling projects, a well-designed catalytic pyrolysis system can provide greater control over hydrocarbon product distribution. The most suitable solution should be determined through feedstock analysis, pilot testing, and evaluation of the final oil's intended use.
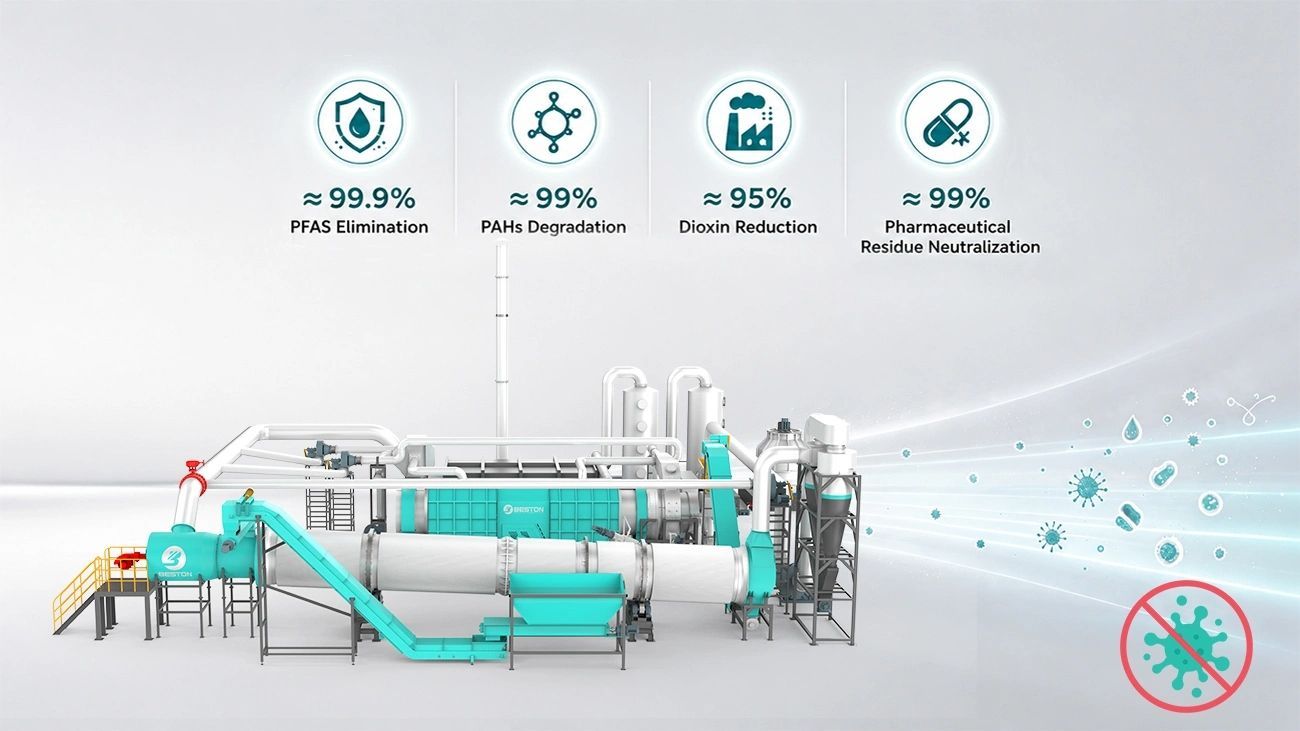
Municipal sewage sludge carbonization is a potential solution for reducing sludge volume, recovering carbon-rich materials, and improving waste management efficiency. However, its feasibility depends on several critical factors, including heavy metal behavior, feedstock moisture content, energy consumption, and the final destination of the carbonized product. Before investing in a carbonization project, operators need to evaluate both technical performance and environmental compliance. 1. How Does Municipal Sewage Sludge Carbonization Work? Municipal sewage sludge is generated during wastewater treatment and typically contains organic matter, inorganic minerals, water, and potentially hazardous contaminants. Carbonization uses controlled heating under oxygen-limited conditions to convert part of the organic matter into a carbon-rich solid product. Compared with conventional disposal methods, carbonization can reduce the volume of sludge requiring further management and may recover useful energy from volatile compounds. Depending on the feedstock and operating conditions, the process can also produce combustible gases and condensable vapors that require appropriate collection and treatment. A complete sewage sludge treatment plant may include sludge dewatering, drying, carbonization, gas treatment, and product handling systems. Integrating these processes helps improve operational stability and provides a clearer basis for evaluating overall project economics. 2. Heavy Metal Treatment: A Critical Feasibility Factor Heavy metals are one of the main concerns when converting municipal sewage sludge into carbonized products. Sludge may contain lead, cadmium, chromium, mercury, nickel, copper, and zinc, depending on the wastewater sources and treatment processes. Carbonization does not automatically eliminate heavy metals. Many metals remain in the solid residue, and their concentrations may increase as organic matter and water are removed. Changes in temperature and chemical composition can also affect metal speciation, mobility, and leachability. Certain volatile elements, particularly mercury and some metal compounds, may transfer into the gas phase and require effective emission controls. Therefore, feasibility studies should include several important measures. - Feedstock testing: Analyze representative sludge samples for total heavy metal concentrations and other relevant contaminants. - Process evaluation: Assess how carbonization temperature, residence time, and feedstock composition influence contaminant distribution. - Emission control: Design suitable gas collection, particulate removal, and exhaust treatment systems based on the expected pollutants. - Product testing: Evaluate heavy metal concentrations, leaching characteristics, and compliance with the intended end-use standards. If the carbonized product is intended for agricultural use, soil improvement, or other beneficial applications, compliance must be demonstrated under the applicable local regulations. If contaminant levels exceed permitted limits, controlled disposal or further treatment may be necessary. 3. What Moisture Content Is Required Before Carbonization? Moisture content directly affects the energy demand and operating cost of sludge carbonization. Fresh municipal sewage sludge often contains substantial amounts of water, making direct thermal treatment energy-intensive. A large proportion of the available heat may otherwise be consumed by water evaporation rather than by the carbonization process. Mechanical dewatering is generally the first step in reducing moisture content. Equipment such as filter presses or centrifuges can remove part of the water before thermal drying. A drying system can then reduce the moisture level to a range suitable for the selected carbonization equipment. There is no universal moisture requirement for every project. The appropriate inlet moisture content depends on reactor design, feedstock characteristics, heat source, and the availability of waste heat. Many thermal carbonization systems benefit from drying sludge to approximately 10%–20% moisture before feeding, but this range should be confirmed with equipment specifications and process testing. Feasibility calculations should compare the energy required for drying with the recoverable energy from process gases and other available heat sources. Waste heat recovery, efficient insulation, and automated temperature control may reduce operating costs. However, the energy balance must be calculated using actual sludge properties rather than theoretical assumptions alone. 4. Where Can the Final Carbonized Product Go? The commercial value of municipal sludge carbonization depends heavily on whether the final product has a safe and legally acceptable destination. Potential pathways include the following. - Construction materials: Subject to technical testing and regulatory approval, treated sludge-derived solids may be evaluated as components in selected building materials. - Land application: Agricultural or soil-related use requires strict assessment of heavy metals, organic contaminants, stability, and applicable product standards. Carbonization alone does not establish suitability. - Industrial applications: Certain products may be considered for mineral-based or carbon-containing industrial uses if their properties meet the required specifications. - Controlled disposal: Material that fails safety or quality requirements may need to be managed at an authorized disposal facility. Before selecting a destination, project developers should consult potential end users and regulatory authorities. Product testing should cover not only contaminant levels but also relevant physical and chemical properties, such as calorific value, ash content, and stability. 5. How to Evaluate Project Feasibility A reliable feasibility study should combine technical, environmental, and financial assessments. Key inputs include daily sludge throughput, initial and target moisture content, organic matter content, heavy metal concentrations, energy prices, and local disposal fees. Capital expenditure should account for dewatering and drying equipment, the carbonization reactor, exhaust treatment, material handling, and safety systems. Operating costs should include electricity, supplementary fuel, maintenance, laboratory testing, and residue management. Revenue from recovered energy or carbonized products should only be included when supported by realistic market demand and regulatory approval. Pilot testing is particularly valuable when sludge composition varies significantly or when the intended product has strict quality requirements. It helps verify drying performance, energy consumption, contaminant behavior, product quality, and the suitability of the proposed treatment process. Conclusion Municipal sewage sludge carbonization can offer a practical route for sludge volume reduction and resource recovery, but it is not automatically a safe or profitable solution. Heavy metal behavior, moisture control, energy efficiency, and final product utilization must be assessed together. By conducting feedstock analysis, process testing, environmental evaluations, and market research before investment, project developers can make better-informed decisions and establish a treatment system that meets local requirements.
Ash management is an important operational consideration in charcoal production because the mineral fraction of biomass directly influences the quality, purity, and end-use suitability of the final product. In charcoal making equipment, ash originates primarily from inorganic constituents naturally present in the feedstock, including calcium, potassium, magnesium, silica, iron, and other mineral compounds. These substances remain largely in the solid residue during carbonization, although their chemical forms and distribution may change with temperature. Effective ash control therefore begins with feedstock characterization and continues through carbonization, discharge, and post-production quality assessment. Mineral Content and Ash Formation During Carbonization The ash content of charcoal depends on both feedstock composition and processing conditions. Wood from clean, debarked sources generally contains relatively low concentrations of inorganic minerals, whereas agricultural residues, bark, straw, and certain industrial biomass streams may contain substantially higher mineral fractions. During carbonization, volatile organic compounds are released while much of the nonvolatile mineral matter remains in the char. Consequently, the relative ash concentration can increase as organic mass is removed, even when the absolute quantity of minerals changes very little. Mineral composition also affects the thermal behavior of the feedstock. Potassium and calcium compounds can catalyze certain reactions during biomass decomposition, while silica-rich materials may contribute to refractory deposits or abrasive residues. These effects vary with mineral speciation, temperature, and interactions among inorganic constituents. For charcoal producers, measuring total ash alone is insufficient. Mineral composition provides additional information about process behavior and product suitability. Effects of Ash Content on Final Charcoal Quality High ash content reduces the proportion of combustible carbon in charcoal on a mass basis. This can lower its effective heating value and increase the quantity of inert material delivered to downstream users. The consequences extend beyond energy performance. In metallurgical applications, excessive mineral impurities may affect reactivity, slag formation, and process consistency. For barbecue charcoal, elevated ash levels can increase residual material after combustion and influence handling characteristics. In activated-carbon production, mineral impurities may obstruct pores or interfere with subsequent activation, depending on their composition and distribution. Ash is not always undesirable. In agricultural biochar, selected minerals can contribute nutrients and influence soil chemical properties. Calcium, magnesium, and potassium may provide agronomic value, although their availability depends on their chemical forms. Conversely, feedstocks contaminated with heavy metals can produce ash-rich char that requires additional safety assessment. The appropriate ash specification therefore depends on the intended application rather than a universal maximum threshold. Feedstock Selection and Mineral Contamination Control Feedstock preparation is the first practical measure for managing ash. Raw materials should be assessed for moisture, mineral content, soil contamination, and the presence of extraneous inorganic matter. Soil and sand adhering to biomass can increase ash content without contributing useful nutrients. Mechanical screening, effective storage practices, and suitable cleaning procedures can reduce this contamination before material enters charcoal making equipment . Feedstock blending may also help stabilize mineral content when several biomass sources are available. However, blending should follow laboratory analysis because combining materials with different mineral profiles does not necessarily produce predictable ash characteristics. Periodic testing of representative feedstock samples allows operators to identify seasonal variations and adjust process settings accordingly. Carbonization Temperature and Ash Management Carbonization temperature affects residual carbon content, mineral transformations, and the physical structure of the resulting charcoal. Higher temperatures generally promote greater devolatilization, potentially increasing ash concentration on a mass basis. Certain minerals may also undergo phase transformations, sintering, or changes in solubility. Excessive temperatures do not automatically improve charcoal quality. The optimal operating range depends on feedstock characteristics, reactor design, residence time, and product requirements. A controlled heating profile helps maintain consistent carbonization and reduces variability between production batches. Operators should monitor temperature distribution, feeding conditions, and discharge performance rather than relying on a single nominal temperature. Ash separation after carbonization may remove loose mineral contaminants, but it cannot reliably eliminate minerals embedded within the char matrix. Prevention at the feedstock stage is therefore more effective than depending entirely on downstream separation. Quality Testing and Operational Monitoring A structured quality-control program should combine laboratory analysis with routine equipment inspection. Relevant measurements include total ash content, fixed carbon, volatile matter, moisture, and calorific value. Where contamination is a concern, elemental analysis can identify specific minerals and potentially hazardous metals. Testing should use representative samples and consistent analytical methods. Comparing results across production runs helps distinguish feedstock-related changes from operational variability. For industrial producers, the most effective ash-management strategy integrates feedstock screening, mineral characterization, controlled carbonization, and application-specific product testing. This approach enables charcoal making equipment to deliver more consistent output while reducing contamination risks, improving resource utilization, and aligning final charcoal quality with the technical requirements of its intended market.
