How to Maintain a Pyrolysis Reactor for Optimal Performance
Cathy Wang • November 1, 2024

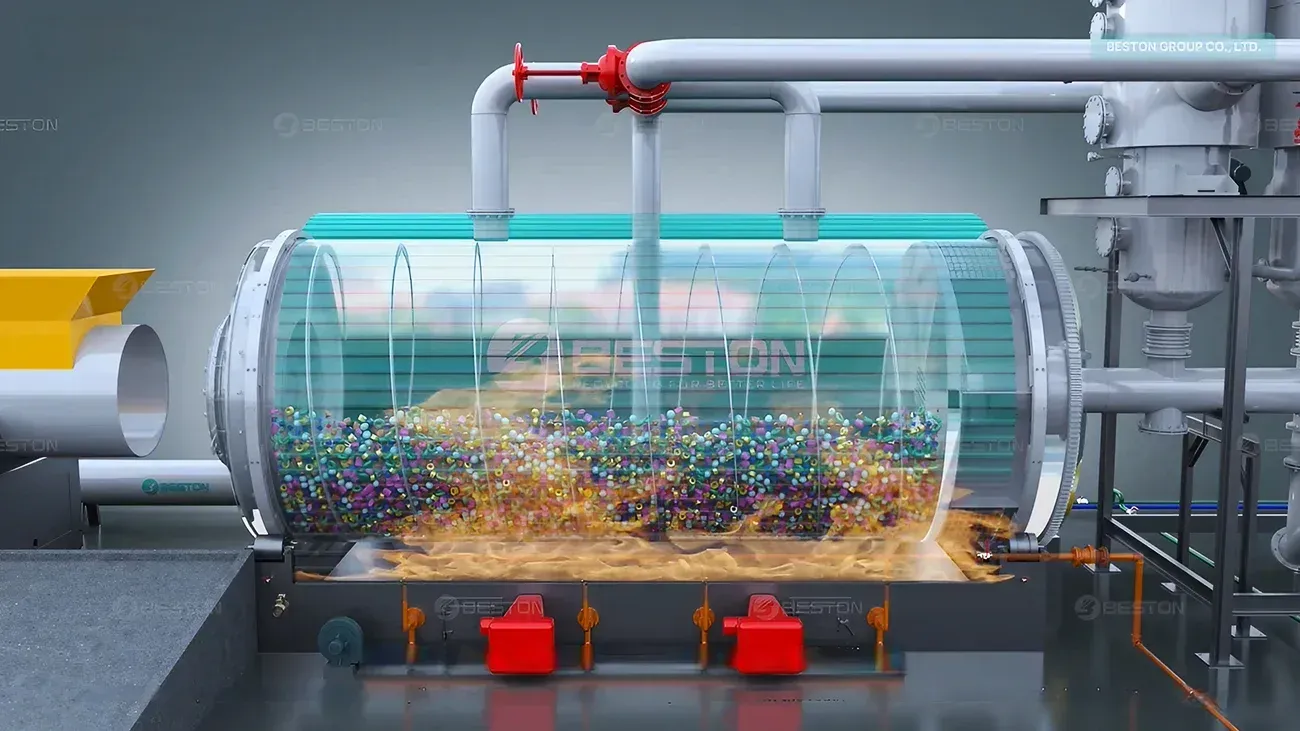
Pyrolysis reactors are integral to the thermal decomposition of organic materials, providing an environmentally-friendly approach to recycling waste into useful byproducts such as biochar, fuel oil, and syngas. However, maintaining a pyrolysis reactor requires meticulous attention to detail and a proactive approach to ensure safe and efficient operation. This guide delves into the essential practices for maintaining a pyrolysis reactor, enhancing its lifespan and ensuring consistent performance.

1. Regular Inspection of Reactor Components

Consistent inspection is fundamental to the maintenance of a pyrolysis reactor. Over time, high temperatures and reactive materials can cause wear and degradation. Key areas to inspect include:

  • Reactor Vessel: Examine for signs of cracking, corrosion, or material degradation. Pay particular attention to areas near heating elements and points of contact with high-heat materials.
  • Seals and Gaskets: Regularly assess seals and gaskets for wear or leaks. These components ensure the airtight environment crucial for pyrolysis and prevent hazardous gas emissions.
  • Piping and Valves: Check for any obstructions, leaks, or irregularities in valves and pipelines. Blockages can compromise pressure levels and impede the flow of byproducts.
  • Heating Elements: Evaluate the condition of the heating system, ensuring that elements distribute heat evenly and achieve target temperatures efficiently.

Routine inspections should be conducted with appropriate safety equipment, as some areas may retain residual heat or reactive substances. Scheduled visual inspections help identify early signs of wear and preempt issues that could escalate into operational failures.

2. Monitoring Temperature and Pressure Controls

Temperature and pressure are critical to achieving the precise conditions required for pyrolysis. Maintaining these parameters within optimal ranges prevents unexpected reactions and maximizes reactor efficiency.

  • Temperature Sensors: Check the calibration of sensors regularly. Accurate readings are essential for the process, and any deviation in calibration could lead to energy inefficiency or potential safety hazards.
  • Pressure Gauges: Monitor pressure gauges to ensure stable internal conditions. Pressure fluctuations can indicate blockages or seal degradation, necessitating immediate attention.
  • Automated Control Systems: Many reactors use PLC (Programmable Logic Controller) systems to manage these variables. Ensure that these systems receive regular software updates and functional checks to maintain their reliability.

Consistent calibration and monitoring not only extend the lifespan of reactor components but also safeguard against abrupt temperature spikes or pressure drops, which can damage the reactor.

3. Cleaning and Decontamination

Reactors for waste pyrolysis plant accumulate residues over time, which can interfere with the process and degrade product quality. Implement a rigorous cleaning schedule to keep the reactor’s internal environment free from obstructions and contaminants.

  • Char and Ash Removal: Char and ash deposits can hinder heat distribution and reduce the reactor's efficiency. Cleaning out these residues after each batch helps maintain optimal thermal conductivity.
  • Reactor Wall Scraping: High-temperature reactors often experience carbon buildup on the walls. Manual or automated scraping can prevent these deposits from becoming problematic. Choose cleaning methods that won’t scratch or degrade the reactor walls.
  • Condensers and Gas Lines: Regularly clear condensers and gas lines to prevent clogging from oil residues or tar, which can compromise gas flow and pressure regulation.

Using a non-abrasive, high-temperature cleaning agent for decontamination is recommended. This prevents the introduction of foreign substances while ensuring the reactor remains functional and efficient.

4. Lubrication and Mechanical Maintenance

Pyrolysis reactors have multiple moving parts, including feed mechanisms, discharge systems, and valves, which require regular lubrication to function seamlessly. Proper lubrication reduces friction, minimizes wear, and prevents overheating in critical components.

  • Feed Mechanism: A smooth feed mechanism ensures a steady flow of material, which is essential for uniform pyrolysis. Lubricate gears and moving parts to avoid jamming and irregular feeding.
  • Discharge System: The discharge system, particularly in continuous reactors, handles high temperatures and frequent material outflow. Regular lubrication of these parts prevents overheating and extends service life.
  • Valves and Actuators: Valves and actuators, which regulate the flow of gases and feedstock, require periodic lubrication and inspection for wear. Replace any components showing signs of damage to avoid operational delays.

Use high-temperature lubricants specifically designed for industrial applications. Low-quality or incompatible lubricants can deteriorate quickly under high temperatures, leaving residue that hampers movement.

5. Ensuring Proper Safety Systems and Emergency Protocols

Safety is paramount when operating a pyrolysis reactor, as the high temperatures and flammable byproducts can create hazardous conditions. Equip the reactor with comprehensive safety features and review emergency protocols regularly.

  • Gas Detection Systems: Install gas sensors to monitor potential leaks. Carbon monoxide and other volatile gases can be hazardous, so early detection systems are essential for operator safety.
  • Emergency Shutoff Valves: Ensure emergency shutoff valves are in place and functional. These systems automatically halt operations in case of irregular pressure or temperature changes.
  • Explosion-Proof Components: Many reactors incorporate explosion-proof designs. Verify that these components are intact, as pressure irregularities or system malfunctions can otherwise lead to dangerous outcomes.

Training staff on emergency procedures and performing regular safety drills ensures a rapid response to potential hazards. Prioritize safety checks and ensure all workers are familiar with reactor emergency protocols.

6. Maintaining a Log of Maintenance Activities

A detailed maintenance log is essential for tracking the health and performance of a pyrolysis reactor. Documenting each maintenance task, along with inspection results and component replacements, offers valuable insight into recurring issues and component lifespan.

  • Routine Inspections and Results: Record the results of every inspection, noting any observations, irregularities, or repairs conducted.
  • Repairs and Replacements: Log each part replacement, including installation dates, supplier details, and warranty information.
  • Operational Metrics: Keep track of temperature, pressure, and output performance metrics over time. This data helps identify any declines in efficiency or emerging patterns that may signal wear.

Regular review of the maintenance log allows operators to identify potential improvements, optimize reactor performance, and forecast the need for replacements before issues become critical.

Conclusion

A well-maintained pyrolysis reactor not only ensures operational efficiency but also enhances safety and prolongs the lifespan of the machinery. Through regular inspections, precise control of temperature and pressure, thorough cleaning, and consistent mechanical upkeep, operators can mitigate common issues and keep the reactor running at optimal levels. By committing to these best practices, facilities can maximize both output and quality, making the pyrolysis process safer, more reliable, and economically sustainable over the long term.
By Cathy Wang • September 29, 2026
The performance of a plastic pyrolysis system is often evaluated by production capacity and energy efficiency. However, product quality remains equally important. In a commercial operation, the composition and consistency of pyrolysis oil, combustible gas, and solid residues determine the potential value of the final products and influence downstream applications. For investors exploring a plastic to oil machine for sale , understanding the factors that affect product quality is essential for making informed technical and economic decisions. Feedstock Composition Determines Product Characteristics Plastic feedstock is the primary variable influencing pyrolysis output. Different polymers exhibit distinct thermal decomposition pathways, resulting in variations in oil composition, gas yield, and solid residue formation. Polyolefin materials such as polyethylene (PE) and polypropylene (PP) generally produce higher liquid yields because their molecular structures favor hydrocarbon generation during pyrolysis. Polystyrene (PS) can generate aromatic compounds, while plastics containing chlorine, oxygen, or other heteroatoms may require additional process control due to the formation of undesirable by-products. Feedstock purity is equally important. Metal fragments, dirt, moisture, and non-target materials can alter thermal behavior and affect the consistency of products. A stable and well-prepared feedstock stream contributes to more predictable operation and product quality. Temperature Control Influences Product Distribution Pyrolysis is fundamentally a temperature-driven process. Reactor temperature affects the extent of polymer cracking and determines the relative proportion of liquid, gas, and solid products. Lower temperatures may lead to incomplete decomposition and higher residue content. Excessively high temperatures, by contrast, can promote secondary cracking reactions, converting condensable hydrocarbons into permanent gases. Maintaining a suitable temperature window allows the system to balance liquid production with gas generation. Temperature uniformity is equally significant. Thermal gradients within the reactor can create heterogeneous reaction zones, leading to fluctuations in product composition. Continuous monitoring and automated control systems help maintain stable operating conditions. Residence Time and Vapor Management The duration that plastic and pyrolysis vapors remain inside the reactor also affects final products. Longer residence times can increase secondary reactions, altering hydrocarbon distribution and reducing the proportion of heavier liquid fractions. Vapor handling systems therefore play an important role. Efficient condensation equipment enables the recovery of condensable hydrocarbons while separating non-condensable gas for energy utilization. The design of condensers, cooling systems, and gas pipelines influences heat transfer efficiency and can affect the composition of collected oil. Insufficient cooling may result in the loss of valuable hydrocarbons, while excessive cooling can increase operational complexity. Role of Non-Condensable Gas Non-condensable gas generated during pyrolysis contains combustible components that can contribute to process heating after suitable treatment. This internal energy circulation reduces dependence on external fuel sources and improves thermal efficiency. Gas composition depends on feedstock type, reactor temperature, and operating conditions. Hydrogen, methane, and light hydrocarbons may be present in varying proportions. Their effective utilization can improve overall energy management within the plant. For buyers comparing a plastic to oil machine for sale , the ability to recover and utilize process gas should be considered alongside reactor design and production capacity. Formation and Management of Solid Residues Solid residues represent the non-volatile fraction remaining after thermal decomposition. Their quantity and characteristics are affected by feedstock composition, operating temperature, and process stability. In plastic pyrolysis, residue may contain carbonaceous material, inorganic additives, pigments, fillers, and traces of contaminants. Excessive residue generation can indicate incomplete conversion or unsuitable feedstock preparation. Residue handling systems therefore form an important part of plant design. Efficient discharge and collection support continuous operation while reducing maintenance requirements. Integrating Quality Control into Plant Operation Product quality does not depend on a single parameter. It results from the interaction of feedstock preparation, temperature management, residence time, vapor recovery, and residue control. For companies evaluating a plastic to oil machine for sale , technical assessment should extend beyond nominal production capacity. Feedstock compatibility, thermal stability, condensation efficiency, gas utilization, and residue management all influence the consistency and value of final products. A well-designed pyrolysis system combines these elements into an integrated process. Stable operation, controlled reaction conditions, and effective product recovery can improve the quality of oil, gas, and solid residues while supporting more efficient resource utilization from plastic waste.
By Cathy Wang • September 29, 2026
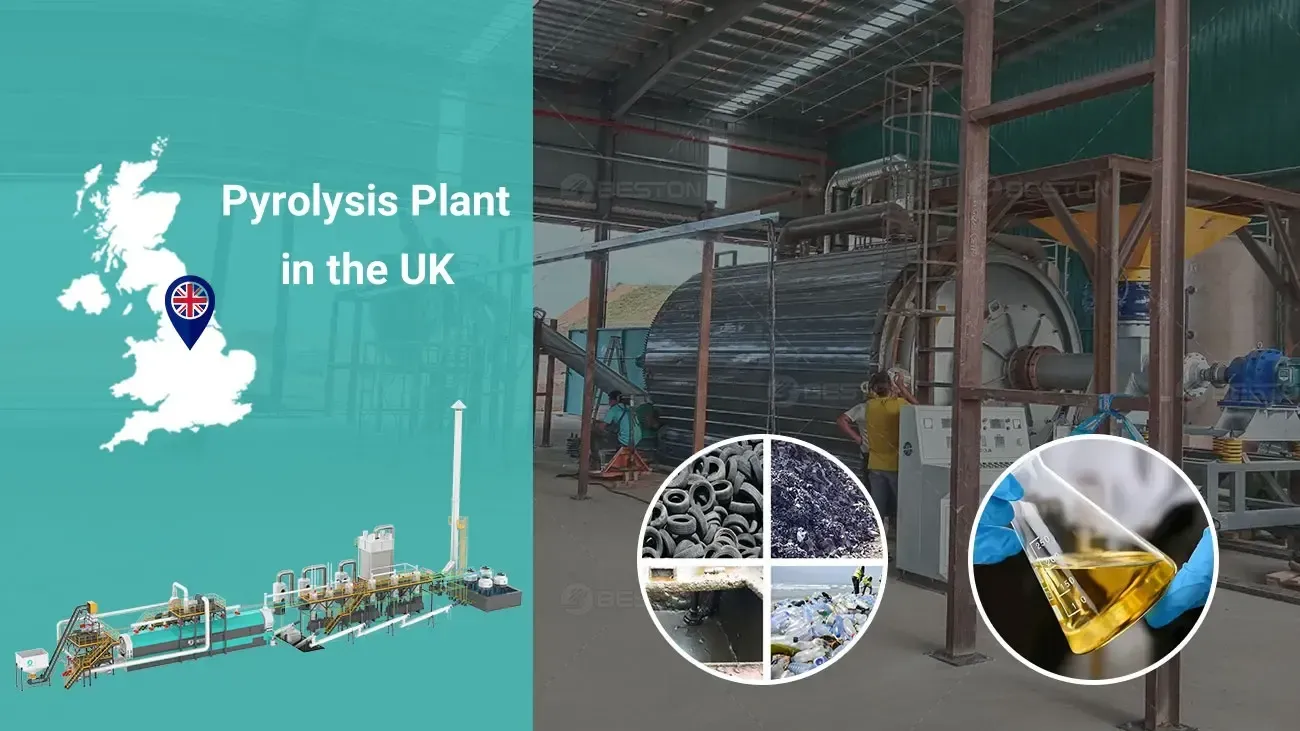
Every year, Britain's roads consume tens of millions of tyres. When they wear out, they become one of the country's most persistent waste streams: bulky, durable, and difficult to recycle. Industry estimates put UK end-of-life tyre (ELT) arisings at roughly 500,000 tonnes a year. With landfill closed to them, how that material is handled has become a defining question for the recycling sector. The Tyre Landfill Ban: What Changed The UK has not banned landfill in general. Many wastes can still be landfilled, subject to permits and Landfill Tax. Tyres, however, are a specifically restricted category. Whole tyres were banned from landfill in 2003, and shredded tyres followed in 2006. The reasoning was sound. Tyres trap gases, tend to work their way up through landfill layers, and consume valuable void space. Stockpiles are just as problematic: tyre fires are notoriously hard to extinguish and release harmful emissions. With landfill off the table, ELTs have followed three main routes: material recovery (crumb and granulate for surfacing and infrastructure), energy recovery (chiefly cement kilns and tyre-derived fuel), and export. Each has limits. Crumb markets are finite, energy recovery does little to keep materials in circulation, and exporting shifts environmental responsibility overseas at a time when regulators and customers are asking tougher questions about where waste ends up. Enter Pyrolysis Pyrolysis heats shredded tyres in an oxygen-free reactor, breaking them down thermally rather than burning them. The process yields three principal outputs: pyrolysis oil, recovered carbon black (rCB), and steel wire. It also produces a non-condensable syngas, which is typically recycled to heat the reactor. This is why interest in the pyrolysis plant UK operators can deploy is rising. Pyrolysis converts a low-value, hard-to-handle waste into several marketable products, and it can process feedstock that is unsuitable for mechanical recycling. Because the syngas can supply much of the process heat, well-designed plants can be reasonably energy self-sufficient once running. Where the Value Lies Carbon black. Recovered carbon black is arguably the most strategically important product. Tyre and rubber manufacturers face growing pressure to increase recycled content, and rCB offers a lower-carbon alternative to virgin carbon black made from fossil feedstocks. The challenge is consistency: buyers need tightly specified material, so post-processing and quality control are critical. Pyrolysis oil. The oil can be used as an industrial fuel or upgraded as a petrochemical feedstock. Access to premium markets depends on refining and on regulatory clarity about when the material stops being classed as waste. Steel. Recovered steel is easy to sell into established scrap markets and adds useful secondary revenue. Challenges Developers Must Address The opportunity is real, but so are the hurdles: Permitting. Thermal treatment facilities need environmental permits, and regulators scrutinise emissions controls, abatement systems, and monitoring closely. Early engagement with the environmental regulator and local planning authority is essential. Feedstock security. Reliable, contracted tyre supply at predictable cost underpins any business case. Relationships with collectors and processors matter as much as reactor design. Product specification. Offtake agreements for oil and carbon black should be pursued early, with clear quality standards. Community acceptance. Thermal technologies attract public scrutiny. Transparent communication about emissions, traffic, and safety builds trust. Technology choice. Batch, semi-continuous, and continuous systems differ significantly in throughput, maintenance demands, and capital cost. Independent due diligence on reference plants is well worth the investment. Policy Tailwinds Broader trends favour recycling routes that return materials to the economy. Resource-efficiency goals, continuing discussion of producer responsibility approaches for tyres, and industry commitments to recycled content all point toward growing demand for verified, traceable secondary materials. Tyre manufacturers and fleet operators increasingly want demonstrable end-of-life solutions, and pyrolysis can offer a credible story when supported by robust carbon accounting and certification. Looking Ahead The tyre landfill ban solved one problem and created another: what to do with half a million tonnes of durable, high-energy material each year. Pyrolysis offers a technically proven answer, but success depends on execution. That means disciplined feedstock sourcing, realistic financial modelling, high-quality outputs, and open engagement with regulators and communities. For investors, waste operators, and technology providers, the message is encouraging. As the UK tightens its approach to waste and raises its circular-economy ambitions, a well-run pyrolysis plant UK projects can build is well placed to turn a regulatory constraint into a durable commercial opportunity.
By Cathy Wang • September 23, 2026
Municipal and industrial wastewater treatment facilities generate large volumes of sludge as a by-product of purification processes. This material often contains organic matter, moisture, inorganic minerals, and trace contaminants, making disposal both technically challenging and economically significant. Traditional management methods, such as landfilling, incineration, and direct land application, are increasingly influenced by environmental regulations, transportation costs, and resource-recovery objectives. Against this background, sewage sludge pyrolysis has emerged as a thermochemical pathway that converts sludge into carbon-rich products while reducing waste volume. Characteristics of Sewage Sludge as a Feedstock Sewage sludge differs substantially from conventional biomass feedstocks. Moisture content is often high, and ash concentrations can vary depending on wastewater composition and treatment processes. In addition, sludge may contain nutrients, metals, inorganic compounds, and residual organic substances. These characteristics influence thermal behavior during pyrolysis. Feedstock preparation therefore becomes an important step. Mechanical dewatering, thermal drying, and particle-size homogenization can improve process stability and reduce unnecessary energy consumption. The selection of pretreatment methods depends on sludge properties, local infrastructure, and the intended application of the final carbon product. Thermal Conversion Through Sewage Sludge Pyrolysis Pyrolysis involves heating organic material under oxygen-limited conditions, allowing thermal decomposition to occur without complete combustion. During sewage sludge pyrolysis , complex organic compounds are transformed into three principal fractions: Carbon-rich solid products; Condensable liquids; Non-condensable gases. The distribution of these products depends on reactor temperature, heating rate, residence time, and feedstock composition. Compared with direct incineration, pyrolysis emphasizes resource recovery alongside waste reduction. Organic carbon is retained partially within the solid product, while combustible gases can contribute to process heating after appropriate treatment. The process also reduces sludge volume significantly, thereby lowering transportation and disposal requirements. Reactor and Equipment Considerations Sludge processing requires equipment designed to accommodate feedstocks with varying moisture levels, particle characteristics, and ash content. A sludge pyrolysis system generally includes: Feedstock pretreatment equipment; Drying units; Thermal conversion reactor; Condensation system; Gas-utilization section; Solid-product cooling system; Emission-control equipment. The reactor is the core component. Rotary kilns, screw reactors, and other indirectly heated systems are frequently used because they provide controlled material movement and stable heat transfer. Temperature management is essential. Excessive temperatures can reduce solid-product yield, while insufficient thermal input may result in incomplete conversion. Process automation and instrumentation help maintain stable operating conditions. Carbon Products and Resource Recovery One of the key outcomes of sewage sludge pyrolysis is the generation of carbon-containing solids. Depending on feedstock composition and processing conditions, these materials may contain fixed carbon, mineral matter, and nutrient elements. Potential applications vary according to product quality, local regulations, and technical requirements. In some contexts, carbon products may be considered for industrial applications, construction materials, or further upgrading processes. Comprehensive characterization is necessary before determining suitable end uses. The gaseous fraction also has value. After purification and controlled combustion, non-condensable gas can provide part of the thermal energy required for the pyrolysis process. This internal energy loop may improve overall thermal efficiency. Emission Control and Environmental Considerations Sludge treatment technologies must address emissions carefully. Pyrolysis systems therefore require integrated gas cleaning and environmental control measures. Dust removal, condensation, thermal oxidation, and exhaust-gas treatment may be incorporated depending on process design and regulatory requirements. Continuous monitoring of temperature, pressure, and emissions can further improve operational reliability. Attention should also be given to the management of inorganic residues and potential contaminants. Product testing remains essential to ensure that recovered materials meet applicable standards. From Waste Management to Carbon Resource Utilization The concept behind sewage sludge pyrolysis extends beyond disposal. Instead of treating sludge solely as a waste stream, pyrolysis views it as a source of carbon, energy, and potentially useful materials. A complete process chain—comprising dewatering, drying, thermal conversion, gas utilization, product cooling, and emission control—can transform complex sludge streams into more stable products while reducing waste volume. As wastewater treatment facilities seek more circular resource-management strategies, sludge pyrolysis machines provide a technological pathway that links waste reduction, energy recovery, and carbon-product generation within a single thermochemical system.