Strategic Approaches to Investing in Biochar Production Equipment

Cathy Wang • April 24, 2025

Biochar production, derived from the thermal decomposition of organic materials, offers significant environmental and economic benefits. As a sustainable solution for carbon sequestration, soil enhancement, and waste management, biochar production has gained attention from governments, corporations, and investors alike. The demand for biochar has increased due to its potential applications in agriculture, water filtration, and energy production, among other industries. As such, investment in biochar production equipment has become an appealing prospect for those looking to tap into the growing green energy sector.

Assessing Market Demand and Product Applications

The first strategic consideration when investing in biochar production equipment is understanding the market demand for biochar and its various applications. Biochar has established itself as a valuable product in agriculture, where it is used as a soil amendment to improve fertility and water retention. Additionally, biochar is used in water treatment, carbon capture, and even as a renewable energy source. With increasing interest in sustainable agriculture practices and carbon offset solutions, the demand for biochar is expected to grow significantly.

Investors should examine the regional markets where biochar is in high demand. In agricultural regions, for instance, biochar’s role as a soil enhancer makes it a key product for farmers seeking to improve soil health without resorting to harmful chemicals. Similarly, municipalities focused on water purification may drive demand for biochar used in filtration systems. By identifying the most promising sectors and regions, investors can better allocate resources to equipment that aligns with market trends.

Selecting the Right Biochar Production Equipment

Investing in the right biochar production equipment is crucial for maximizing profitability. The technology behind biochar production relies on pyrolysis, a process that requires specific equipment to achieve the desired results. The two primary types of equipment used for biochar production are fixed-bed and rotary kiln systems, each with its advantages and trade-offs.

1. Fixed-Bed Systems

Fixed-bed pyrolysis units are typically smaller and more cost-effective, making them suitable for small to medium-scale production. These systems are highly efficient and provide high-quality biochar with low operating costs. They are often preferred for research, pilot projects, or regional applications. However, the scale of production may be limited compared to larger systems, which could affect the ability to meet high demand or capitalize on economies of scale.

2. Rotary Kiln Systems

For large-scale biochar production, rotary kiln systems are often the preferred choice. These systems are capable of processing larger quantities of feedstock and produce higher volumes of biochar. Rotary kilns are also versatile, capable of processing a wide range of organic materials, including agricultural waste, forestry residues, and municipal solid waste. However, they come with higher initial investment costs and require more complex maintenance compared to fixed-bed systems. When considering rotary kilns, investors must assess whether the projected demand justifies the larger scale of operations.

3. Upgraded and Hybrid Systems

Some modern biochar production systems combine the benefits of fixed-bed and rotary kilns, providing flexibility and scalability. These hybrid systems offer enhanced automation, improved feedstock processing, and better energy efficiency. Such systems may be ideal for investors looking to future-proof their operations, as they can scale production and integrate advanced features without significant capital expenditure.

The decision on which equipment to purchase should consider the scale of operation, the availability of feedstock, the expected output, and the target market. While larger systems may seem appealing for high-volume production, smaller systems can offer quicker returns on investment and lower operational risk.

Evaluating Financial and Environmental Impact

Investors must evaluate the financial feasibility of biochar production, balancing the initial investment in equipment with the expected return on investment (ROI). The capital expenditure involved in acquiring high-quality biochar production equipment can be substantial. However, there are several factors that can make this investment worthwhile:

  • Revenue Streams: Biochar production can create multiple revenue streams. In addition to selling biochar, investors can monetize other by-products such as bio-oil, syngas, and wood vinegar. These by-products, when processed and marketed correctly, can significantly improve the ROI of a biochar production plant.
  • Carbon Credits: As biochar is a carbon-negative product, producers may qualify for carbon credits or other incentives. This can provide a secondary source of revenue, improving the financial outlook for the investment.
  • Government Incentives: Many governments offer financial incentives for green technology projects, including biochar production. These can take the form of grants, tax credits, or low-interest loans, which can reduce the initial capital burden and improve profitability.

On the environmental side, biochar production offers substantial sustainability benefits. It acts as a carbon sink, trapping carbon in a stable form that can remain in the soil for hundreds to thousands of years. By converting waste biomass into biochar, investors can contribute to reducing landfill waste, lowering greenhouse gas emissions, and improving soil health.

Scaling Operations and Diversifying Production

Once the initial equipment is in place and production has ramped up, scaling operations becomes a critical consideration. The scalability of biochar production equipment is an important factor in long-term profitability. Investors should look for technologies that can easily expand in capacity to accommodate increased demand, as well as adapt to changing market conditions.

Diversifying the feedstock used in biochar production can also help reduce risk and improve operational efficiency. While wood chips and agricultural residues are common feedstocks, biochar production can also utilize municipal solid waste, forestry by-products, and industrial waste, such as plastic waste. By incorporating diverse feedstocks, operators can reduce supply chain risks associated with feedstock shortages and volatility in raw material prices.

Furthermore, as demand for biochar continues to grow, the opportunity to integrate biochar production with other sustainable technologies, such as biogas production or biomass-to-energy systems, becomes increasingly attractive. This diversification can improve the financial resilience of biochar production plants and increase their long-term sustainability.

Monitoring Industry Trends and Technological Advancements

Investors should remain attuned to the latest industry trends and technological advancements in biochar production. Innovations in pyrolysis technology, such as higher-efficiency systems, lower emissions, and the ability to process a wider range of feedstocks, are continually reshaping the market. By keeping an eye on these developments, investors can ensure that their biochar production equipment remains competitive and aligned with the evolving needs of the market.

Additionally, understanding global regulatory standards for carbon emissions, waste management, and renewable energy can provide valuable insights into future market conditions and investment risks. As more industries and governments commit to carbon neutrality, the demand for biochar is expected to increase, creating favorable conditions for those who strategically position themselves in this growing sector.
By Cathy Wang • October 29, 2026
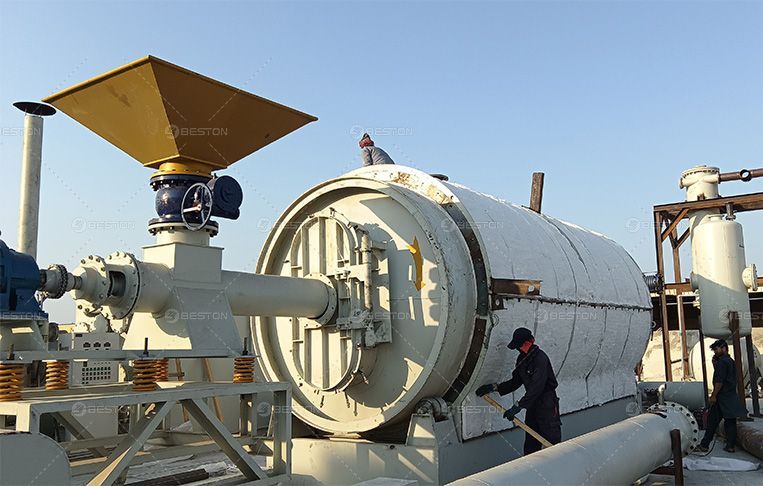
Installing a pyrolysis plant involves more than positioning the reactor and connecting auxiliary equipment. Successful commissioning requires coordinated mechanical assembly, utility integration, instrumentation verification, safety inspections, and performance testing. Each stage establishes the conditions for reliable operation and helps identify installation defects before commercial production begins. For a Beston pyrolysis plant , the installation plan should reflect the equipment configuration, feedstock characteristics, site infrastructure, and applicable local regulations. Equipment Assembly and Site Preparation Installation begins with a site-readiness assessment. The foundation must meet the equipment supplier's requirements for load-bearing capacity, levelness, anchoring, and vibration control. Access roads, unloading areas, lifting equipment, and maintenance clearances should also be confirmed before delivery. Once the equipment arrives, components are inspected against the packing list and technical documentation. Transport damage, missing parts, and deviations from approved drawings should be recorded and resolved before assembly proceeds. Mechanical installation typically covers the following systems: Main reactor: Positioning, alignment, anchoring, and verification of the drive or rotation mechanism where applicable. Feeding and discharge equipment: Installation of conveyors, feeders, sealing devices, and residue-handling components. Condensation system: Assembly of condensers, separators, pipelines, and associated cooling equipment. Gas handling: Connection of non-condensable gas lines, combustion equipment, and required treatment systems. Storage facilities: Installation of appropriate tanks, transfer lines, valves, and containment provisions for liquid products. Flange connections, seals, supports, and expansion allowances require particular attention. Thermal expansion can impose substantial mechanical stress during operation, especially where hot pipelines connect to relatively cool equipment. Assembly should follow approved engineering drawings rather than relying on visual alignment alone. Electrical Integration and Instrumentation Electrical and control-system installation establishes the link between mechanical equipment and process supervision. Motors, control cabinets, sensors, actuators, and protective devices must be connected and verified according to the electrical drawings and equipment specifications. Temperature sensors should be checked for correct placement, signal transmission, and calibration status. Pressure instruments, level indicators, flow meters, and gas detectors should undergo appropriate functional tests where installed. The programmable logic controller (PLC) and human-machine interface (HMI) should be checked for correct input and output mapping, alarm behavior, interlock logic, and operating sequences. Emergency stops and other protective functions require documented verification. These checks are essential. An instrument may display a plausible reading while transmitting an incorrect signal or responding too slowly. Functional verification helps identify such discrepancies before hot commissioning. Cold Commissioning and System Verification Cold commissioning tests equipment without introducing the full thermal load or conducting normal feedstock processing. Its purpose is to confirm mechanical readiness and verify that individual systems operate as intended. Typical activities include: Checking motor rotation, drive alignment, and conveyor movement. Verifying valve positions, pipeline connections, and cooling-water circulation. Testing control sequences, alarms, and emergency shutdown functions. Inspecting electrical protection and confirming instrument responses. Checking accessible joints and connections for leakage using approved methods. The commissioning team should record test results, unresolved defects, corrective actions, and approval status. Outstanding deficiencies affecting safety or equipment integrity must be addressed before the plant proceeds to hot commissioning. Hot Commissioning and Performance Testing Hot commissioning introduces thermal energy and establishes operating conditions under controlled procedures. Startup should follow the supplier's sequence for heating, gas handling, pressure management, and process stabilization. Once operating temperatures are established, suitable feedstock can be introduced according to the approved commissioning plan. Operators monitor temperature trends, pressure where applicable, gas flow, condensation performance, and discharge behavior. Abnormal fluctuations should be investigated rather than compensated for through arbitrary parameter changes. Performance testing then evaluates whether the plant meets agreed acceptance criteria. Relevant indicators may include: Feedstock throughput over a defined operating period. Liquid, gas, and solid product distribution. Specific fuel or energy consumption. Temperature stability and process continuity. Condensation performance and emissions-related measurements. Reliability of feeding, discharge, and auxiliary systems. Testing conditions must be documented, including feedstock composition, moisture content, operating hours, and measurement methods. These variables can materially affect results. Product yields should not be compared directly when feedstock properties or test conditions differ substantially. Documentation, Training, and Operational Handover Commissioning concludes with a structured handover. Essential records include approved drawings, equipment manuals, electrical schematics, calibration certificates, inspection reports, performance-test results, and maintenance schedules. Operators should receive practical training in startup, shutdown, routine inspection, alarm response, and emergency procedures. Spare-parts inventories and maintenance responsibilities should also be established before normal operation begins. A properly installed Beston pyrolysis plant depends on disciplined execution at every stage, from foundation preparation to performance verification. Systematic commissioning reduces avoidable startup problems, establishes a documented operating baseline, and provides evidence that the installed equipment performs according to the agreed technical requirements.
By Cathy Wang • October 26, 2026
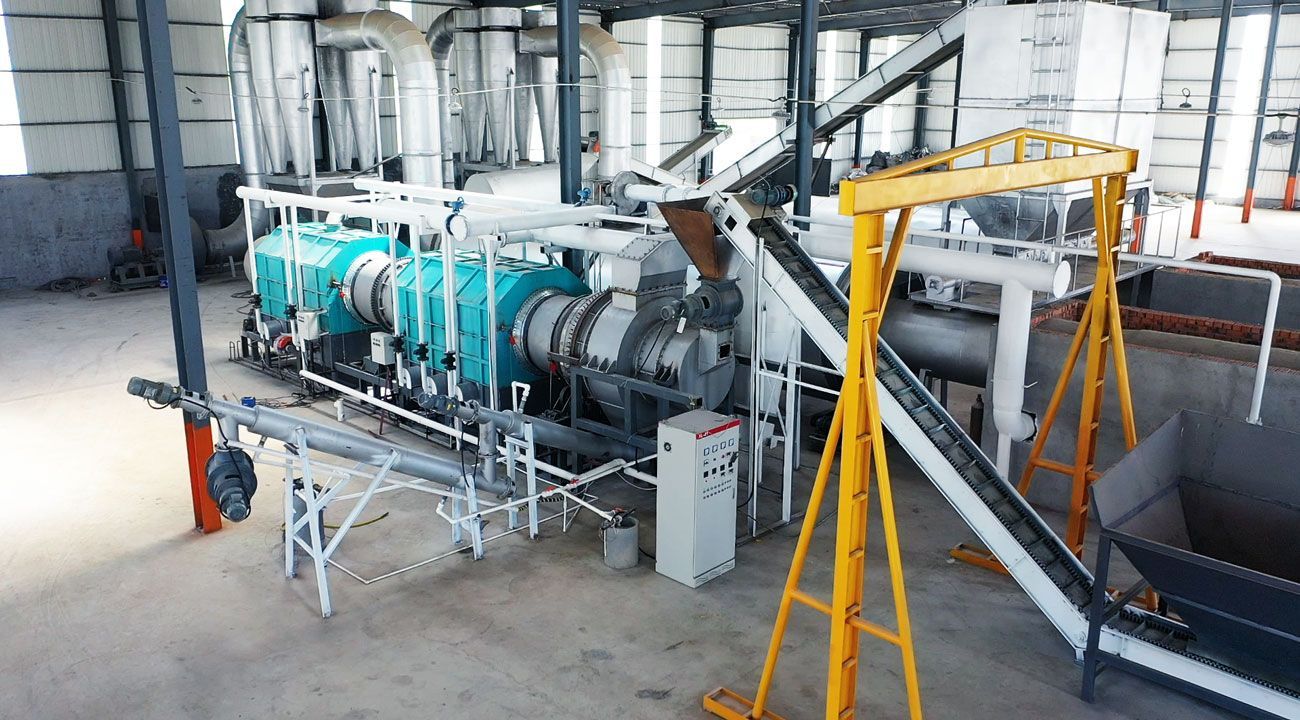
Emission treatment is an essential component of a coconut shell charcoal machine, particularly when carbonization operates at commercial scale. Thermal decomposition of coconut shells generates particulate matter, condensable vapors, and combustible gases that require appropriate collection, treatment, or controlled combustion. The composition and volume of these emissions depend on feedstock moisture, carbonization temperature, reactor configuration, and operating conditions. An effective treatment system must address each emission stream while maintaining thermal efficiency, operational safety, and compliance with applicable environmental requirements. Dust Collection During Feedstock Handling and Charcoal Discharge Dust can arise during coconut shell crushing, screening, conveying, carbonization residue handling, and finished charcoal packaging. Fine particles may become airborne during material transfer, creating housekeeping challenges and increasing the risk of dust accumulation around mechanical equipment. Source capture is generally more effective than relying exclusively on general ventilation. Enclosed conveyors, covered transfer points, and appropriately positioned extraction hoods can limit the dispersion of particulate matter. Depending on particle characteristics and gas conditions, cyclones or bag filters may be incorporated into the dust collection system. Cyclones separate particles through centrifugal force and are often used as a preliminary collection stage. Bag filters capture finer particulates by passing gas through porous filter media. Their suitability depends on gas temperature, humidity, particle loading, and the potential presence of combustible dust. Several operating considerations are important: Temperature control: Gas entering a filter must remain within the filter media's permissible temperature range. Moisture management: Excessive humidity can cause particle agglomeration or filter blinding. Pressure-drop monitoring: Increasing pressure drop may indicate dust accumulation or restricted airflow. Fire prevention: Charcoal fines and hot particles require appropriate isolation, housekeeping, and fire-protection measures. Dust collection equipment should be selected according to the actual gas stream. Hot, dust-laden process gas may require cooling or preliminary separation before fine filtration. Managing Pyrolysis Vapors and Condensable Compounds During carbonization, the organic constituents of coconut shells decompose and release vapors containing water vapor and various organic compounds. As these vapors cool, some components condense into liquid fractions, while others remain gaseous. The vapor-treatment arrangement must account for this changing composition. In systems designed to recover condensable products, heat exchangers or condensers lower the vapor temperature, allowing suitable compounds to be separated from the gas stream. The resulting liquids may contain mixtures of water and organic substances, depending on the process configuration and feedstock characteristics. Uncondensed gases require further management. Sending untreated vapor directly to the atmosphere can result in odorous emissions and the release of organic pollutants. A properly engineered system may route combustible non-condensable gases to a controlled combustion chamber, provided that the gas composition, heating value, and operating conditions are suitable. Condensation performance depends on cooling capacity, gas flow, temperature, and the properties of the vapor mixture. Fouling can reduce heat-transfer efficiency, while inadequate condensate drainage may impair separation. Routine inspection and accessible cleaning arrangements are therefore important design considerations for a coconut shell charcoal machine . Combustion Gas Treatment and Heat Utilization Combustion gases are generated when fuel or recovered combustible gas is burned to provide process heat. Their composition depends on the fuel, combustion temperature, oxygen availability, burner design, and operating stability. Potential pollutants include particulate matter, carbon monoxide, nitrogen oxides, and other compounds associated with the feedstock and combustion conditions. Sulfur-containing compounds may also require consideration where relevant to the incoming material. Combustion control is the first line of emission management. Adequate mixing, appropriate residence time, sufficient oxygen, and stable temperature help promote more complete oxidation of combustible compounds. Secondary treatment may be necessary to meet site-specific emission limits. Depending on the measured emissions and applicable regulations, the treatment train may include particulate filtration, wet scrubbing, or other pollutant-specific controls. Wet scrubbers can remove certain soluble gases and particulates, but they generate wastewater that must be managed appropriately. Heat recovery can improve the thermal efficiency of a coconut shell charcoal machine. Suitable exhaust heat may be used for feedstock drying or combustion-air preheating, subject to temperature constraints, corrosion risks, and the requirements of the emission-control system. Heat recovery should not compromise adequate combustion or downstream pollutant removal. Monitoring and Integrated System Design Emission treatment performs most reliably when collection, condensation, combustion, and exhaust purification are designed as an integrated system. Poor coordination can create pressure fluctuations, inadequate gas flow, excessive condensation in unsuitable locations, or unstable burner operation. Temperature sensors, pressure gauges, gas-flow measurements, and periodic exhaust testing help operators identify deviations. Monitoring should focus on parameters relevant to the actual process and local environmental requirements. Maintenance schedules should address filter cleaning, condenser inspection, condensate removal, and combustion-system verification. Ultimately, emission management for a coconut shell charcoal machine requires more than installing a single filtration device. Dust, condensable vapors, and combustion gases have different physical and chemical properties, so each stream needs an appropriate treatment strategy. A coordinated design can reduce uncontrolled emissions, support stable carbonization, improve heat utilization, and strengthen the plant's environmental performance.
By Cathy Wang • October 26, 2026
Recovered carbon black (rCB) is emerging as a valuable material in the tire recycling industry. Produced during waste tire pyrolysis, raw carbon black contains carbonaceous residues, inorganic ash, residual oils, and sulfur-containing compounds. In its untreated form, this material often has inconsistent quality and limited applications, resulting in a lower market value than virgin commercial carbon black. However, through grinding, classification, pelletizing, and appropriate purification or surface modification, recovered carbon black can be upgraded into a more consistent industrial filler for rubber and plastic products. 1. Why Raw Carbon Black Has Limited Market Value During waste tire pyrolysis plant , rubber polymers decompose under oxygen-limited conditions, producing pyrolysis oil, non-condensable gas, steel wire, and a solid carbon-rich residue. This solid residue is commonly called raw pyrolysis char. Unlike virgin carbon black, which is manufactured under controlled conditions to achieve specific particle characteristics, raw pyrolysis char retains some of the original tire components. Its properties depend on the tire composition, pyrolysis temperature, residence time, and reactor design. Several factors limit its direct use in industrial manufacturing: High ash content: Silica, zinc compounds, and other inorganic residues from tire additives can reduce the proportion of usable carbon. Residual oil and volatile matter: Incomplete removal of organic compounds can affect processing behavior and product consistency. Sulfur-containing compounds: Sulfur originating from tire vulcanization may remain in the recovered material and influence certain applications. Uneven particle size: Agglomerated particles and coarse residues can cause dispersion problems in rubber compounds. Variable reinforcing performance: Surface chemistry, aggregate structure, and particle characteristics may differ substantially from those of virgin carbon black. These limitations explain why raw carbon black generally sells at a discount. To unlock its commercial potential, producers must focus on improving material quality rather than simply increasing the amount of char recovered from each ton of waste tires. 2. Grinding and Classification Improve Material Consistency Grinding is one of the first steps in upgrading raw pyrolysis char. The objective is to reduce oversized particles, break down agglomerates, and produce a more uniform powder suitable for downstream processing. Industrial milling systems can include impact mills, pin mills, or other grinding equipment selected according to the characteristics of the feed material. Classification equipment separates particles according to size, helping manufacturers maintain consistent product specifications. However, finer grinding does not automatically produce better reinforcing performance. Carbon black's behavior in rubber also depends on aggregate structure, surface area, surface chemistry, and dispersion. Excessive grinding can increase energy consumption without delivering a proportional improvement in final product performance. Magnetic separation and screening may also be necessary to remove residual steel fragments and coarse contaminants before milling. For commercial production, particle size distribution should be monitored alongside ash content, moisture, and other relevant properties. These measurements help establish repeatable product quality and reduce the risk of inconsistent performance during compounding. 3. Pelletizing Improves Handling and Transportation Fine recovered carbon black powder can create dust during conveying, storage, and feeding. It may also have poor flowability, making accurate dosing more difficult in industrial production lines. Pelletizing addresses these handling problems by compressing or agglomerating the powder into small granules. Depending on the formulation and intended application, the process may use water, binders, or other processing aids. The main benefits include: Reduced dust generation during handling. Improved flowability and feeding consistency. Easier storage, packaging, and transportation. More convenient integration into automated rubber and plastic compounding systems. Pellet quality is important. Pellets that are too hard may disperse poorly during mixing, while those with insufficient strength may break apart and generate dust. Binder selection and dosage must also be controlled because they can affect moisture content, mixing behavior, and the properties of the finished compound. Pelletizing primarily improves handling characteristics. It does not independently remove ash, reduce sulfur content, or guarantee that recovered carbon black meets a particular industrial grade. 4. Purification and Modification Increase Commercial Value After physical processing, additional treatments may be required to improve the chemical and functional properties of recovered carbon black. De-oiling and volatile matter removal Residual organic compounds can be reduced through suitable thermal treatment, extraction, or other purification processes. The appropriate method depends on the initial char composition and the target product specifications. Better control of volatile matter can improve product consistency, although treatment conditions must be carefully selected to avoid unnecessary energy consumption or changes to desirable carbon characteristics. Ash reduction and desulfurization Ash reduction can involve chemical treatment, washing, or other separation methods. Desulfurization may use thermal, chemical, or combined processes, depending on the sulfur compounds present. These treatments can improve the suitability of recovered carbon black for selected applications, but they also introduce additional costs and potential environmental challenges. Chemical treatment may generate wastewater or secondary residues that require appropriate management. Producers should evaluate the improvement in product performance against the costs of reagents, energy, wastewater treatment, and material losses. Surface modification Surface treatment can alter the interactions between recovered carbon black and the surrounding polymer matrix. Depending on the treatment, it may improve compatibility, dispersion, or selected mechanical properties. The best modification strategy should be determined through laboratory testing and application-specific trials rather than assumed to work equally well for every recovered carbon black product. 5. Can Recovered Carbon Black Replace N330 or N660? Recovered carbon black can replace part of the virgin carbon black used in certain rubber compounds, but substitution depends on the application and the quality of the recovered material. N330 is commonly used in tire treads and other applications requiring relatively strong reinforcement. N660 is generally associated with lower reinforcement and lower hysteresis requirements than N330 in many rubber formulations. These grades have defined performance characteristics. Matching their particle size alone is insufficient because reinforcing behavior also depends on surface area, structure, surface chemistry, and dispersion. A practical evaluation should consider: Iodine adsorption or other surface-area indicators. Oil absorption or structure-related measurements. Ash, sulfur, moisture, and volatile matter. Particle size distribution and dispersion quality. Tensile strength, elongation, hardness, abrasion resistance, and other application-specific properties of the finished compound. Rather than claiming that all recovered carbon black can directly replace N330 or N660, manufacturers should establish substitution ratios through controlled trials. In some formulations, rCB may partially replace virgin carbon black while maintaining acceptable performance. Other demanding applications may require additional purification, modification, or blending with virgin grades. 6. Applications in Rubber and Plastic Manufacturing The commercial opportunities for upgraded recovered carbon black extend beyond tire recycling. In rubber products, potential applications include conveyor belts, rubber mats, hoses, molded components, and selected automotive rubber parts. The appropriate use depends on mechanical requirements, product safety standards, and the consistency of the recovered material. In plastics, recovered carbon black may be incorporated into selected masterbatches and polymer compounds where its color, dispersion, contamination level, and processing behavior meet customer specifications. Testing is especially important for products requiring consistent appearance, electrical performance, or stringent mechanical properties. Market entry generally begins with less demanding applications before progressing toward products requiring higher reinforcement and tighter quality control. Conclusion Recovered carbon black offers tire pyrolysis operators an opportunity to move beyond selling low-value raw char. Grinding and classification improve physical consistency, pelletizing facilitates handling, and targeted purification or surface modification can expand the range of potential applications. The key to commercial success is not simply producing more recovered carbon black, but developing a consistent material that meets measurable customer requirements. By combining appropriate post-processing equipment, quality control, and application-specific testing, producers can improve product value, reduce dependence on virgin raw materials, and strengthen the economics of waste tire pyrolysis.