Enhancing Thermal Efficiency in Plastic Pyrolysis Reactor
Cathy Wang • April 2, 2025

In pyrolysis processes, thermal efficiency plays a vital role in determining the overall effectiveness of the reactor and the quality of the products generated. Plastic pyrolysis is no exception. A high level of thermal efficiency can significantly reduce operational costs, improve energy utilization, and increase product yield, making the pyrolysis process more economically viable. Optimizing the thermal efficiency of a plastic pyrolysis reactor involves various strategies, from improving heat transfer mechanisms to utilizing waste heat. This article explores effective ways to achieve higher thermal efficiency, thereby maximizing the performance and profitability of the pyrolysis operation.

Optimizing Reactor Design

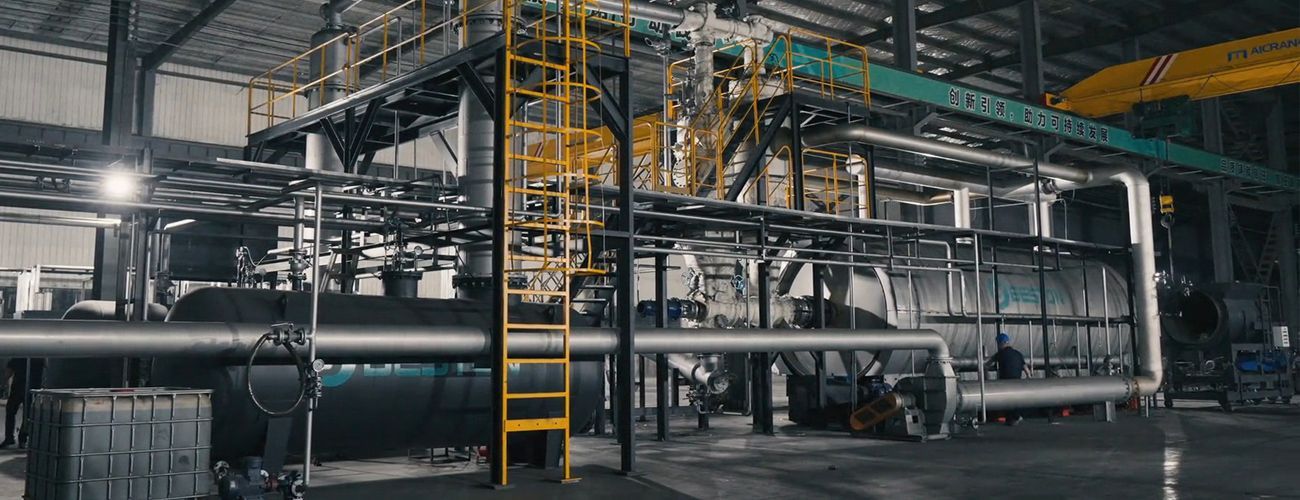
The design of the plastic pyrolysis reactor is one of the most critical factors influencing its thermal efficiency. Enhancing the design for better heat retention and transfer can have a direct impact on the overall energy consumption of the process.

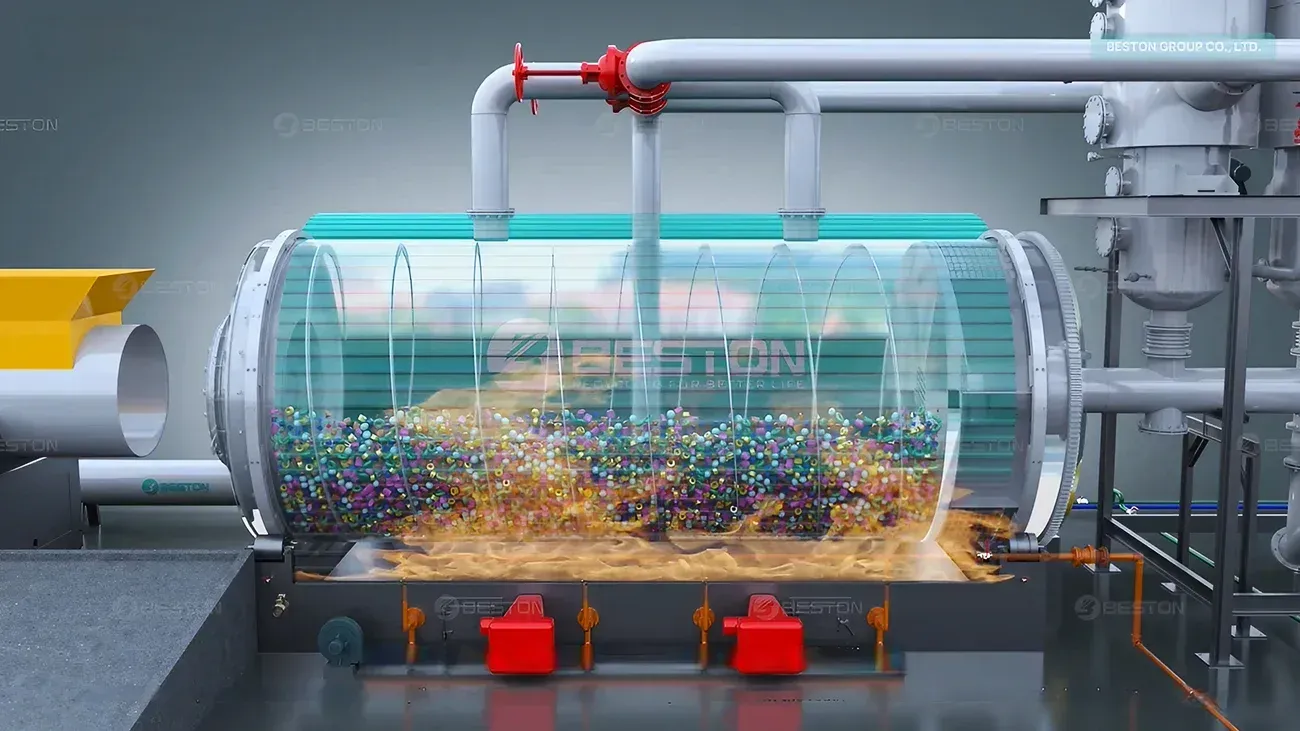
  1. Double or Multi-Chamber Reactors: Many modern pyrolysis reactors incorporate double or multi-chamber designs. These systems allow for more effective heat circulation and provide more space for the heat to penetrate the feedstock. As the waste plastic enters the reactor, the multiple chambers enable better heat distribution, ensuring more uniform temperatures throughout the material. This reduces energy losses and ensures that the feedstock is exposed to optimal temperatures for the thermal decomposition process.
  2. Insulation: Proper insulation is crucial for maintaining high thermal efficiency. By ensuring that the reactor is well-insulated, heat losses to the environment are minimized. This not only saves energy but also stabilizes the temperature inside the reactor, improving the consistency of the pyrolysis process. High-quality insulation materials, such as ceramic fiber or mineral wool, can provide effective thermal barriers, keeping the heat within the reactor and ensuring optimal operating conditions.
  3. Heat Recovery Systems: Heat recovery is a crucial element in improving thermal efficiency. Incorporating a heat recovery system, such as a heat exchanger, can significantly reduce energy consumption. In a typical plastic pyrolysis reactor, much of the heat is produced during the pyrolysis process and can be captured and reused to pre-heat the incoming feedstock. This reduces the reliance on external energy sources and increases the overall thermal efficiency of the reactor.

Managing Temperature Control

Precise temperature control is essential to the pyrolysis process, as the breakdown of plastics into useful products depends on maintaining the right thermal conditions.

  1. Automatic Temperature Regulation: Pyrolysis reactors can benefit from automated temperature control systems, which allow for precise regulation of internal temperatures. By using sensors and advanced control systems, the reactor can maintain a stable temperature, minimizing fluctuations that can cause inefficiencies. Maintaining optimal temperatures ensures that the plastic feedstock undergoes thermal decomposition at the most efficient rate, without the waste of energy due to overheating or underheating.
  2. Temperature Profiling: Dividing the pyrolysis reactor into multiple temperature zones can also help to optimize the thermal efficiency. By implementing different temperature settings for each zone, the reactor can ensure that the feedstock receives the appropriate level of heat at different stages of the pyrolysis process. This enables a more controlled breakdown of plastics, improving the overall yield of bio-oil, gas, and carbon black, and reducing energy waste.
  3. Advanced Heating Systems: Using advanced heating methods, such as indirect heating or electromagnetic heating, can also improve thermal efficiency. Indirect heating systems reduce the loss of energy to the environment and provide a more uniform heat distribution within the reactor. Electromagnetic heating, on the other hand, allows for more direct and efficient energy transfer to the feedstock, making the pyrolysis process faster and more energy-efficient.

Utilizing Waste Heat

Pyrolysis reactors generate significant amounts of waste heat during the process, and this heat, if not utilized efficiently, represents a lost opportunity for increasing thermal efficiency. Using waste heat to supplement energy needs within the reactor can drastically improve overall performance.

  1. Pre-heating Feedstock: Waste heat can be used to pre-heat incoming plastic feedstock before it enters the pyrolysis reactor. This step reduces the energy required to reach the desired reaction temperature, saving fuel or electricity. In this way, the reactor can operate with lower energy inputs while achieving the same or better output.
  2. Syngas Utilization: The syngas produced during the pyrolysis process can be used as a secondary energy source to power the reactor. By utilizing syngas in the reactor’s burner, operators can reduce dependency on external energy supplies. This process of self-sustaining heat generation through the use of syngas significantly increases the thermal efficiency of the reactor and reduces operational costs.
  3. Co-generation of Power: Another method of utilizing waste heat is through co-generation, where waste heat is captured and converted into electrical power. In this setup, the pyrolysis plant can generate its own electricity, reducing the need for grid power. This not only improves thermal efficiency but also enhances the sustainability of the pyrolysis operation by lowering its carbon footprint.

Improving Heat Transfer

Efficient heat transfer within the reactor is essential for maintaining thermal efficiency. The quality of the heat exchange between the heating elements and the feedstock directly impacts how well the reactor operates.

  1. Optimized Reactor Geometry: Adjusting the geometry of the reactor can enhance heat transfer efficiency. For example, incorporating spiral or helical designs in the reactor walls increases surface area contact, thereby improving the transfer of heat from the walls to the feedstock. This design ensures that more of the heat produced is effectively used for the pyrolysis process, reducing energy waste.
  2. Enhanced Stirring Mechanisms: In some reactors, the feedstock is stirred during the pyrolysis process to ensure better heat distribution. Using advanced stirring mechanisms that create uniform mixing of the plastic materials can significantly improve the overall heat distribution within the reactor, ensuring that all materials are uniformly exposed to the required temperature.

Advanced Materials and Coatings

The material composition of the reactor plays a pivotal role in its thermal efficiency. Special coatings and materials that enhance heat retention or improve heat conductivity can make a considerable difference.

  1. Reactor Lining: Lining the interior of the reactor with materials that are highly resistant to heat can improve both durability and thermal efficiency. High-performance refractory materials or heat-resistant ceramics are often used in the construction of reactors to ensure long-term stability and minimal energy loss.
  2. Thermal Coatings: Applying advanced thermal coatings to the reactor surfaces can further reduce heat loss. These coatings reflect heat back into the reaction chamber, ensuring that more energy is retained within the system and less is lost to the surrounding environment.
By Cathy Wang • October 13, 2026
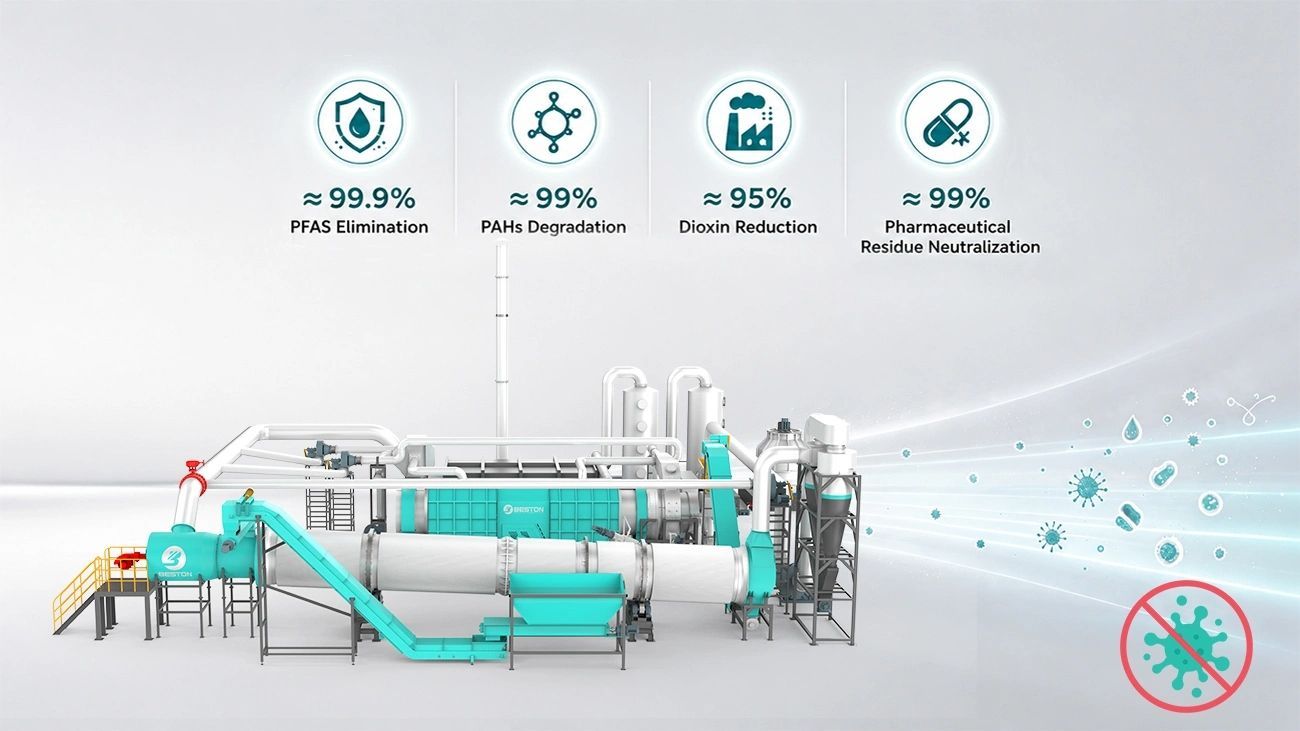
Municipal sewage sludge carbonization is a potential solution for reducing sludge volume, recovering carbon-rich materials, and improving waste management efficiency. However, its feasibility depends on several critical factors, including heavy metal behavior, feedstock moisture content, energy consumption, and the final destination of the carbonized product. Before investing in a carbonization project, operators need to evaluate both technical performance and environmental compliance. 1. How Does Municipal Sewage Sludge Carbonization Work? Municipal sewage sludge is generated during wastewater treatment and typically contains organic matter, inorganic minerals, water, and potentially hazardous contaminants. Carbonization uses controlled heating under oxygen-limited conditions to convert part of the organic matter into a carbon-rich solid product. Compared with conventional disposal methods, carbonization can reduce the volume of sludge requiring further management and may recover useful energy from volatile compounds. Depending on the feedstock and operating conditions, the process can also produce combustible gases and condensable vapors that require appropriate collection and treatment. A complete sewage sludge treatment plant may include sludge dewatering, drying, carbonization, gas treatment, and product handling systems. Integrating these processes helps improve operational stability and provides a clearer basis for evaluating overall project economics. 2. Heavy Metal Treatment: A Critical Feasibility Factor Heavy metals are one of the main concerns when converting municipal sewage sludge into carbonized products. Sludge may contain lead, cadmium, chromium, mercury, nickel, copper, and zinc, depending on the wastewater sources and treatment processes. Carbonization does not automatically eliminate heavy metals. Many metals remain in the solid residue, and their concentrations may increase as organic matter and water are removed. Changes in temperature and chemical composition can also affect metal speciation, mobility, and leachability. Certain volatile elements, particularly mercury and some metal compounds, may transfer into the gas phase and require effective emission controls. Therefore, feasibility studies should include several important measures. - Feedstock testing: Analyze representative sludge samples for total heavy metal concentrations and other relevant contaminants. - Process evaluation: Assess how carbonization temperature, residence time, and feedstock composition influence contaminant distribution. - Emission control: Design suitable gas collection, particulate removal, and exhaust treatment systems based on the expected pollutants. - Product testing: Evaluate heavy metal concentrations, leaching characteristics, and compliance with the intended end-use standards. If the carbonized product is intended for agricultural use, soil improvement, or other beneficial applications, compliance must be demonstrated under the applicable local regulations. If contaminant levels exceed permitted limits, controlled disposal or further treatment may be necessary. 3. What Moisture Content Is Required Before Carbonization? Moisture content directly affects the energy demand and operating cost of sludge carbonization. Fresh municipal sewage sludge often contains substantial amounts of water, making direct thermal treatment energy-intensive. A large proportion of the available heat may otherwise be consumed by water evaporation rather than by the carbonization process. Mechanical dewatering is generally the first step in reducing moisture content. Equipment such as filter presses or centrifuges can remove part of the water before thermal drying. A drying system can then reduce the moisture level to a range suitable for the selected carbonization equipment. There is no universal moisture requirement for every project. The appropriate inlet moisture content depends on reactor design, feedstock characteristics, heat source, and the availability of waste heat. Many thermal carbonization systems benefit from drying sludge to approximately 10%–20% moisture before feeding, but this range should be confirmed with equipment specifications and process testing. Feasibility calculations should compare the energy required for drying with the recoverable energy from process gases and other available heat sources. Waste heat recovery, efficient insulation, and automated temperature control may reduce operating costs. However, the energy balance must be calculated using actual sludge properties rather than theoretical assumptions alone. 4. Where Can the Final Carbonized Product Go? The commercial value of municipal sludge carbonization depends heavily on whether the final product has a safe and legally acceptable destination. Potential pathways include the following. - Construction materials: Subject to technical testing and regulatory approval, treated sludge-derived solids may be evaluated as components in selected building materials. - Land application: Agricultural or soil-related use requires strict assessment of heavy metals, organic contaminants, stability, and applicable product standards. Carbonization alone does not establish suitability. - Industrial applications: Certain products may be considered for mineral-based or carbon-containing industrial uses if their properties meet the required specifications. - Controlled disposal: Material that fails safety or quality requirements may need to be managed at an authorized disposal facility. Before selecting a destination, project developers should consult potential end users and regulatory authorities. Product testing should cover not only contaminant levels but also relevant physical and chemical properties, such as calorific value, ash content, and stability. 5. How to Evaluate Project Feasibility A reliable feasibility study should combine technical, environmental, and financial assessments. Key inputs include daily sludge throughput, initial and target moisture content, organic matter content, heavy metal concentrations, energy prices, and local disposal fees. Capital expenditure should account for dewatering and drying equipment, the carbonization reactor, exhaust treatment, material handling, and safety systems. Operating costs should include electricity, supplementary fuel, maintenance, laboratory testing, and residue management. Revenue from recovered energy or carbonized products should only be included when supported by realistic market demand and regulatory approval. Pilot testing is particularly valuable when sludge composition varies significantly or when the intended product has strict quality requirements. It helps verify drying performance, energy consumption, contaminant behavior, product quality, and the suitability of the proposed treatment process. Conclusion Municipal sewage sludge carbonization can offer a practical route for sludge volume reduction and resource recovery, but it is not automatically a safe or profitable solution. Heavy metal behavior, moisture control, energy efficiency, and final product utilization must be assessed together. By conducting feedstock analysis, process testing, environmental evaluations, and market research before investment, project developers can make better-informed decisions and establish a treatment system that meets local requirements.
By Cathy Wang • October 13, 2026
Ash management is an important operational consideration in charcoal production because the mineral fraction of biomass directly influences the quality, purity, and end-use suitability of the final product. In charcoal making equipment, ash originates primarily from inorganic constituents naturally present in the feedstock, including calcium, potassium, magnesium, silica, iron, and other mineral compounds. These substances remain largely in the solid residue during carbonization, although their chemical forms and distribution may change with temperature. Effective ash control therefore begins with feedstock characterization and continues through carbonization, discharge, and post-production quality assessment. Mineral Content and Ash Formation During Carbonization The ash content of charcoal depends on both feedstock composition and processing conditions. Wood from clean, debarked sources generally contains relatively low concentrations of inorganic minerals, whereas agricultural residues, bark, straw, and certain industrial biomass streams may contain substantially higher mineral fractions. During carbonization, volatile organic compounds are released while much of the nonvolatile mineral matter remains in the char. Consequently, the relative ash concentration can increase as organic mass is removed, even when the absolute quantity of minerals changes very little. Mineral composition also affects the thermal behavior of the feedstock. Potassium and calcium compounds can catalyze certain reactions during biomass decomposition, while silica-rich materials may contribute to refractory deposits or abrasive residues. These effects vary with mineral speciation, temperature, and interactions among inorganic constituents. For charcoal producers, measuring total ash alone is insufficient. Mineral composition provides additional information about process behavior and product suitability. Effects of Ash Content on Final Charcoal Quality High ash content reduces the proportion of combustible carbon in charcoal on a mass basis. This can lower its effective heating value and increase the quantity of inert material delivered to downstream users. The consequences extend beyond energy performance. In metallurgical applications, excessive mineral impurities may affect reactivity, slag formation, and process consistency. For barbecue charcoal, elevated ash levels can increase residual material after combustion and influence handling characteristics. In activated-carbon production, mineral impurities may obstruct pores or interfere with subsequent activation, depending on their composition and distribution. Ash is not always undesirable. In agricultural biochar, selected minerals can contribute nutrients and influence soil chemical properties. Calcium, magnesium, and potassium may provide agronomic value, although their availability depends on their chemical forms. Conversely, feedstocks contaminated with heavy metals can produce ash-rich char that requires additional safety assessment. The appropriate ash specification therefore depends on the intended application rather than a universal maximum threshold. Feedstock Selection and Mineral Contamination Control Feedstock preparation is the first practical measure for managing ash. Raw materials should be assessed for moisture, mineral content, soil contamination, and the presence of extraneous inorganic matter. Soil and sand adhering to biomass can increase ash content without contributing useful nutrients. Mechanical screening, effective storage practices, and suitable cleaning procedures can reduce this contamination before material enters charcoal making equipment . Feedstock blending may also help stabilize mineral content when several biomass sources are available. However, blending should follow laboratory analysis because combining materials with different mineral profiles does not necessarily produce predictable ash characteristics. Periodic testing of representative feedstock samples allows operators to identify seasonal variations and adjust process settings accordingly. Carbonization Temperature and Ash Management Carbonization temperature affects residual carbon content, mineral transformations, and the physical structure of the resulting charcoal. Higher temperatures generally promote greater devolatilization, potentially increasing ash concentration on a mass basis. Certain minerals may also undergo phase transformations, sintering, or changes in solubility. Excessive temperatures do not automatically improve charcoal quality. The optimal operating range depends on feedstock characteristics, reactor design, residence time, and product requirements. A controlled heating profile helps maintain consistent carbonization and reduces variability between production batches. Operators should monitor temperature distribution, feeding conditions, and discharge performance rather than relying on a single nominal temperature. Ash separation after carbonization may remove loose mineral contaminants, but it cannot reliably eliminate minerals embedded within the char matrix. Prevention at the feedstock stage is therefore more effective than depending entirely on downstream separation. Quality Testing and Operational Monitoring A structured quality-control program should combine laboratory analysis with routine equipment inspection. Relevant measurements include total ash content, fixed carbon, volatile matter, moisture, and calorific value. Where contamination is a concern, elemental analysis can identify specific minerals and potentially hazardous metals. Testing should use representative samples and consistent analytical methods. Comparing results across production runs helps distinguish feedstock-related changes from operational variability. For industrial producers, the most effective ash-management strategy integrates feedstock screening, mineral characterization, controlled carbonization, and application-specific product testing. This approach enables charcoal making equipment to deliver more consistent output while reducing contamination risks, improving resource utilization, and aligning final charcoal quality with the technical requirements of its intended market.
By Cathy Wang • September 29, 2026
The performance of a plastic pyrolysis system is often evaluated by production capacity and energy efficiency. However, product quality remains equally important. In a commercial operation, the composition and consistency of pyrolysis oil, combustible gas, and solid residues determine the potential value of the final products and influence downstream applications. For investors exploring a plastic to oil machine for sale , understanding the factors that affect product quality is essential for making informed technical and economic decisions. Feedstock Composition Determines Product Characteristics Plastic feedstock is the primary variable influencing pyrolysis output. Different polymers exhibit distinct thermal decomposition pathways, resulting in variations in oil composition, gas yield, and solid residue formation. Polyolefin materials such as polyethylene (PE) and polypropylene (PP) generally produce higher liquid yields because their molecular structures favor hydrocarbon generation during pyrolysis. Polystyrene (PS) can generate aromatic compounds, while plastics containing chlorine, oxygen, or other heteroatoms may require additional process control due to the formation of undesirable by-products. Feedstock purity is equally important. Metal fragments, dirt, moisture, and non-target materials can alter thermal behavior and affect the consistency of products. A stable and well-prepared feedstock stream contributes to more predictable operation and product quality. Temperature Control Influences Product Distribution Pyrolysis is fundamentally a temperature-driven process. Reactor temperature affects the extent of polymer cracking and determines the relative proportion of liquid, gas, and solid products. Lower temperatures may lead to incomplete decomposition and higher residue content. Excessively high temperatures, by contrast, can promote secondary cracking reactions, converting condensable hydrocarbons into permanent gases. Maintaining a suitable temperature window allows the system to balance liquid production with gas generation. Temperature uniformity is equally significant. Thermal gradients within the reactor can create heterogeneous reaction zones, leading to fluctuations in product composition. Continuous monitoring and automated control systems help maintain stable operating conditions. Residence Time and Vapor Management The duration that plastic and pyrolysis vapors remain inside the reactor also affects final products. Longer residence times can increase secondary reactions, altering hydrocarbon distribution and reducing the proportion of heavier liquid fractions. Vapor handling systems therefore play an important role. Efficient condensation equipment enables the recovery of condensable hydrocarbons while separating non-condensable gas for energy utilization. The design of condensers, cooling systems, and gas pipelines influences heat transfer efficiency and can affect the composition of collected oil. Insufficient cooling may result in the loss of valuable hydrocarbons, while excessive cooling can increase operational complexity. Role of Non-Condensable Gas Non-condensable gas generated during pyrolysis contains combustible components that can contribute to process heating after suitable treatment. This internal energy circulation reduces dependence on external fuel sources and improves thermal efficiency. Gas composition depends on feedstock type, reactor temperature, and operating conditions. Hydrogen, methane, and light hydrocarbons may be present in varying proportions. Their effective utilization can improve overall energy management within the plant. For buyers comparing a plastic to oil machine for sale , the ability to recover and utilize process gas should be considered alongside reactor design and production capacity. Formation and Management of Solid Residues Solid residues represent the non-volatile fraction remaining after thermal decomposition. Their quantity and characteristics are affected by feedstock composition, operating temperature, and process stability. In plastic pyrolysis, residue may contain carbonaceous material, inorganic additives, pigments, fillers, and traces of contaminants. Excessive residue generation can indicate incomplete conversion or unsuitable feedstock preparation. Residue handling systems therefore form an important part of plant design. Efficient discharge and collection support continuous operation while reducing maintenance requirements. Integrating Quality Control into Plant Operation Product quality does not depend on a single parameter. It results from the interaction of feedstock preparation, temperature management, residence time, vapor recovery, and residue control. For companies evaluating a plastic to oil machine for sale , technical assessment should extend beyond nominal production capacity. Feedstock compatibility, thermal stability, condensation efficiency, gas utilization, and residue management all influence the consistency and value of final products. A well-designed pyrolysis system combines these elements into an integrated process. Stable operation, controlled reaction conditions, and effective product recovery can improve the quality of oil, gas, and solid residues while supporting more efficient resource utilization from plastic waste.