5 Advantages of Mobile Pyrolysis Plant

Cathy Wang • August 22, 2024

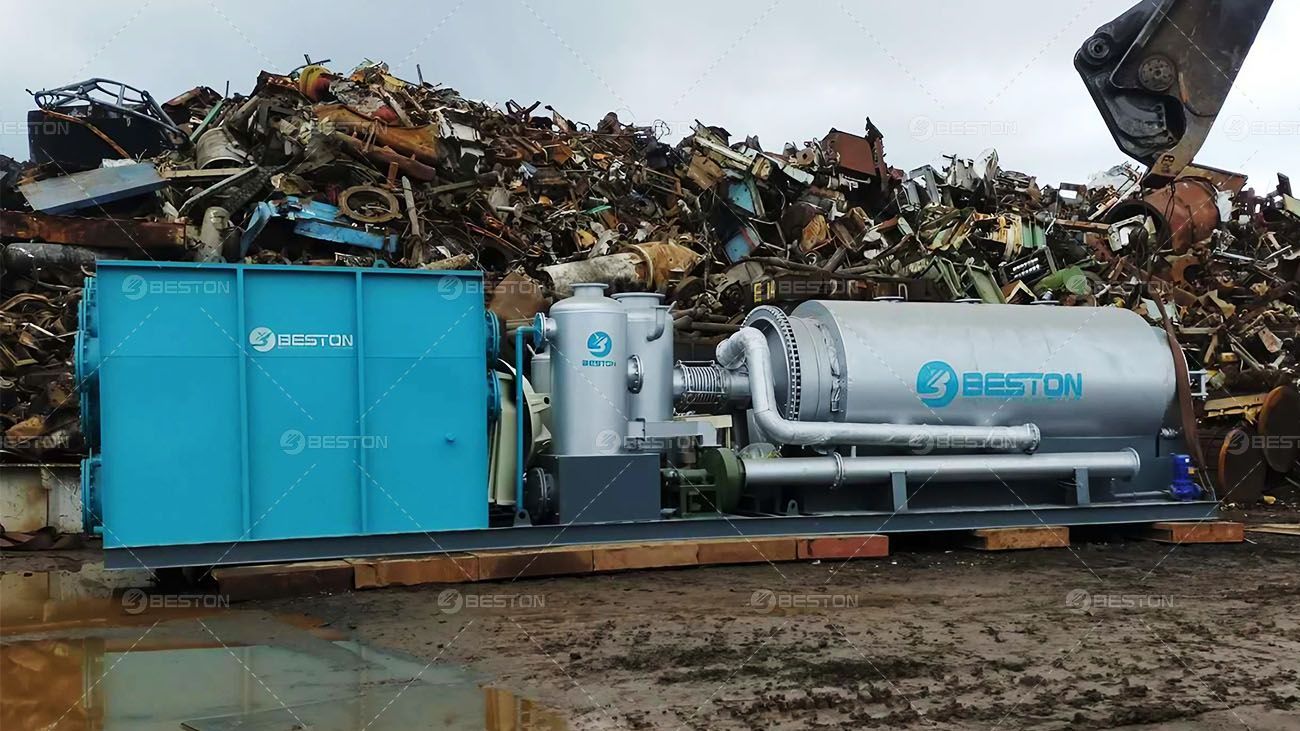
The advent of mobile pyrolysis plant technology represents a significant advancement in the field of waste management. These mobile units offer a versatile and efficient solution for converting waste into valuable byproducts such as bio-oil, syngas, and char. Unlike traditional stationary plants, mobile pyrolysis plants can be transported directly to waste sites, offering a unique set of advantages that make them increasingly popular in various industries. This article explores five key advantages of mobile pyrolysis plants, highlighting their impact on waste management and sustainability.

1. Enhanced Flexibility and Accessibility

A primary advantage of mobile pyrolysis plant is the inherent flexibility. Traditional stationary pyrolysis plants require significant infrastructure, including land acquisition, construction, and permanent installation. In contrast, mobile pyrolysis plants are designed to be compact and transportable, allowing them to be deployed directly to the location where waste is generated. This flexibility significantly reduces the need for waste transportation, cutting down on associated costs and environmental impacts.

Mobile pyrolysis plants can access remote or otherwise inaccessible areas where waste accumulation is a significant problem. For instance, in regions where waste collection infrastructure is underdeveloped or in disaster-stricken areas where waste management is urgently needed, a mobile pyrolysis plant can be deployed quickly and efficiently. This capability not only enhances the efficiency of waste management operations but also ensures that even the most challenging environments can benefit from advanced pyrolysis technology.

2. Cost-Effective Waste Management

Cost efficiency is another crucial advantage of mobile pyrolysis plants. By eliminating the need for extensive infrastructure and reducing transportation costs, mobile pyrolysis plants offer a more economical solution for waste management. The ability to process waste on-site means that there is no need to transport waste to a central processing facility, which can be particularly costly for remote or large-scale operations.

Moreover, mobile pyrolysis plants often require lower capital investment compared to their stationary counterparts. The modular design of these units allows for scalability, meaning that operators can start with a smaller investment and expand capacity as needed. This adaptability makes mobile pyrolysis plants an attractive option for small and medium-sized enterprises (SMEs) or municipalities with limited budgets.

The operational costs of a mobile pyrolysis plant are also generally lower, as these units are designed to be energy-efficient. Many mobile pyrolysis plants utilize energy recovery systems, which capture and reuse the heat generated during the pyrolysis process, further reducing fuel consumption and operational expenses. These cost-saving features contribute to the overall economic viability of mobile pyrolysis technology.

3. Improved Environmental Impact

The environmental benefits of mobile pyrolysis plants are multifaceted. Firstly, by processing waste on-site, these units reduce the need for long-distance waste transportation, which in turn lowers greenhouse gas emissions associated with fuel consumption. This localized approach to waste management helps to minimize the carbon footprint of waste processing operations.

Additionally, mobile pyrolysis plants contribute to waste minimization by converting various types of waste, including plastic, biomass, and tires, into valuable byproducts such as bio-oil, char, and syngas. These byproducts can be used as renewable energy sources or raw materials in other industrial processes, promoting a circular economy and reducing reliance on fossil fuels.

Mobile pyrolysis technology also addresses the issue of landfill overuse. By providing an alternative method for waste disposal, mobile pyrolysis plants help to divert waste from landfills, reducing the environmental hazards associated with landfill sites, such as leachate contamination and methane emissions. This reduction in landfill dependency is particularly beneficial in regions where landfill space is limited or where strict environmental regulations are in place.

4. Rapid Deployment and Operational Efficiency

The design of mobile pyrolysis oil plant allows for rapid deployment, making them ideal for situations where quick waste management solutions are required. Unlike stationary plants, which can take months or even years to construct and become operational, mobile pyrolysis units can be set up and commissioned within a short timeframe. This rapid deployment capability is especially valuable in emergency scenarios, such as natural disasters or industrial accidents, where immediate waste management is critical to prevent environmental damage.

Operational efficiency is another key advantage of mobile pyrolysis plants. These units are typically designed with automated controls and monitoring systems, allowing for streamlined operation with minimal human intervention. The automation of the pyrolysis process ensures consistent and high-quality output, reducing the likelihood of errors and increasing overall productivity.

Furthermore, the portability of mobile pyrolysis plants means that they can be relocated as needed to follow waste generation patterns. This adaptability ensures that the pyrolysis plant is always positioned where it is most needed, maximizing its utilization and effectiveness. For example, a mobile pyrolysis plant can be deployed to different construction sites, agricultural areas, or industrial zones, providing targeted waste management solutions without the need for multiple stationary facilities.

5. Versatility in Feedstock Processing

Mobile pyrolysis plants are highly versatile in terms of the types of feedstock they can process. These units are capable of handling a wide range of waste materials, including plastic, rubber, biomass, and municipal solid waste. This versatility makes mobile pyrolysis plants a valuable tool for waste management operations that deal with diverse waste streams.

The ability to process multiple types of feedstock not only increases the utility of mobile pyrolysis plants but also enhances their economic viability. Operators can switch between different types of waste depending on availability and market demand for pyrolysis products. For instance, when there is a high demand for biochar, the plant can focus on processing biomass. Alternatively, during periods when waste plastic accumulation is high, the plant can shift to plastic pyrolysis, producing valuable pyrolysis oil and reducing plastic waste.

The adaptability of mobile pyrolysis plants also means that they can be used in various industries and applications. From agriculture to industrial waste management, these units provide a flexible and effective solution for converting waste into valuable resources. This versatility is particularly advantageous in regions where waste composition varies seasonally or where different industries generate different types of waste.

Conclusion

Mobile pyrolysis plants offer a range of significant advantages that make them an increasingly popular choice for modern waste management. Their flexibility, cost-effectiveness, environmental benefits, rapid deployment, and versatility in feedstock processing make them well-suited for a variety of applications across different industries and regions. As global demand for sustainable waste management solutions continues to grow, mobile pyrolysis technology is poised to play a crucial role in reducing waste and promoting the circular economy.
By Cathy Wang • September 29, 2026
The performance of a plastic pyrolysis system is often evaluated by production capacity and energy efficiency. However, product quality remains equally important. In a commercial operation, the composition and consistency of pyrolysis oil, combustible gas, and solid residues determine the potential value of the final products and influence downstream applications. For investors exploring a plastic to oil machine for sale , understanding the factors that affect product quality is essential for making informed technical and economic decisions. Feedstock Composition Determines Product Characteristics Plastic feedstock is the primary variable influencing pyrolysis output. Different polymers exhibit distinct thermal decomposition pathways, resulting in variations in oil composition, gas yield, and solid residue formation. Polyolefin materials such as polyethylene (PE) and polypropylene (PP) generally produce higher liquid yields because their molecular structures favor hydrocarbon generation during pyrolysis. Polystyrene (PS) can generate aromatic compounds, while plastics containing chlorine, oxygen, or other heteroatoms may require additional process control due to the formation of undesirable by-products. Feedstock purity is equally important. Metal fragments, dirt, moisture, and non-target materials can alter thermal behavior and affect the consistency of products. A stable and well-prepared feedstock stream contributes to more predictable operation and product quality. Temperature Control Influences Product Distribution Pyrolysis is fundamentally a temperature-driven process. Reactor temperature affects the extent of polymer cracking and determines the relative proportion of liquid, gas, and solid products. Lower temperatures may lead to incomplete decomposition and higher residue content. Excessively high temperatures, by contrast, can promote secondary cracking reactions, converting condensable hydrocarbons into permanent gases. Maintaining a suitable temperature window allows the system to balance liquid production with gas generation. Temperature uniformity is equally significant. Thermal gradients within the reactor can create heterogeneous reaction zones, leading to fluctuations in product composition. Continuous monitoring and automated control systems help maintain stable operating conditions. Residence Time and Vapor Management The duration that plastic and pyrolysis vapors remain inside the reactor also affects final products. Longer residence times can increase secondary reactions, altering hydrocarbon distribution and reducing the proportion of heavier liquid fractions. Vapor handling systems therefore play an important role. Efficient condensation equipment enables the recovery of condensable hydrocarbons while separating non-condensable gas for energy utilization. The design of condensers, cooling systems, and gas pipelines influences heat transfer efficiency and can affect the composition of collected oil. Insufficient cooling may result in the loss of valuable hydrocarbons, while excessive cooling can increase operational complexity. Role of Non-Condensable Gas Non-condensable gas generated during pyrolysis contains combustible components that can contribute to process heating after suitable treatment. This internal energy circulation reduces dependence on external fuel sources and improves thermal efficiency. Gas composition depends on feedstock type, reactor temperature, and operating conditions. Hydrogen, methane, and light hydrocarbons may be present in varying proportions. Their effective utilization can improve overall energy management within the plant. For buyers comparing a plastic to oil machine for sale , the ability to recover and utilize process gas should be considered alongside reactor design and production capacity. Formation and Management of Solid Residues Solid residues represent the non-volatile fraction remaining after thermal decomposition. Their quantity and characteristics are affected by feedstock composition, operating temperature, and process stability. In plastic pyrolysis, residue may contain carbonaceous material, inorganic additives, pigments, fillers, and traces of contaminants. Excessive residue generation can indicate incomplete conversion or unsuitable feedstock preparation. Residue handling systems therefore form an important part of plant design. Efficient discharge and collection support continuous operation while reducing maintenance requirements. Integrating Quality Control into Plant Operation Product quality does not depend on a single parameter. It results from the interaction of feedstock preparation, temperature management, residence time, vapor recovery, and residue control. For companies evaluating a plastic to oil machine for sale , technical assessment should extend beyond nominal production capacity. Feedstock compatibility, thermal stability, condensation efficiency, gas utilization, and residue management all influence the consistency and value of final products. A well-designed pyrolysis system combines these elements into an integrated process. Stable operation, controlled reaction conditions, and effective product recovery can improve the quality of oil, gas, and solid residues while supporting more efficient resource utilization from plastic waste.
By Cathy Wang • September 29, 2026
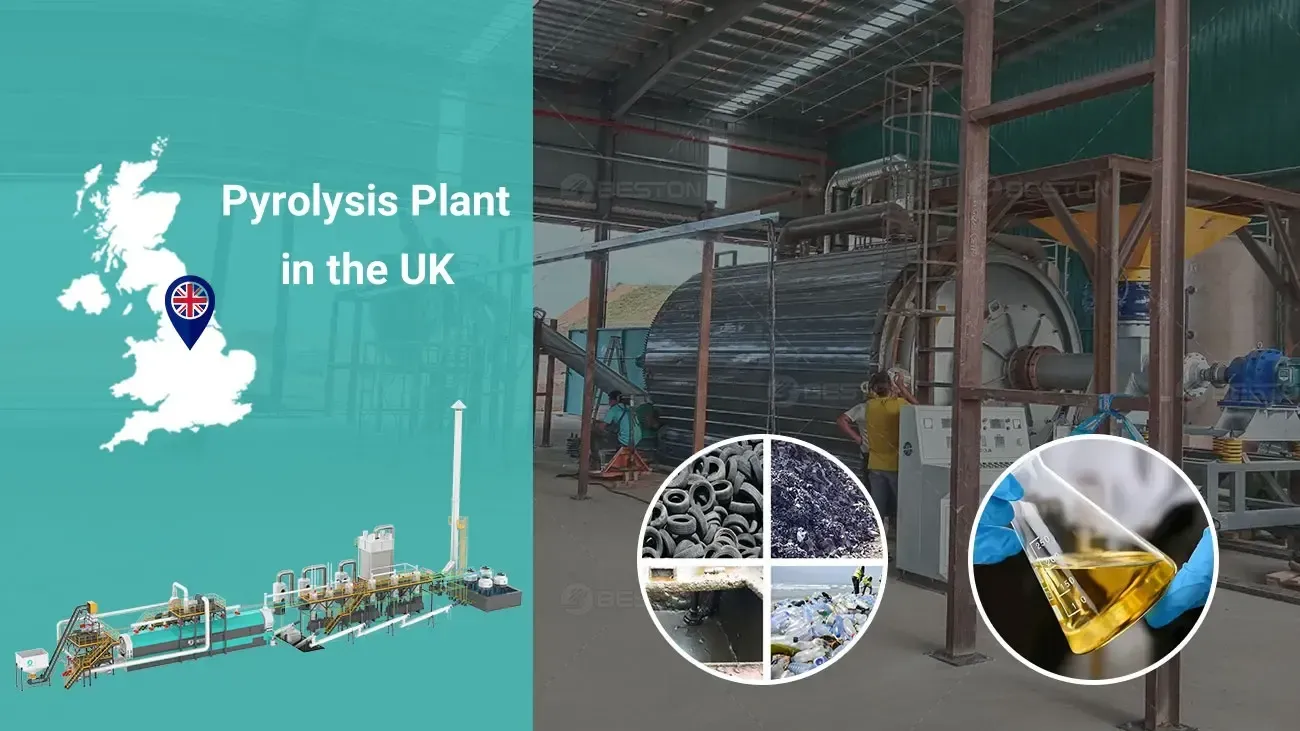
Every year, Britain's roads consume tens of millions of tyres. When they wear out, they become one of the country's most persistent waste streams: bulky, durable, and difficult to recycle. Industry estimates put UK end-of-life tyre (ELT) arisings at roughly 500,000 tonnes a year. With landfill closed to them, how that material is handled has become a defining question for the recycling sector. The Tyre Landfill Ban: What Changed The UK has not banned landfill in general. Many wastes can still be landfilled, subject to permits and Landfill Tax. Tyres, however, are a specifically restricted category. Whole tyres were banned from landfill in 2003, and shredded tyres followed in 2006. The reasoning was sound. Tyres trap gases, tend to work their way up through landfill layers, and consume valuable void space. Stockpiles are just as problematic: tyre fires are notoriously hard to extinguish and release harmful emissions. With landfill off the table, ELTs have followed three main routes: material recovery (crumb and granulate for surfacing and infrastructure), energy recovery (chiefly cement kilns and tyre-derived fuel), and export. Each has limits. Crumb markets are finite, energy recovery does little to keep materials in circulation, and exporting shifts environmental responsibility overseas at a time when regulators and customers are asking tougher questions about where waste ends up. Enter Pyrolysis Pyrolysis heats shredded tyres in an oxygen-free reactor, breaking them down thermally rather than burning them. The process yields three principal outputs: pyrolysis oil, recovered carbon black (rCB), and steel wire. It also produces a non-condensable syngas, which is typically recycled to heat the reactor. This is why interest in the pyrolysis plant UK operators can deploy is rising. Pyrolysis converts a low-value, hard-to-handle waste into several marketable products, and it can process feedstock that is unsuitable for mechanical recycling. Because the syngas can supply much of the process heat, well-designed plants can be reasonably energy self-sufficient once running. Where the Value Lies Carbon black. Recovered carbon black is arguably the most strategically important product. Tyre and rubber manufacturers face growing pressure to increase recycled content, and rCB offers a lower-carbon alternative to virgin carbon black made from fossil feedstocks. The challenge is consistency: buyers need tightly specified material, so post-processing and quality control are critical. Pyrolysis oil. The oil can be used as an industrial fuel or upgraded as a petrochemical feedstock. Access to premium markets depends on refining and on regulatory clarity about when the material stops being classed as waste. Steel. Recovered steel is easy to sell into established scrap markets and adds useful secondary revenue. Challenges Developers Must Address The opportunity is real, but so are the hurdles: Permitting. Thermal treatment facilities need environmental permits, and regulators scrutinise emissions controls, abatement systems, and monitoring closely. Early engagement with the environmental regulator and local planning authority is essential. Feedstock security. Reliable, contracted tyre supply at predictable cost underpins any business case. Relationships with collectors and processors matter as much as reactor design. Product specification. Offtake agreements for oil and carbon black should be pursued early, with clear quality standards. Community acceptance. Thermal technologies attract public scrutiny. Transparent communication about emissions, traffic, and safety builds trust. Technology choice. Batch, semi-continuous, and continuous systems differ significantly in throughput, maintenance demands, and capital cost. Independent due diligence on reference plants is well worth the investment. Policy Tailwinds Broader trends favour recycling routes that return materials to the economy. Resource-efficiency goals, continuing discussion of producer responsibility approaches for tyres, and industry commitments to recycled content all point toward growing demand for verified, traceable secondary materials. Tyre manufacturers and fleet operators increasingly want demonstrable end-of-life solutions, and pyrolysis can offer a credible story when supported by robust carbon accounting and certification. Looking Ahead The tyre landfill ban solved one problem and created another: what to do with half a million tonnes of durable, high-energy material each year. Pyrolysis offers a technically proven answer, but success depends on execution. That means disciplined feedstock sourcing, realistic financial modelling, high-quality outputs, and open engagement with regulators and communities. For investors, waste operators, and technology providers, the message is encouraging. As the UK tightens its approach to waste and raises its circular-economy ambitions, a well-run pyrolysis plant UK projects can build is well placed to turn a regulatory constraint into a durable commercial opportunity.
By Cathy Wang • September 23, 2026
Municipal and industrial wastewater treatment facilities generate large volumes of sludge as a by-product of purification processes. This material often contains organic matter, moisture, inorganic minerals, and trace contaminants, making disposal both technically challenging and economically significant. Traditional management methods, such as landfilling, incineration, and direct land application, are increasingly influenced by environmental regulations, transportation costs, and resource-recovery objectives. Against this background, sewage sludge pyrolysis has emerged as a thermochemical pathway that converts sludge into carbon-rich products while reducing waste volume. Characteristics of Sewage Sludge as a Feedstock Sewage sludge differs substantially from conventional biomass feedstocks. Moisture content is often high, and ash concentrations can vary depending on wastewater composition and treatment processes. In addition, sludge may contain nutrients, metals, inorganic compounds, and residual organic substances. These characteristics influence thermal behavior during pyrolysis. Feedstock preparation therefore becomes an important step. Mechanical dewatering, thermal drying, and particle-size homogenization can improve process stability and reduce unnecessary energy consumption. The selection of pretreatment methods depends on sludge properties, local infrastructure, and the intended application of the final carbon product. Thermal Conversion Through Sewage Sludge Pyrolysis Pyrolysis involves heating organic material under oxygen-limited conditions, allowing thermal decomposition to occur without complete combustion. During sewage sludge pyrolysis , complex organic compounds are transformed into three principal fractions: Carbon-rich solid products; Condensable liquids; Non-condensable gases. The distribution of these products depends on reactor temperature, heating rate, residence time, and feedstock composition. Compared with direct incineration, pyrolysis emphasizes resource recovery alongside waste reduction. Organic carbon is retained partially within the solid product, while combustible gases can contribute to process heating after appropriate treatment. The process also reduces sludge volume significantly, thereby lowering transportation and disposal requirements. Reactor and Equipment Considerations Sludge processing requires equipment designed to accommodate feedstocks with varying moisture levels, particle characteristics, and ash content. A sludge pyrolysis system generally includes: Feedstock pretreatment equipment; Drying units; Thermal conversion reactor; Condensation system; Gas-utilization section; Solid-product cooling system; Emission-control equipment. The reactor is the core component. Rotary kilns, screw reactors, and other indirectly heated systems are frequently used because they provide controlled material movement and stable heat transfer. Temperature management is essential. Excessive temperatures can reduce solid-product yield, while insufficient thermal input may result in incomplete conversion. Process automation and instrumentation help maintain stable operating conditions. Carbon Products and Resource Recovery One of the key outcomes of sewage sludge pyrolysis is the generation of carbon-containing solids. Depending on feedstock composition and processing conditions, these materials may contain fixed carbon, mineral matter, and nutrient elements. Potential applications vary according to product quality, local regulations, and technical requirements. In some contexts, carbon products may be considered for industrial applications, construction materials, or further upgrading processes. Comprehensive characterization is necessary before determining suitable end uses. The gaseous fraction also has value. After purification and controlled combustion, non-condensable gas can provide part of the thermal energy required for the pyrolysis process. This internal energy loop may improve overall thermal efficiency. Emission Control and Environmental Considerations Sludge treatment technologies must address emissions carefully. Pyrolysis systems therefore require integrated gas cleaning and environmental control measures. Dust removal, condensation, thermal oxidation, and exhaust-gas treatment may be incorporated depending on process design and regulatory requirements. Continuous monitoring of temperature, pressure, and emissions can further improve operational reliability. Attention should also be given to the management of inorganic residues and potential contaminants. Product testing remains essential to ensure that recovered materials meet applicable standards. From Waste Management to Carbon Resource Utilization The concept behind sewage sludge pyrolysis extends beyond disposal. Instead of treating sludge solely as a waste stream, pyrolysis views it as a source of carbon, energy, and potentially useful materials. A complete process chain—comprising dewatering, drying, thermal conversion, gas utilization, product cooling, and emission control—can transform complex sludge streams into more stable products while reducing waste volume. As wastewater treatment facilities seek more circular resource-management strategies, sludge pyrolysis machines provide a technological pathway that links waste reduction, energy recovery, and carbon-product generation within a single thermochemical system.