Upgrading Recovered Carbon Black: From Raw Char to High-Value Industrial Filler
Recovered carbon black (rCB) is emerging as a valuable material in the tire recycling industry. Produced during waste tire pyrolysis, raw carbon black contains carbonaceous residues, inorganic ash, residual oils, and sulfur-containing compounds. In its untreated form, this material often has inconsistent quality and limited applications, resulting in a lower market value than virgin commercial carbon black. However, through grinding, classification, pelletizing, and appropriate purification or surface modification, recovered carbon black can be upgraded into a more consistent industrial filler for rubber and plastic products.
1. Why Raw Carbon Black Has Limited Market Value
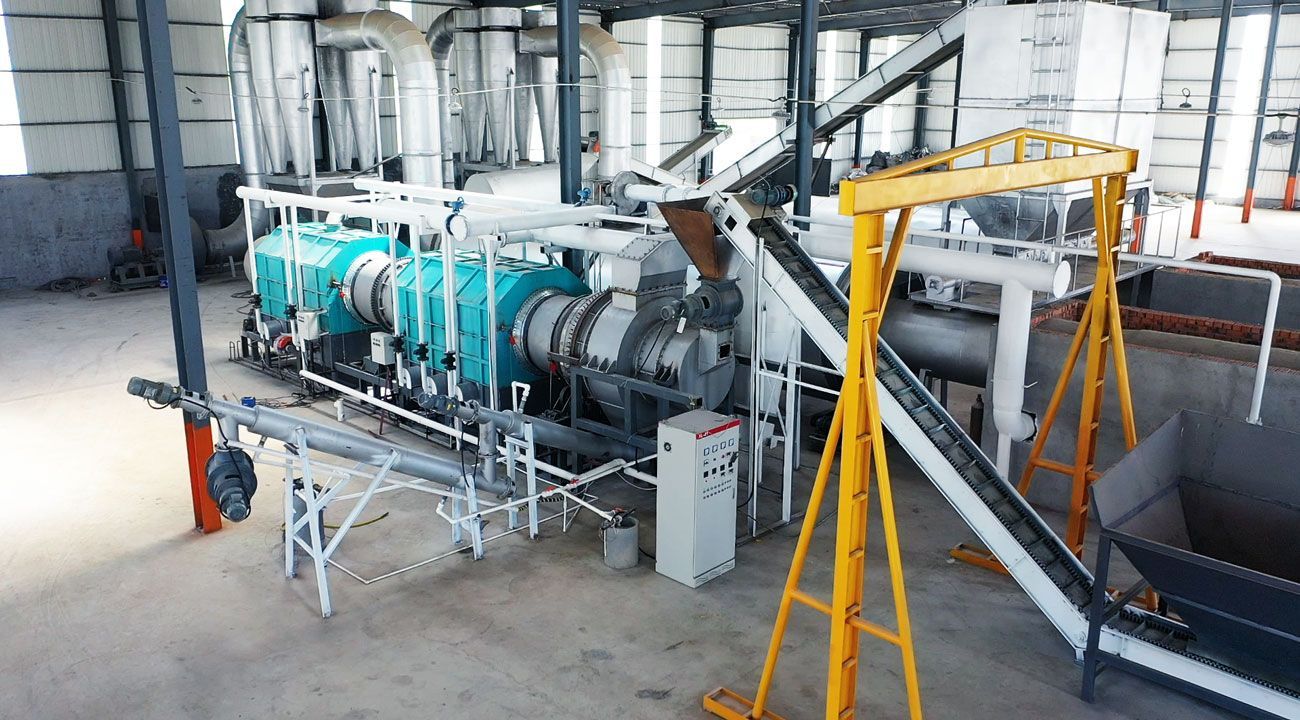
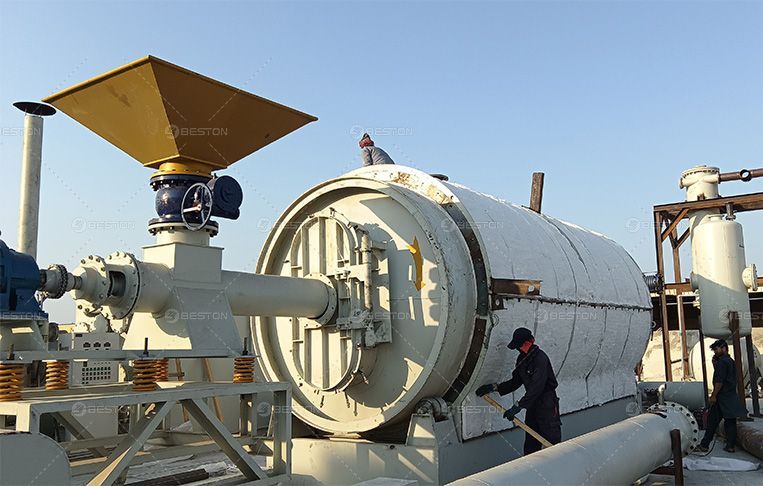
During waste tire pyrolysis plant, rubber polymers decompose under oxygen-limited conditions, producing pyrolysis oil, non-condensable gas, steel wire, and a solid carbon-rich residue. This solid residue is commonly called raw pyrolysis char.
Unlike virgin carbon black, which is manufactured under controlled conditions to achieve specific particle characteristics, raw pyrolysis char retains some of the original tire components. Its properties depend on the tire composition, pyrolysis temperature, residence time, and reactor design.
Several factors limit its direct use in industrial manufacturing:
- High ash content: Silica, zinc compounds, and other inorganic residues from tire additives can reduce the proportion of usable carbon.
- Residual oil and volatile matter: Incomplete removal of organic compounds can affect processing behavior and product consistency.
- Sulfur-containing compounds: Sulfur originating from tire vulcanization may remain in the recovered material and influence certain applications.
- Uneven particle size: Agglomerated particles and coarse residues can cause dispersion problems in rubber compounds.
- Variable reinforcing performance: Surface chemistry, aggregate structure, and particle characteristics may differ substantially from those of virgin carbon black.
These limitations explain why raw carbon black generally sells at a discount. To unlock its commercial potential, producers must focus on improving material quality rather than simply increasing the amount of char recovered from each ton of waste tires.
2. Grinding and Classification Improve Material Consistency
Grinding is one of the first steps in upgrading raw pyrolysis char. The objective is to reduce oversized particles, break down agglomerates, and produce a more uniform powder suitable for downstream processing.
Industrial milling systems can include impact mills, pin mills, or other grinding equipment selected according to the characteristics of the feed material. Classification equipment separates particles according to size, helping manufacturers maintain consistent product specifications.
However, finer grinding does not automatically produce better reinforcing performance. Carbon black's behavior in rubber also depends on aggregate structure, surface area, surface chemistry, and dispersion. Excessive grinding can increase energy consumption without delivering a proportional improvement in final product performance.
Magnetic separation and screening may also be necessary to remove residual steel fragments and coarse contaminants before milling.
For commercial production, particle size distribution should be monitored alongside ash content, moisture, and other relevant properties. These measurements help establish repeatable product quality and reduce the risk of inconsistent performance during compounding.
3. Pelletizing Improves Handling and Transportation
Fine recovered carbon black powder can create dust during conveying, storage, and feeding. It may also have poor flowability, making accurate dosing more difficult in industrial production lines.
Pelletizing addresses these handling problems by compressing or agglomerating the powder into small granules. Depending on the formulation and intended application, the process may use water, binders, or other processing aids.
The main benefits include:
- Reduced dust generation during handling.
- Improved flowability and feeding consistency.
- Easier storage, packaging, and transportation.
- More convenient integration into automated rubber and plastic compounding systems.
Pellet quality is important. Pellets that are too hard may disperse poorly during mixing, while those with insufficient strength may break apart and generate dust. Binder selection and dosage must also be controlled because they can affect moisture content, mixing behavior, and the properties of the finished compound.
Pelletizing primarily improves handling characteristics. It does not independently remove ash, reduce sulfur content, or guarantee that recovered carbon black meets a particular industrial grade.
4. Purification and Modification Increase Commercial Value
After physical processing, additional treatments may be required to improve the chemical and functional properties of recovered carbon black.
De-oiling and volatile matter removal
Residual organic compounds can be reduced through suitable thermal treatment, extraction, or other purification processes. The appropriate method depends on the initial char composition and the target product specifications.
Better control of volatile matter can improve product consistency, although treatment conditions must be carefully selected to avoid unnecessary energy consumption or changes to desirable carbon characteristics.
Ash reduction and desulfurization
Ash reduction can involve chemical treatment, washing, or other separation methods. Desulfurization may use thermal, chemical, or combined processes, depending on the sulfur compounds present.
These treatments can improve the suitability of recovered carbon black for selected applications, but they also introduce additional costs and potential environmental challenges. Chemical treatment may generate wastewater or secondary residues that require appropriate management.
Producers should evaluate the improvement in product performance against the costs of reagents, energy, wastewater treatment, and material losses.
Surface modification
Surface treatment can alter the interactions between recovered carbon black and the surrounding polymer matrix. Depending on the treatment, it may improve compatibility, dispersion, or selected mechanical properties.
The best modification strategy should be determined through laboratory testing and application-specific trials rather than assumed to work equally well for every recovered carbon black product.
5. Can Recovered Carbon Black Replace N330 or N660?
Recovered carbon black can replace part of the virgin carbon black used in certain rubber compounds, but substitution depends on the application and the quality of the recovered material.
N330 is commonly used in tire treads and other applications requiring relatively strong reinforcement. N660 is generally associated with lower reinforcement and lower hysteresis requirements than N330 in many rubber formulations.
These grades have defined performance characteristics. Matching their particle size alone is insufficient because reinforcing behavior also depends on surface area, structure, surface chemistry, and dispersion.
A practical evaluation should consider:
- Iodine adsorption or other surface-area indicators.
- Oil absorption or structure-related measurements.
- Ash, sulfur, moisture, and volatile matter.
- Particle size distribution and dispersion quality.
- Tensile strength, elongation, hardness, abrasion resistance, and other application-specific properties of the finished compound.
Rather than claiming that all recovered carbon black can directly replace N330 or N660, manufacturers should establish substitution ratios through controlled trials. In some formulations, rCB may partially replace virgin carbon black while maintaining acceptable performance. Other demanding applications may require additional purification, modification, or blending with virgin grades.
6. Applications in Rubber and Plastic Manufacturing
The commercial opportunities for upgraded recovered carbon black extend beyond tire recycling.
In rubber products, potential applications include conveyor belts, rubber mats, hoses, molded components, and selected automotive rubber parts. The appropriate use depends on mechanical requirements, product safety standards, and the consistency of the recovered material.
In plastics, recovered carbon black may be incorporated into selected masterbatches and polymer compounds where its color, dispersion, contamination level, and processing behavior meet customer specifications. Testing is especially important for products requiring consistent appearance, electrical performance, or stringent mechanical properties.
Market entry generally begins with less demanding applications before progressing toward products requiring higher reinforcement and tighter quality control.
Conclusion
Recovered carbon black offers tire pyrolysis operators an opportunity to move beyond selling low-value raw char. Grinding and classification improve physical consistency, pelletizing facilitates handling, and targeted purification or surface modification can expand the range of potential applications.
The key to commercial success is not simply producing more recovered carbon black, but developing a consistent material that meets measurable customer requirements. By combining appropriate post-processing equipment, quality control, and application-specific testing, producers can improve product value, reduce dependence on virgin raw materials, and strengthen the economics of waste tire pyrolysis.