Application Scenarios of Wood Pyrolysis Plant
Cathy Wang • August 8, 2024

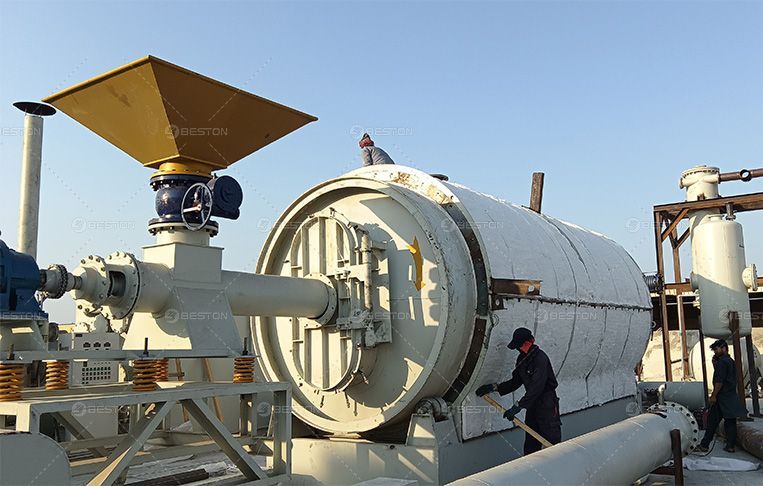
Wood pyrolysis plants represent a critical innovation in the sustainable management of wood waste and biomass. These plants utilize pyrolysis technology to convert wood and other organic materials into valuable byproducts, including bio-oil, syngas, and biochar. The diverse applications of wood pyrolysis plants illustrate their potential to contribute significantly to resource efficiency, waste management, and energy production.

Overview of Wood Pyrolysis Technology

Wood pyrolysis is a thermal decomposition process conducted in the absence of oxygen, where wood is heated to high temperatures. This process breaks down complex organic molecules into simpler compounds. The primary products of wood pyrolysis include:

  • Bio-oil: A liquid product that can be refined into various fuels and chemicals.
  • Syngas: A gaseous mixture mainly comprising hydrogen, carbon monoxide, and carbon dioxide, useful for energy generation.
  • Biochar: A solid, carbon-rich material that can be used as a soil amendment or in industrial applications.

The efficiency and output of a wood pyrolysis plant depend on factors such as feedstock type, pyrolysis conditions, and the technology employed.

Application Scenarios

1. Biomass Waste Management

Wood pyrolysis plants play a crucial role in managing biomass waste, which includes wood chips, sawdust, and forestry residues. Traditionally, such waste might be burned or left to decay, leading to environmental concerns such as air pollution and methane emissions. Pyrolysis provides a sustainable alternative by converting this waste into valuable products while minimizing harmful emissions. The biochar produced can be used to enrich soil, reducing the need for synthetic fertilizers and improving soil health.

2. Energy Production

Energy generation is a prominent application of wood pyrolysis technology. The syngas generated during pyrolysis can be utilized as a renewable energy source. It can be combusted to produce electricity or heat, contributing to energy diversification and reducing reliance on fossil fuels. Additionally, bio-oil can be further processed to produce biofuels, offering a sustainable alternative to petroleum-based fuels. Wood pyrolysis plants can thus support energy security and contribute to cleaner energy solutions.

3. Soil Enhancement

Biochar, one of the byproducts of wood pyrolysis, is increasingly recognized for its benefits in soil enhancement. When added to agricultural soils, biochar improves soil structure, increases water and nutrient retention, and promotes microbial activity. This can lead to enhanced crop yields and reduced need for chemical fertilizers. By utilizing wood pyrolysis plants to produce biochar, agricultural practices can become more sustainable, contributing to soil health and agricultural productivity.

4. Carbon Sequestration

The carbon sequestration potential of wood pyrolysis is significant. By converting wood into biochar, carbon that would otherwise be released into the atmosphere as CO2 is effectively stored in a stable form. This contributes to climate change mitigation efforts by reducing greenhouse gas concentrations. Wood pyrolysis plants thus offer a dual benefit: managing wood waste and sequestering carbon, aligning with global climate goals.

5. Industrial Applications

Wood pyrolysis products have several industrial applications beyond energy and soil improvement. Bio-oil can be refined and used as a feedstock for producing chemicals and materials, such as phenols, acids, and resins. Biochar can be utilized in various industrial processes, including metal production and water treatment. The versatility of wood pyrolysis products enhances their utility in diverse industrial sectors, contributing to resource efficiency and sustainability.

6. Waste Reduction and Recycling

The efficient processing of wood waste through pyrolysis supports waste reduction and recycling efforts. Wood pyrolysis plants convert waste materials into valuable products, reducing the volume of waste that needs to be managed through traditional methods. This contributes to a circular economy approach by turning waste into resources, minimizing landfill use, and promoting sustainable waste management practices.

7. Rural Development

In rural areas, wood pyrolysis plants can stimulate economic development by creating local jobs and providing a source of income for communities involved in wood waste collection and processing. The establishment of pyrolysis facilities can also support local industries by supplying biochar and bio-oil for various applications. This local economic activity fosters sustainable development and enhances the resilience of rural economies.

8. Disaster Recovery

In the aftermath of natural disasters, such as wildfires or hurricanes, large quantities of wood waste may accumulate. Wood pyrolysis plants offer a solution for processing this waste efficiently. By converting disaster debris into charcoal made from wood and other products, these plants can aid in recovery efforts and reduce the environmental impact of waste. This application underscores the role of pyrolysis technology in addressing emergency situations and supporting recovery processes.

Technological Considerations

1. Feedstock Variety

Wood pyrolysis plants can process various types of feedstock, including wood chips, sawdust, and agricultural residues. The choice of feedstock influences the characteristics and yield of the pyrolysis products. Effective feedstock management and preparation are essential for optimizing plant performance and product quality.

2. Process Optimization

The efficiency of a wood pyrolysis plant depends on the optimization of process parameters such as temperature, pressure, and residence time. Advanced pyrolysis systems incorporate precise control mechanisms to ensure optimal conditions for producing high-quality bio-oil, syngas, and biochar. Continuous monitoring and adjustment of these parameters are crucial for maximizing output and minimizing byproduct formation.

3. Environmental Compliance

Wood pyrolysis plants must adhere to environmental regulations to ensure that emissions and byproducts are managed responsibly. The integration of emissions control systems, such as gas cleaning and filtration, is essential for reducing the environmental impact of pyrolysis operations. Compliance with regulatory standards helps maintain the sustainability and acceptability of wood pyrolysis technology.

Conclusion

Wood pyrolysis plants offer a range of applications that contribute to sustainable waste management, energy production, soil enhancement, and industrial resource utilization. By converting wood and biomass into valuable byproducts, these plants support environmental protection, economic development, and resource efficiency. The diverse application scenarios of wood pyrolysis technology highlight its potential to address various challenges and promote sustainable practices across multiple sectors. As technology advances and awareness grows, the role of wood pyrolysis plants in achieving sustainability goals is likely to expand, fostering a more resource-efficient and environmentally friendly future.
By Cathy Wang • November 17, 2026
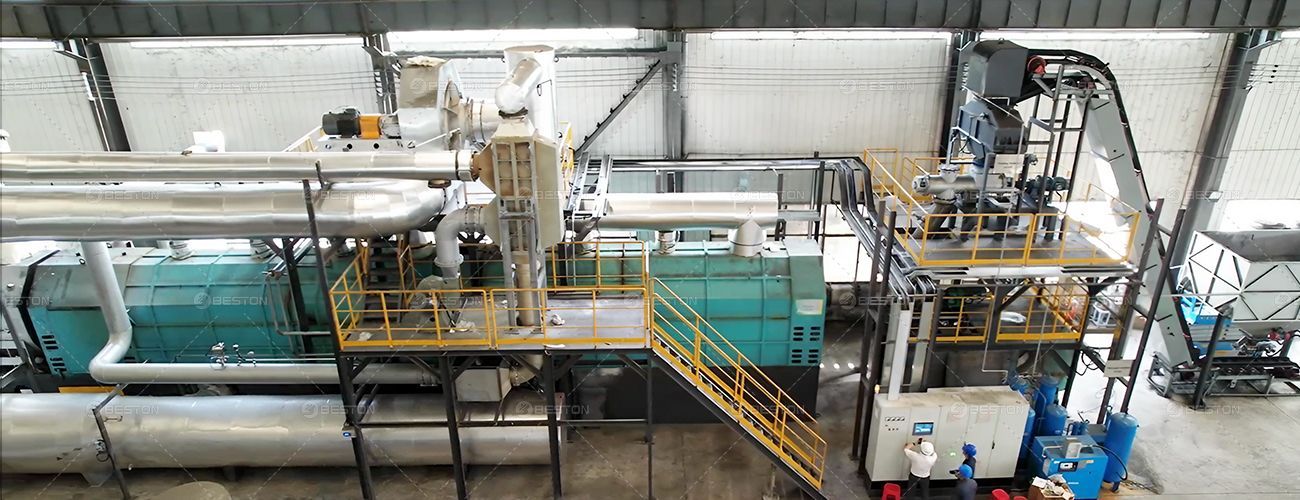
Continuous pyrolysis technology enables the sustained thermal conversion of waste materials into recoverable resources, including pyrolysis oil, combustible gas, and solid residues. Compared with batch processing, continuous operation places greater emphasis on coordinated material feeding, temperature regulation, vapor recovery, and residue discharge. Maintaining stable operating conditions is essential for achieving consistent product quality, maximizing equipment utilization, and controlling production costs. A fully continuous pyrolysis plant therefore requires integrated process management rather than isolated control of individual equipment components. 1. Feedstock Preparation and Continuous Feeding Feedstock consistency is the foundation of stable pyrolysis operation in a fully continuous pyrolysis plant . Variations in moisture content, particle size, composition, and contamination levels can affect heat transfer, material movement, and thermal decomposition efficiency. Before entering the reactor, raw materials should undergo appropriate pretreatment. Depending on the feedstock, this may involve sorting, crushing, screening, and drying. For waste plastic processing, removing unsuitable materials such as PVC and PET helps reduce undesirable chemical compounds and downstream treatment requirements. The feeding system must also maintain a relatively consistent material supply. Fluctuating feed rates can disturb reactor temperature and residence time, resulting in uneven decomposition. Automated screw conveyors, sealed feeding devices, and coordinated material transfer mechanisms help maintain stable throughput while limiting air ingress. 2. Temperature Regulation and Thermal Stability Temperature control is one of the most important aspects of continuous pyrolysis operation. Thermal decomposition involves complex chemical reactions, and different feedstocks require specific temperature conditions to achieve the desired product distribution. Insufficient heating may cause incomplete decomposition, excessive wax formation, or residual unconverted material. Conversely, excessively high temperatures can promote secondary cracking, increasing non-condensable gas production and reducing liquid recovery. Industrial systems typically integrate multiple temperature monitoring points along the reactor. Automated control systems adjust heating intensity according to operating conditions, helping minimize thermal fluctuations. Heat distribution also deserves attention. Uneven heating can create localized temperature differences, affecting conversion efficiency and product consistency. Appropriate reactor configuration, material movement, and heat transfer arrangements help maintain a more uniform thermal environment. 3. Vapor Recovery and Byproduct Management During pyrolysis, decomposed hydrocarbons leave the reactor as vapor and enter the condensation system. Efficient vapor transfer and cooling are essential for maximizing liquid recovery. A properly configured condensation system separates recoverable liquid fractions from non-condensable gases. Multiple cooling stages can improve condensation performance across different hydrocarbon boiling ranges. Pipeline temperature management is particularly important when processing plastic waste. Heavy hydrocarbon vapors may condense prematurely and form wax deposits, potentially restricting vapor flow. Suitable insulation, temperature monitoring, and pipeline configuration help mitigate this problem. Non-condensable gases can also be collected and reused as supplementary heating fuel. This energy-recovery arrangement reduces dependence on external fuel and improves overall thermal utilization. Solid residues require equally systematic management. Continuous discharge and controlled cooling prevent material accumulation and help maintain uninterrupted reactor operation. 4. Automated Monitoring and Production Management A fully continuous pyrolysis plant relies on coordinated control across feeding, heating, condensation, and discharge systems. Automated monitoring improves operational visibility and helps operators identify deviations before they develop into production interruptions. Important monitoring parameters include: Reactor temperature: Maintains the required thermal conditions. System pressure: Helps identify abnormal pressure fluctuations and potential blockages. Feeding rate: Ensures consistent material input. Vapor temperature: Supports effective transfer and condensation. Discharge conditions: Prevents residue accumulation and operational instability. Centralized control systems can integrate these parameters into a unified operating interface. Historical operating data also help identify recurring inefficiencies and support preventive maintenance planning. However, automation does not eliminate the need for trained operators. Regular inspection and appropriate operating procedures remain essential for safe and reliable production. 5. Preventive Maintenance and Long-Term Reliability Continuous operation places sustained mechanical and thermal demands on reactors, conveyors, pipelines, pumps, and sealing components. Wear, corrosion, carbon deposits, and thermal fatigue can gradually affect equipment performance. Preventive maintenance should focus on critical components and potential failure points. Regular inspection of feeding mechanisms, reactor seals, condensation equipment, and gas pipelines helps identify deterioration before unexpected shutdowns occur. Maintenance schedules should also account for feedstock characteristics. Materials with higher impurity levels or greater ash content may require more frequent cleaning and inspection. Conclusion Stable continuous pyrolysis operation depends on the coordination of feedstock preparation, thermal regulation, vapor recovery, automated monitoring, and preventive maintenance. Consistent material input and controlled reactor conditions help maintain product quality, while effective energy recovery and residue management improve operational efficiency. Integrating these elements into a unified production management system provides a foundation for reliable long-term operation and more predictable industrial output.
By Cathy Wang • November 9, 2026
Investing in biochar production equipment requires more than evaluating the initial purchase price. The total project expenditure includes equipment procurement, installation, infrastructure preparation, energy consumption, labor, maintenance, and feedstock handling. These costs vary according to production capacity, biomass characteristics, pyrolysis technology, and operating schedules. A comprehensive cost analysis should therefore consider both capital expenditure (CAPEX) and operating expenditure (OPEX) to determine the economic feasibility of a biochar production project over its service life. 1. Initial Equipment Investment and Procurement Costs Equipment procurement typically represents a substantial proportion of the initial project investment. However, the purchase price of a biochar machine depends on several technical and commercial factors rather than production capacity alone. Key cost determinants include: Processing capacity: Larger systems generally require higher equipment investment because of increased reactor dimensions, feeding capacity, and auxiliary configurations. Reactor design: Rotary reactors, screw reactors, and other pyrolysis configurations differ in manufacturing complexity, thermal efficiency, and material requirements. Automation level: Automated feeding, temperature regulation, discharge, and monitoring systems may increase initial expenditure while reducing certain labor requirements. Emission treatment: Gas purification, dust collection, and exhaust treatment equipment contribute to procurement costs but are important for environmental management. Material specifications: Reactor steel grade, insulation materials, and high-temperature components influence manufacturing costs and expected service life. A bamboo charcoal machine , for example, may share certain thermal conversion principles with a biochar production system, but its configuration and operating parameters should reflect the characteristics of bamboo feedstock and the intended carbon product. Equipment specifications should therefore be evaluated against actual production requirements.  2. Installation and Supporting Infrastructure Equipment procurement is only one component of project investment. Installation and infrastructure preparation can significantly affect the overall capital budget. Site preparation may involve foundation construction, workshop development, electrical connections, water supply, and feedstock storage facilities. Additional expenses may arise from transportation, lifting equipment, mechanical assembly, and commissioning. Other infrastructure considerations include: Raw material storage and pretreatment areas. Biomass drying and size-reduction equipment. Fuel supply and electrical distribution systems. Finished biochar cooling, screening, and packaging facilities. Fire protection and environmental management installations. The availability of existing infrastructure can substantially reduce project expenditure. Conversely, remote installations or sites requiring extensive civil engineering may experience higher initial costs. 3. Energy Consumption and Feedstock Expenses Operating expenditure is influenced heavily by energy requirements and biomass procurement. Energy consumption depends on reactor configuration, feedstock moisture, operating temperature, insulation performance, and heat recovery efficiency. Wet biomass requires additional thermal energy for moisture evaporation before effective carbonization can proceed. Consequently, appropriate drying and feedstock preparation can help reduce unnecessary energy consumption. Some pyrolysis systems recover combustible gases generated during carbonization and reuse them as process fuel. This arrangement can reduce dependence on external energy sources after the system reaches stable operating conditions. Feedstock expenses also require careful assessment. Agricultural residues, forestry by-products, bamboo waste, and wood processing residues may have different procurement costs depending on local availability, transportation distance, and seasonal supply. For accurate budgeting, manufacturers should calculate feedstock consumption based on actual moisture content, bulk density, and expected biochar yield rather than relying exclusively on theoretical production figures. 4. Labor, Maintenance, and Replacement Costs Labor expenses depend on automation level, production capacity, and operational organization. Automated feeding and discharge systems can reduce manual handling requirements, although operators and maintenance personnel remain necessary for equipment supervision, inspection, and troubleshooting. Maintenance expenditure should also be incorporated into long-term financial planning. Typical maintenance activities include: Inspecting reactor shells, welds, and rotating assemblies. Replacing worn bearings, seals, and transmission components. Maintaining burners, pipelines, and gas treatment equipment. Cleaning material accumulation from feeding and discharge systems. Checking temperature sensors and electrical control components. High-temperature operation gradually affects refractory linings, insulation, and mechanical components. Establishing preventive maintenance schedules helps reduce unexpected equipment failures and associated production losses. 5. Evaluating Long-Term Operating Economics A reliable biochar machine cost analysis should distinguish between fixed and variable operating expenses. Several financial indicators can support investment decisions: Operating cost per ton: Total operating expenditure divided by annual biochar output. Capital cost per unit of capacity: Initial equipment investment relative to designed processing capacity. Payback period: The estimated time required for project cash flow to recover the initial investment. Equipment utilization rate: The proportion of available operating time during which the system produces biochar. These indicators should be calculated using realistic operating hours, production yields, and local energy prices. 6. Improving Investment Efficiency Through Equipment Selection Reducing the initial purchase price does not necessarily produce the lowest lifetime operating cost. Equipment reliability, thermal efficiency, automation, and maintenance accessibility can have a greater influence on long-term expenditure. A suitable selection process should consider feedstock availability, target production volume, site conditions, product specifications, and environmental requirements. Comparing equipment configurations against these parameters helps prevent overinvestment or insufficient processing capacity. Conclusion Biochar production economics depend on the interaction between initial equipment investment and recurring operating expenses. Procurement, installation, energy consumption, feedstock preparation, labor, and maintenance all contribute to total project costs. A comprehensive financial assessment should therefore extend beyond the equipment quotation and examine expected expenditure throughout the system's operating life. Selecting appropriately configured equipment and maintaining stable production conditions can improve resource utilization, control operating costs, and strengthen the long-term economic viability of biochar manufacturing.
By Cathy Wang • October 29, 2026
Installing a pyrolysis plant involves more than positioning the reactor and connecting auxiliary equipment. Successful commissioning requires coordinated mechanical assembly, utility integration, instrumentation verification, safety inspections, and performance testing. Each stage establishes the conditions for reliable operation and helps identify installation defects before commercial production begins. For a Beston pyrolysis plant , the installation plan should reflect the equipment configuration, feedstock characteristics, site infrastructure, and applicable local regulations. Equipment Assembly and Site Preparation Installation begins with a site-readiness assessment. The foundation must meet the equipment supplier's requirements for load-bearing capacity, levelness, anchoring, and vibration control. Access roads, unloading areas, lifting equipment, and maintenance clearances should also be confirmed before delivery. Once the equipment arrives, components are inspected against the packing list and technical documentation. Transport damage, missing parts, and deviations from approved drawings should be recorded and resolved before assembly proceeds. Mechanical installation typically covers the following systems: Main reactor: Positioning, alignment, anchoring, and verification of the drive or rotation mechanism where applicable. Feeding and discharge equipment: Installation of conveyors, feeders, sealing devices, and residue-handling components. Condensation system: Assembly of condensers, separators, pipelines, and associated cooling equipment. Gas handling: Connection of non-condensable gas lines, combustion equipment, and required treatment systems. Storage facilities: Installation of appropriate tanks, transfer lines, valves, and containment provisions for liquid products. Flange connections, seals, supports, and expansion allowances require particular attention. Thermal expansion can impose substantial mechanical stress during operation, especially where hot pipelines connect to relatively cool equipment. Assembly should follow approved engineering drawings rather than relying on visual alignment alone. Electrical Integration and Instrumentation Electrical and control-system installation establishes the link between mechanical equipment and process supervision. Motors, control cabinets, sensors, actuators, and protective devices must be connected and verified according to the electrical drawings and equipment specifications. Temperature sensors should be checked for correct placement, signal transmission, and calibration status. Pressure instruments, level indicators, flow meters, and gas detectors should undergo appropriate functional tests where installed. The programmable logic controller (PLC) and human-machine interface (HMI) should be checked for correct input and output mapping, alarm behavior, interlock logic, and operating sequences. Emergency stops and other protective functions require documented verification. These checks are essential. An instrument may display a plausible reading while transmitting an incorrect signal or responding too slowly. Functional verification helps identify such discrepancies before hot commissioning. Cold Commissioning and System Verification Cold commissioning tests equipment without introducing the full thermal load or conducting normal feedstock processing. Its purpose is to confirm mechanical readiness and verify that individual systems operate as intended. Typical activities include: Checking motor rotation, drive alignment, and conveyor movement. Verifying valve positions, pipeline connections, and cooling-water circulation. Testing control sequences, alarms, and emergency shutdown functions. Inspecting electrical protection and confirming instrument responses. Checking accessible joints and connections for leakage using approved methods. The commissioning team should record test results, unresolved defects, corrective actions, and approval status. Outstanding deficiencies affecting safety or equipment integrity must be addressed before the plant proceeds to hot commissioning. Hot Commissioning and Performance Testing Hot commissioning introduces thermal energy and establishes operating conditions under controlled procedures. Startup should follow the supplier's sequence for heating, gas handling, pressure management, and process stabilization. Once operating temperatures are established, suitable feedstock can be introduced according to the approved commissioning plan. Operators monitor temperature trends, pressure where applicable, gas flow, condensation performance, and discharge behavior. Abnormal fluctuations should be investigated rather than compensated for through arbitrary parameter changes. Performance testing then evaluates whether the plant meets agreed acceptance criteria. Relevant indicators may include: Feedstock throughput over a defined operating period. Liquid, gas, and solid product distribution. Specific fuel or energy consumption. Temperature stability and process continuity. Condensation performance and emissions-related measurements. Reliability of feeding, discharge, and auxiliary systems. Testing conditions must be documented, including feedstock composition, moisture content, operating hours, and measurement methods. These variables can materially affect results. Product yields should not be compared directly when feedstock properties or test conditions differ substantially. Documentation, Training, and Operational Handover Commissioning concludes with a structured handover. Essential records include approved drawings, equipment manuals, electrical schematics, calibration certificates, inspection reports, performance-test results, and maintenance schedules. Operators should receive practical training in startup, shutdown, routine inspection, alarm response, and emergency procedures. Spare-parts inventories and maintenance responsibilities should also be established before normal operation begins. A properly installed Beston pyrolysis plant depends on disciplined execution at every stage, from foundation preparation to performance verification. Systematic commissioning reduces avoidable startup problems, establishes a documented operating baseline, and provides evidence that the installed equipment performs according to the agreed technical requirements.