NEWS
The Best Luxury Real Estate in Southern California
NEWS
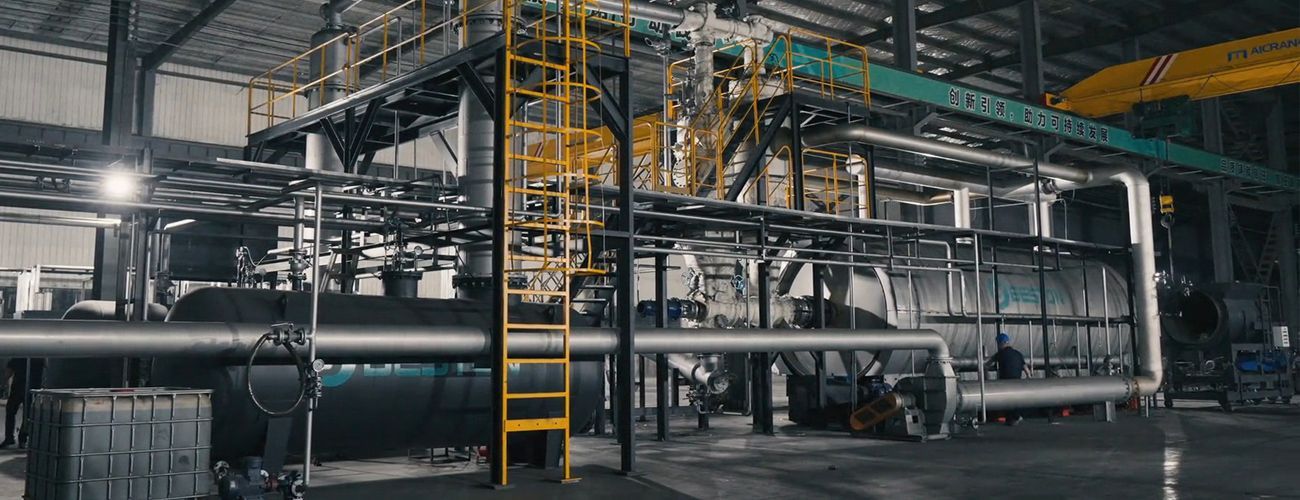
The performance of a plastic pyrolysis system is often evaluated by production capacity and energy efficiency. However, product quality remains equally important. In a commercial operation, the composition and consistency of pyrolysis oil, combustible gas, and solid residues determine the potential value of the final products and influence downstream applications. For investors exploring a plastic to oil machine for sale , understanding the factors that affect product quality is essential for making informed technical and economic decisions. Feedstock Composition Determines Product Characteristics Plastic feedstock is the primary variable influencing pyrolysis output. Different polymers exhibit distinct thermal decomposition pathways, resulting in variations in oil composition, gas yield, and solid residue formation. Polyolefin materials such as polyethylene (PE) and polypropylene (PP) generally produce higher liquid yields because their molecular structures favor hydrocarbon generation during pyrolysis. Polystyrene (PS) can generate aromatic compounds, while plastics containing chlorine, oxygen, or other heteroatoms may require additional process control due to the formation of undesirable by-products. Feedstock purity is equally important. Metal fragments, dirt, moisture, and non-target materials can alter thermal behavior and affect the consistency of products. A stable and well-prepared feedstock stream contributes to more predictable operation and product quality. Temperature Control Influences Product Distribution Pyrolysis is fundamentally a temperature-driven process. Reactor temperature affects the extent of polymer cracking and determines the relative proportion of liquid, gas, and solid products. Lower temperatures may lead to incomplete decomposition and higher residue content. Excessively high temperatures, by contrast, can promote secondary cracking reactions, converting condensable hydrocarbons into permanent gases. Maintaining a suitable temperature window allows the system to balance liquid production with gas generation. Temperature uniformity is equally significant. Thermal gradients within the reactor can create heterogeneous reaction zones, leading to fluctuations in product composition. Continuous monitoring and automated control systems help maintain stable operating conditions. Residence Time and Vapor Management The duration that plastic and pyrolysis vapors remain inside the reactor also affects final products. Longer residence times can increase secondary reactions, altering hydrocarbon distribution and reducing the proportion of heavier liquid fractions. Vapor handling systems therefore play an important role. Efficient condensation equipment enables the recovery of condensable hydrocarbons while separating non-condensable gas for energy utilization. The design of condensers, cooling systems, and gas pipelines influences heat transfer efficiency and can affect the composition of collected oil. Insufficient cooling may result in the loss of valuable hydrocarbons, while excessive cooling can increase operational complexity. Role of Non-Condensable Gas Non-condensable gas generated during pyrolysis contains combustible components that can contribute to process heating after suitable treatment. This internal energy circulation reduces dependence on external fuel sources and improves thermal efficiency. Gas composition depends on feedstock type, reactor temperature, and operating conditions. Hydrogen, methane, and light hydrocarbons may be present in varying proportions. Their effective utilization can improve overall energy management within the plant. For buyers comparing a plastic to oil machine for sale , the ability to recover and utilize process gas should be considered alongside reactor design and production capacity. Formation and Management of Solid Residues Solid residues represent the non-volatile fraction remaining after thermal decomposition. Their quantity and characteristics are affected by feedstock composition, operating temperature, and process stability. In plastic pyrolysis, residue may contain carbonaceous material, inorganic additives, pigments, fillers, and traces of contaminants. Excessive residue generation can indicate incomplete conversion or unsuitable feedstock preparation. Residue handling systems therefore form an important part of plant design. Efficient discharge and collection support continuous operation while reducing maintenance requirements. Integrating Quality Control into Plant Operation Product quality does not depend on a single parameter. It results from the interaction of feedstock preparation, temperature management, residence time, vapor recovery, and residue control. For companies evaluating a plastic to oil machine for sale , technical assessment should extend beyond nominal production capacity. Feedstock compatibility, thermal stability, condensation efficiency, gas utilization, and residue management all influence the consistency and value of final products. A well-designed pyrolysis system combines these elements into an integrated process. Stable operation, controlled reaction conditions, and effective product recovery can improve the quality of oil, gas, and solid residues while supporting more efficient resource utilization from plastic waste.
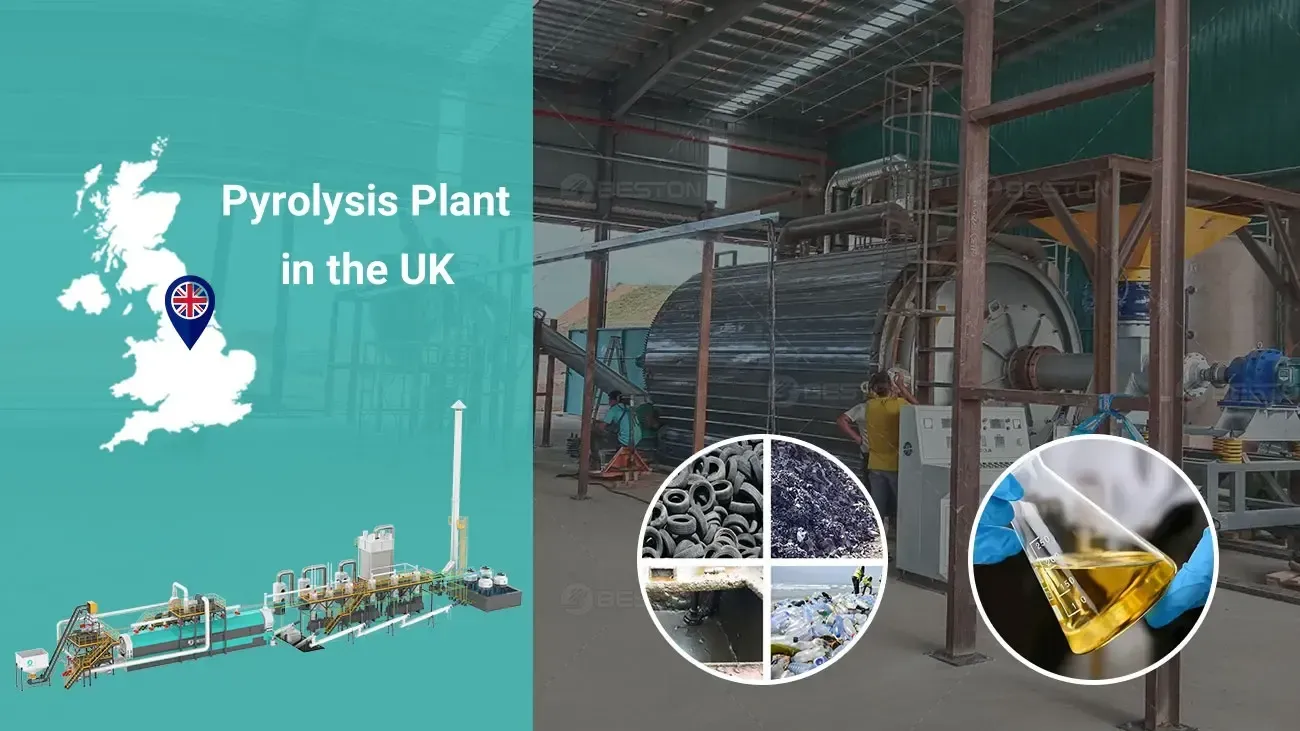
Every year, Britain's roads consume tens of millions of tyres. When they wear out, they become one of the country's most persistent waste streams: bulky, durable, and difficult to recycle. Industry estimates put UK end-of-life tyre (ELT) arisings at roughly 500,000 tonnes a year. With landfill closed to them, how that material is handled has become a defining question for the recycling sector. The Tyre Landfill Ban: What Changed The UK has not banned landfill in general. Many wastes can still be landfilled, subject to permits and Landfill Tax. Tyres, however, are a specifically restricted category. Whole tyres were banned from landfill in 2003, and shredded tyres followed in 2006. The reasoning was sound. Tyres trap gases, tend to work their way up through landfill layers, and consume valuable void space. Stockpiles are just as problematic: tyre fires are notoriously hard to extinguish and release harmful emissions. With landfill off the table, ELTs have followed three main routes: material recovery (crumb and granulate for surfacing and infrastructure), energy recovery (chiefly cement kilns and tyre-derived fuel), and export. Each has limits. Crumb markets are finite, energy recovery does little to keep materials in circulation, and exporting shifts environmental responsibility overseas at a time when regulators and customers are asking tougher questions about where waste ends up. Enter Pyrolysis Pyrolysis heats shredded tyres in an oxygen-free reactor, breaking them down thermally rather than burning them. The process yields three principal outputs: pyrolysis oil, recovered carbon black (rCB), and steel wire. It also produces a non-condensable syngas, which is typically recycled to heat the reactor. This is why interest in the pyrolysis plant UK operators can deploy is rising. Pyrolysis converts a low-value, hard-to-handle waste into several marketable products, and it can process feedstock that is unsuitable for mechanical recycling. Because the syngas can supply much of the process heat, well-designed plants can be reasonably energy self-sufficient once running. Where the Value Lies Carbon black. Recovered carbon black is arguably the most strategically important product. Tyre and rubber manufacturers face growing pressure to increase recycled content, and rCB offers a lower-carbon alternative to virgin carbon black made from fossil feedstocks. The challenge is consistency: buyers need tightly specified material, so post-processing and quality control are critical. Pyrolysis oil. The oil can be used as an industrial fuel or upgraded as a petrochemical feedstock. Access to premium markets depends on refining and on regulatory clarity about when the material stops being classed as waste. Steel. Recovered steel is easy to sell into established scrap markets and adds useful secondary revenue. Challenges Developers Must Address The opportunity is real, but so are the hurdles: Permitting. Thermal treatment facilities need environmental permits, and regulators scrutinise emissions controls, abatement systems, and monitoring closely. Early engagement with the environmental regulator and local planning authority is essential. Feedstock security. Reliable, contracted tyre supply at predictable cost underpins any business case. Relationships with collectors and processors matter as much as reactor design. Product specification. Offtake agreements for oil and carbon black should be pursued early, with clear quality standards. Community acceptance. Thermal technologies attract public scrutiny. Transparent communication about emissions, traffic, and safety builds trust. Technology choice. Batch, semi-continuous, and continuous systems differ significantly in throughput, maintenance demands, and capital cost. Independent due diligence on reference plants is well worth the investment. Policy Tailwinds Broader trends favour recycling routes that return materials to the economy. Resource-efficiency goals, continuing discussion of producer responsibility approaches for tyres, and industry commitments to recycled content all point toward growing demand for verified, traceable secondary materials. Tyre manufacturers and fleet operators increasingly want demonstrable end-of-life solutions, and pyrolysis can offer a credible story when supported by robust carbon accounting and certification. Looking Ahead The tyre landfill ban solved one problem and created another: what to do with half a million tonnes of durable, high-energy material each year. Pyrolysis offers a technically proven answer, but success depends on execution. That means disciplined feedstock sourcing, realistic financial modelling, high-quality outputs, and open engagement with regulators and communities. For investors, waste operators, and technology providers, the message is encouraging. As the UK tightens its approach to waste and raises its circular-economy ambitions, a well-run pyrolysis plant UK projects can build is well placed to turn a regulatory constraint into a durable commercial opportunity.
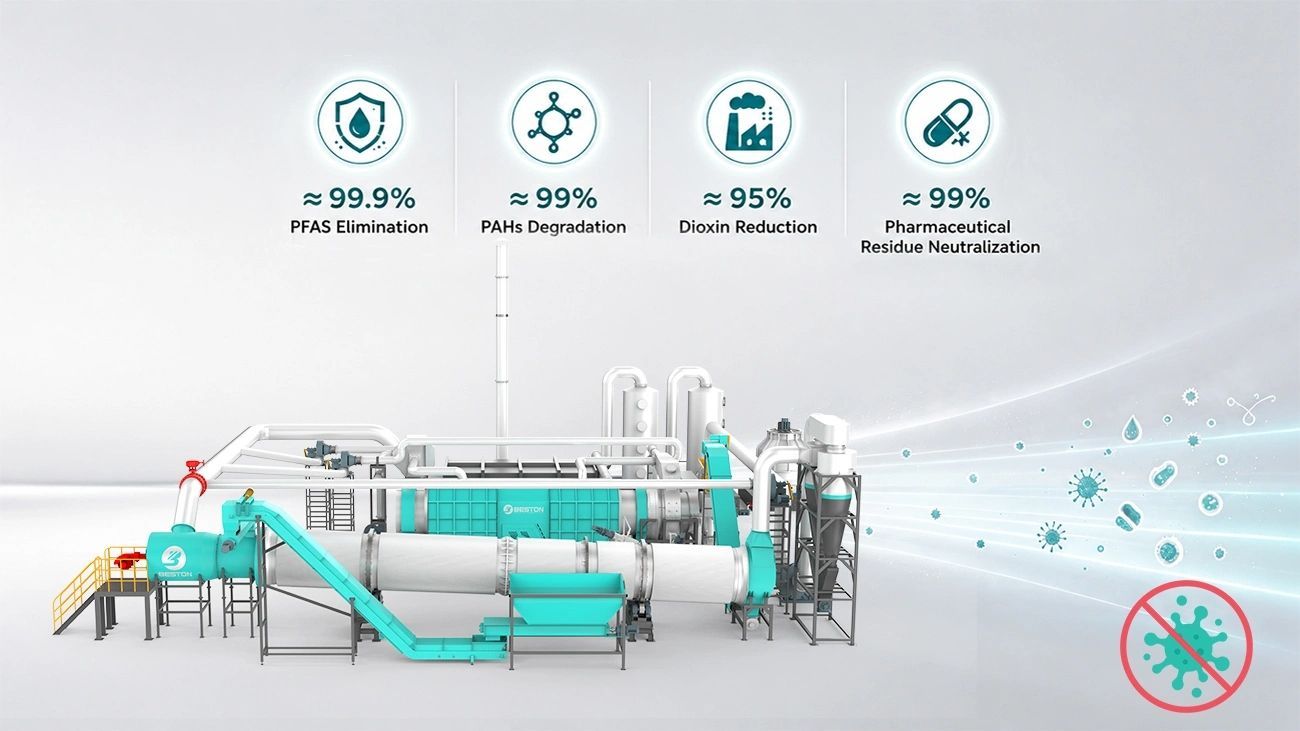
Municipal and industrial wastewater treatment facilities generate large volumes of sludge as a by-product of purification processes. This material often contains organic matter, moisture, inorganic minerals, and trace contaminants, making disposal both technically challenging and economically significant. Traditional management methods, such as landfilling, incineration, and direct land application, are increasingly influenced by environmental regulations, transportation costs, and resource-recovery objectives. Against this background, sewage sludge pyrolysis has emerged as a thermochemical pathway that converts sludge into carbon-rich products while reducing waste volume. Characteristics of Sewage Sludge as a Feedstock Sewage sludge differs substantially from conventional biomass feedstocks. Moisture content is often high, and ash concentrations can vary depending on wastewater composition and treatment processes. In addition, sludge may contain nutrients, metals, inorganic compounds, and residual organic substances. These characteristics influence thermal behavior during pyrolysis. Feedstock preparation therefore becomes an important step. Mechanical dewatering, thermal drying, and particle-size homogenization can improve process stability and reduce unnecessary energy consumption. The selection of pretreatment methods depends on sludge properties, local infrastructure, and the intended application of the final carbon product. Thermal Conversion Through Sewage Sludge Pyrolysis Pyrolysis involves heating organic material under oxygen-limited conditions, allowing thermal decomposition to occur without complete combustion. During sewage sludge pyrolysis , complex organic compounds are transformed into three principal fractions: Carbon-rich solid products; Condensable liquids; Non-condensable gases. The distribution of these products depends on reactor temperature, heating rate, residence time, and feedstock composition. Compared with direct incineration, pyrolysis emphasizes resource recovery alongside waste reduction. Organic carbon is retained partially within the solid product, while combustible gases can contribute to process heating after appropriate treatment. The process also reduces sludge volume significantly, thereby lowering transportation and disposal requirements. Reactor and Equipment Considerations Sludge processing requires equipment designed to accommodate feedstocks with varying moisture levels, particle characteristics, and ash content. A sludge pyrolysis system generally includes: Feedstock pretreatment equipment; Drying units; Thermal conversion reactor; Condensation system; Gas-utilization section; Solid-product cooling system; Emission-control equipment. The reactor is the core component. Rotary kilns, screw reactors, and other indirectly heated systems are frequently used because they provide controlled material movement and stable heat transfer. Temperature management is essential. Excessive temperatures can reduce solid-product yield, while insufficient thermal input may result in incomplete conversion. Process automation and instrumentation help maintain stable operating conditions. Carbon Products and Resource Recovery One of the key outcomes of sewage sludge pyrolysis is the generation of carbon-containing solids. Depending on feedstock composition and processing conditions, these materials may contain fixed carbon, mineral matter, and nutrient elements. Potential applications vary according to product quality, local regulations, and technical requirements. In some contexts, carbon products may be considered for industrial applications, construction materials, or further upgrading processes. Comprehensive characterization is necessary before determining suitable end uses. The gaseous fraction also has value. After purification and controlled combustion, non-condensable gas can provide part of the thermal energy required for the pyrolysis process. This internal energy loop may improve overall thermal efficiency. Emission Control and Environmental Considerations Sludge treatment technologies must address emissions carefully. Pyrolysis systems therefore require integrated gas cleaning and environmental control measures. Dust removal, condensation, thermal oxidation, and exhaust-gas treatment may be incorporated depending on process design and regulatory requirements. Continuous monitoring of temperature, pressure, and emissions can further improve operational reliability. Attention should also be given to the management of inorganic residues and potential contaminants. Product testing remains essential to ensure that recovered materials meet applicable standards. From Waste Management to Carbon Resource Utilization The concept behind sewage sludge pyrolysis extends beyond disposal. Instead of treating sludge solely as a waste stream, pyrolysis views it as a source of carbon, energy, and potentially useful materials. A complete process chain—comprising dewatering, drying, thermal conversion, gas utilization, product cooling, and emission control—can transform complex sludge streams into more stable products while reducing waste volume. As wastewater treatment facilities seek more circular resource-management strategies, sludge pyrolysis machines provide a technological pathway that links waste reduction, energy recovery, and carbon-product generation within a single thermochemical system.
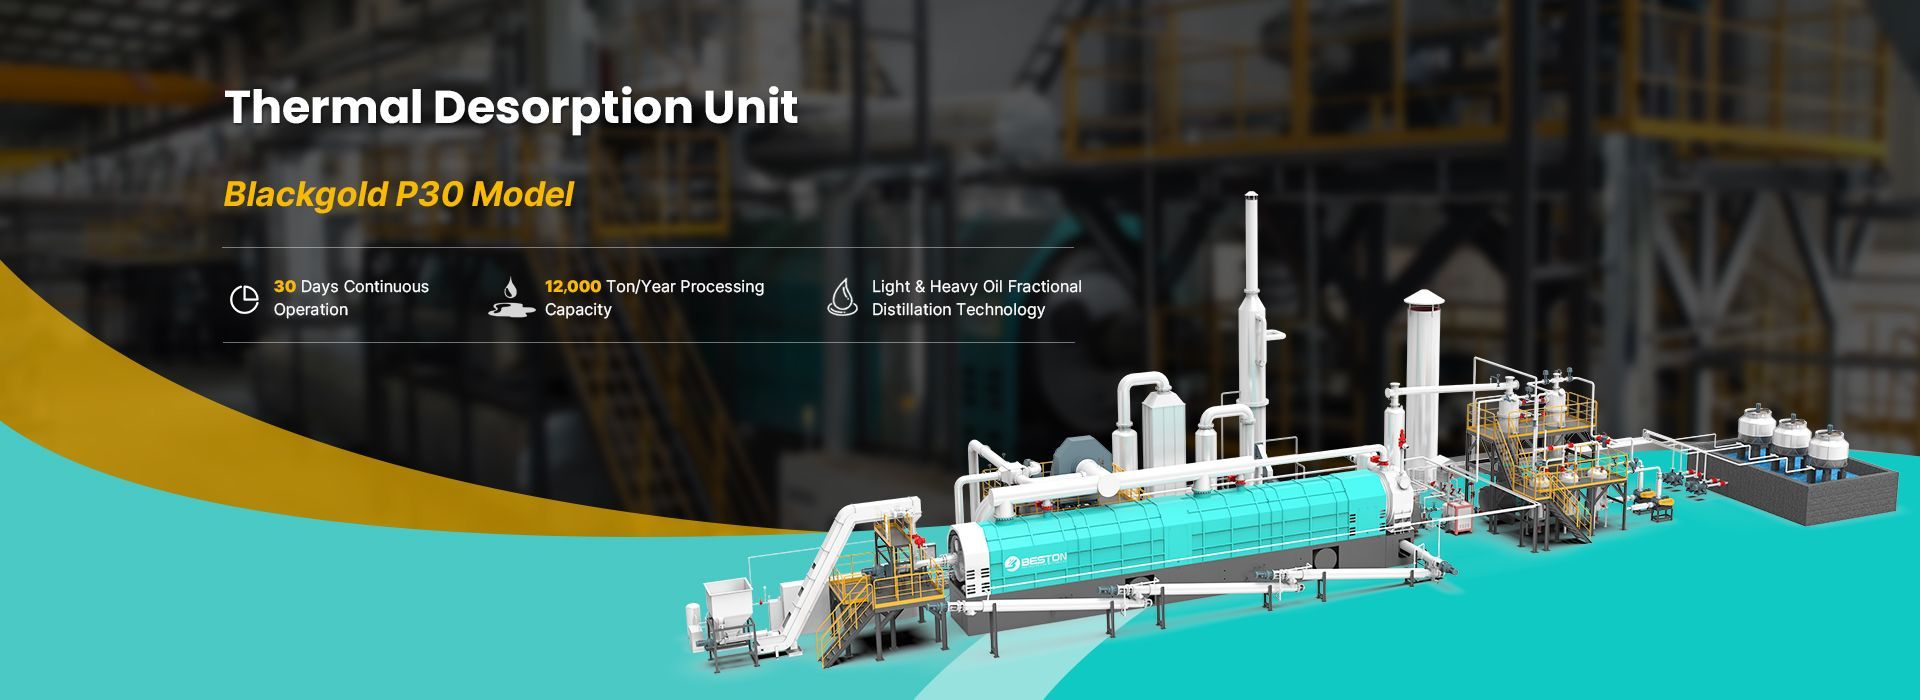
Thermal desorption is widely used to treat oily wastes and recover hydrocarbons from contaminated solids. However, not all oily waste behaves the same way during thermal treatment. Tank bottom sludge, refinery sludge, and drilling waste can have very different moisture levels, hydrocarbon contents, particle characteristics, and inorganic compositions. These differences directly affect how a thermal desorption unit (TDU) should be configured. Choosing equipment based only on daily processing capacity can lead to inefficient heating, unstable feeding, excessive energy consumption, or difficulties with downstream vapor treatment. Understanding the feedstock is therefore one of the first steps in designing an appropriate TDU system. 1. Tank Bottom Sludge: High Hydrocarbon Variability Tank bottom sludge accumulates at the bottom of crude oil, fuel, and other hydrocarbon storage tanks. It typically contains a mixture of hydrocarbons, water, sediment, rust, and other solid contaminants. Its composition can vary considerably depending on the stored material, tank operating history, and cleaning method. Some tank bottoms may contain a relatively high proportion of recoverable hydrocarbons, while others may contain large amounts of water and inorganic solids. For a TDU system, this variability makes feedstock analysis particularly important. The heating system must provide sufficient energy to remove water and hydrocarbons without unnecessarily increasing the treatment temperature. Feed handling is also important because sticky sludge can be difficult to transport. Mixing, dewatering, or other pretreatment may be required depending on its physical condition. 2. Refinery Sludge: More Complex Contaminants Refinery sludge can originate from crude oil processing, wastewater treatment, separators, storage facilities, and other refinery operations. Its composition may include hydrocarbons, water, catalysts, mineral solids, and other process-related contaminants. Because refinery sludge can come from different sources within the same facility, its properties may vary from one stream to another. A thermal desorption unit designed for refinery sludge may therefore require greater flexibility in temperature control, feeding, vapor condensation, and gas treatment. Corrosive compounds should also be considered when selecting equipment materials and downstream components. For larger projects, separating different sludge streams before treatment can make process control easier and provide more predictable operating conditions. 3. Drilling Waste: Water and Solids Become Critical Drilling waste, including oil-based drilling cuttings, has a different physical structure from many tank or refinery sludges. It can contain rock cuttings, drilling fluids, oil, water, and various additives. The solid content can be relatively high, and particle size may vary significantly. This affects feeding, heat transfer, and residence time inside the thermal treatment equipment. Moisture is another major consideration. If drilling waste contains substantial water, a significant portion of the thermal energy supplied to the system may be consumed by water evaporation. The TDU design therefore needs to account for both the hydrocarbon removal target and the energy required to heat and evaporate the water fraction. 4. Feedstock Changes the Heating Requirement One of the most important differences among these feedstocks is moisture content. Water requires substantial energy to heat and vaporize. Two systems processing the same mass of waste can therefore have very different energy requirements if their moisture levels differ. Hydrocarbon content also affects the thermal balance. Volatile hydrocarbons released during treatment can be recovered through condensation, while non-condensable gases may potentially be used as part of the plant's heating system, depending on their composition and system design. Consequently, the TDU should be sized according to the actual feed composition rather than simply using tons per day as the only design parameter. 5. Feeding and Material Handling Need to Match the Waste Physical characteristics can be just as important as chemical composition. Sticky tank sludge may require specialized feeding equipment. Refinery sludge may need mixing to maintain a relatively uniform feed. Drilling cuttings may require conveyors or other solids-handling equipment capable of dealing with abrasive particles. Pretreatment can also influence overall plant performance. Removing excess water, breaking up large particles, or homogenizing the feed can improve heat transfer and make the thermal process more stable. 6. Vapor and Condensation Systems May Differ The composition of vapors released during thermal treatment depends on the feedstock. A hydrocarbon-rich sludge may generate substantial quantities of condensable oil vapors. Water-rich waste can produce a significant water vapor load. Other contaminants may require additional gas cleaning or treatment. The condenser, oil-water separation system, non-condensable gas handling, and emission-control equipment should therefore be designed around the expected vapor composition. This is particularly important when different waste streams are expected to be processed in the same TDU. A system designed around one feedstock should not automatically be assumed to perform identically with another. 7. Reactor Material and Wear Also Matter Feedstock can influence equipment durability. Drilling waste containing abrasive mineral particles may create greater mechanical wear than relatively soft sludge. Certain refinery and tank-bottom wastes may contain corrosive compounds that require appropriate material selection. The reactor, feeding equipment, conveyors, seals, and other components should therefore be evaluated according to both chemical and mechanical conditions. 8. A Feedstock-Based TDU Design Approach Before selecting a thermal desorption unit, operators should collect representative feedstock data, including: Moisture content Oil and hydrocarbon content Solid content Particle size Density Salt and mineral content Potentially corrosive compounds Daily and seasonal volume variations This information can then be used to determine heating capacity, reactor throughput, residence time, feeding requirements, condensation capacity, and gas-treatment needs. Conclusion Tank bottom sludge, refinery sludge, and drilling waste may all be described as oily wastes, but they can behave very differently during thermal treatment. Tank bottom sludge often presents variability in hydrocarbon and sediment content, refinery sludge can contain complex mixtures of process contaminants, and drilling waste can introduce significant water, solids, and abrasion considerations. For this reason, a thermal desorption unit should be designed around the specific characteristics of the feedstock. A successful TDU setup is not simply a matter of selecting the largest available capacity—it requires matching the heating system, feeding equipment, reactor configuration, condensation system, and emission controls to the waste being processed.
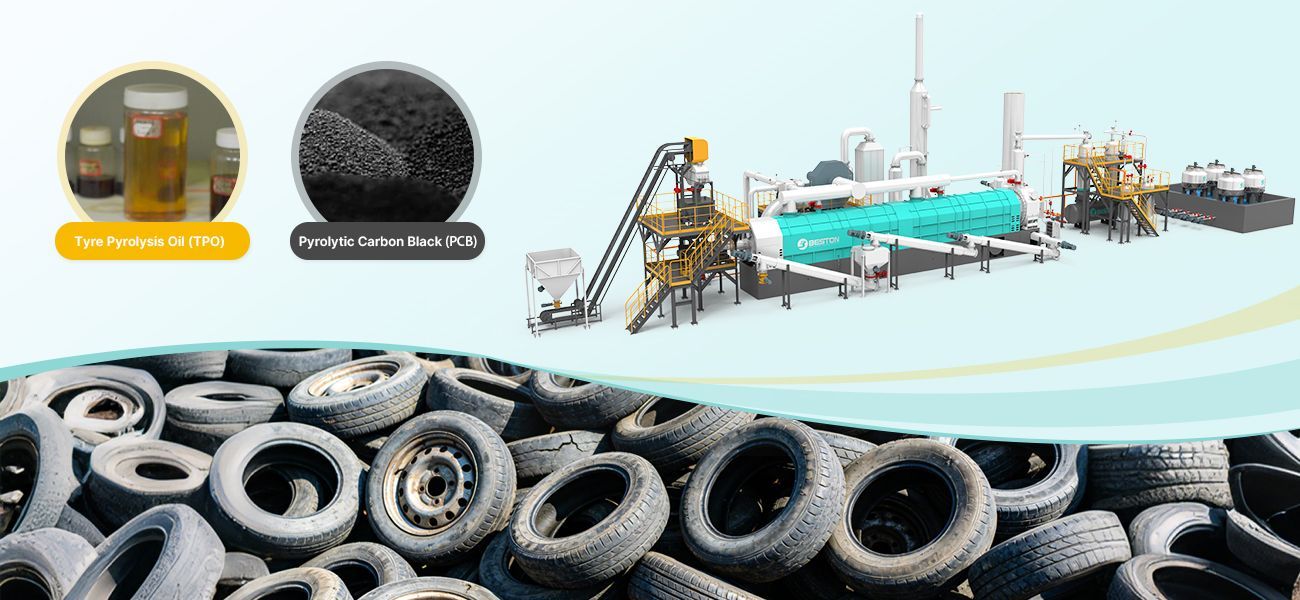
Operating a tyre pyrolysis facility involves high temperatures, combustible gases, flammable liquids, rotating machinery, and pressurized process equipment. A well-engineered tyre to oil plant therefore requires safety controls that address the entire process chain, from tyre preparation and feeding to pyrolysis, gas handling, oil condensation, residue discharge, and storage. Safety should be integrated into equipment design and operating procedures rather than treated as a separate compliance activity. Process Safety Starts with Hazard Identification Before commissioning, the major hazards should be identified through a structured process hazard assessment. Typical scenarios include reactor overheating, combustible-gas leakage, abnormal pressure, loss of cooling, feed-system blockage, and ignition of hydrocarbon vapors. A HAZOP (Hazard and Operability Study) can be used to systematically examine deviations such as excessive temperature, insufficient flow, or unexpected pressure. Emergency scenarios should also be evaluated through risk assessment and operating procedures. The assessment should consider both normal operation and foreseeable abnormal conditions. Interlocks, alarms, emergency shutdown systems, pressure-relief devices, and temperature monitoring can then be incorporated according to the identified hazards. Temperature and Pressure Require Continuous Control Pyrolysis occurs at elevated temperatures, making thermal control one of the fundamental safety requirements. Excessive heating can accelerate unwanted secondary reactions, increase gas generation, and place additional stress on process components. A modern tyre to oil plant should use multiple temperature-monitoring points rather than relying on a single measurement. Automated control can regulate the heating system and trigger protective actions when predefined limits are exceeded. Pressure control is equally important. The reactor and connected piping should be designed for the applicable operating conditions, with appropriate pressure-relief and isolation provisions. Sudden pressure changes may indicate condensation problems, blockage, excessive gas production, or abnormal operating conditions and should be investigated immediately. Combustible Gas Management Prevents Ignition Hazards Pyrolysis generates non-condensable gases containing combustible hydrocarbons. These gases can be recovered as process fuel, but uncontrolled accumulation presents a significant fire and explosion hazard. Gas piping should be properly sealed and routinely inspected for leakage. Pressure, flow, and temperature should be monitored at critical locations. Where applicable, gas detection and ventilation systems can provide additional protection around areas where combustible gases may accumulate. Ignition sources must also be controlled. Electrical equipment installed in hazardous areas should be appropriately selected for the classified environment, while hot surfaces, sparks, and unauthorized flame sources should be prevented from contacting hydrocarbon vapors. Feedstock Preparation and Mechanical Safety Matter Tyres contain steel reinforcement and other materials that can create mechanical hazards during cutting, shredding, and conveying. Guards, emergency-stop devices, interlocks, and safe maintenance procedures are essential around rotating and cutting machinery. Feedstock specifications should also be controlled. Oversized tyres, excessive foreign material, or unsuitable inputs can cause feeding difficulties and mechanical obstruction. Consistent feed preparation helps reduce both operational instability and equipment stress. Lockout/tagout procedures should be applied before maintenance or cleaning activities involving electrical, mechanical, thermal, or pneumatic energy. Fire Protection and Emergency Response Fire protection should cover the reactor area, gas system, oil-processing section, and product-storage area. Appropriate extinguishing systems, fire detection, emergency shutdown controls, clearly marked escape routes, and accessible emergency equipment are fundamental components of the safety strategy. Operators should receive documented training for abnormal conditions, including power failure, cooling-system failure, gas leakage, excessive temperature, and emergency shutdown. Regular drills can verify whether procedures are practical rather than merely documented. Compliance Requires More Than Equipment Certification Applicable standards vary by country and project configuration. Depending on the jurisdiction, requirements may cover pressure equipment, electrical installations, hazardous-area classification, fire protection, occupational safety, emissions, and environmental permitting. For a tyre to oil plant, compliance should therefore be verified against the regulations and recognized standards applicable at the installation site. Equipment documentation, inspection records, maintenance schedules, operating procedures, and staff training should form part of the overall safety management system. Ultimately, safe tyre pyrolysis depends on layered protection: sound mechanical design, reliable instrumentation, controlled operating parameters, effective gas management, preventive maintenance, and trained personnel. No single safety device can compensate for weaknesses elsewhere in the process.
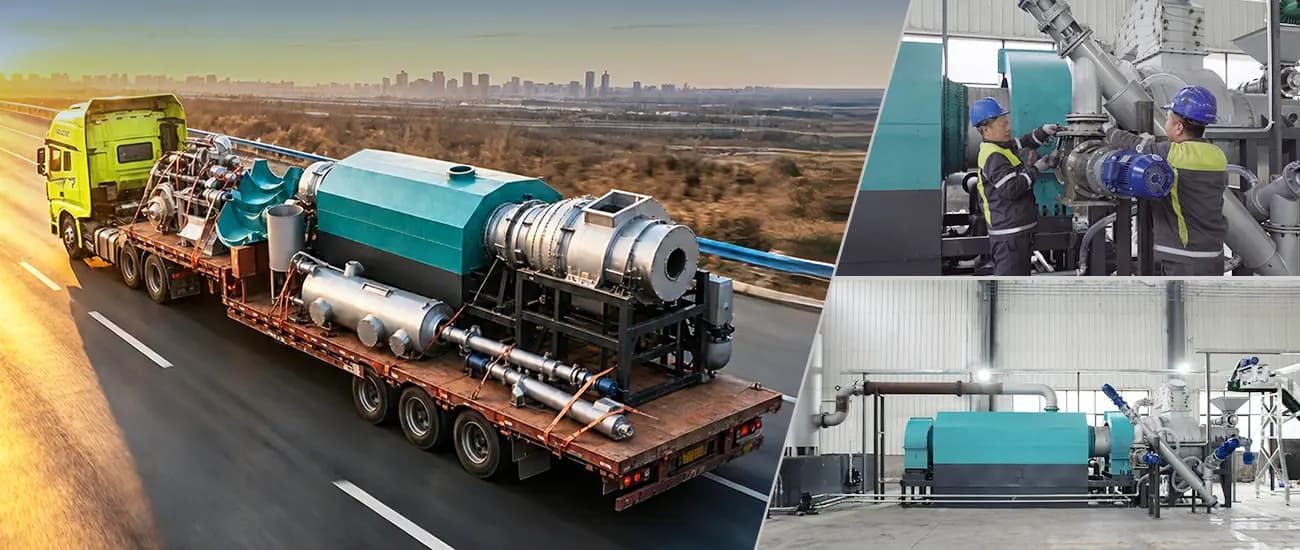
Biomass waste is often generated far away from centralized processing facilities. Agricultural residues, forestry waste, orchard prunings, and other organic materials may need to be collected and transported before they can be converted into useful products. For businesses handling large quantities of low-density biomass, transportation can become a significant part of the overall operating cost. A mobile biochar machine offers a different approach: instead of transporting all the raw biomass to a fixed processing plant, the carbonization equipment can be moved closer to where the biomass is generated. By processing biomass on-site, businesses can reduce unnecessary transportation and convert bulky organic waste into a more compact, valuable carbon-rich product. Why Biomass Transportation Can Be Expensive Many types of biomass have a relatively low bulk density. Straw, branches, leaves, sawdust, and other agricultural residues can occupy considerable space compared with their actual dry weight. This creates a transportation challenge. Trucks may reach their volume limit before reaching their maximum weight capacity. At the same time, biomass with high moisture content can add substantial weight without increasing its energy or carbon value. Transportation costs therefore depend not only on the amount of biomass available but also on its moisture content, bulk density, transportation distance, loading efficiency, and local fuel prices. When biomass is generated across multiple farms or remote sites, repeatedly transporting it to a centralized facility can make waste processing less economical. How On-Site Carbonization Changes the Logistics Model A mobile biochar machine changes the traditional biomass logistics chain. Instead of following the model of: Biomass collection → Long-distance transportation → Fixed plant → Carbonization → Biochar distribution A mobile biochar machine can support: Biomass collection → On-site carbonization → Biochar transportation This means that part of the biomass handling process occurs close to the source. After carbonization, the resulting biochar is generally more concentrated than the original loose biomass, making subsequent transportation and storage easier to manage. The actual reduction in transportation cost depends on feedstock characteristics, processing conditions, distance, and local logistics. However, the fundamental advantage is straightforward: businesses can avoid transporting material that does not need to travel long distances in its original bulky form. Suitable Applications for Mobile Biochar Machines Mobile biochar equipment is particularly attractive when biomass is geographically dispersed. For example, agricultural producers may generate large amounts of crop residues after harvesting. Forestry operations can produce branches, bark, and other wood residues across different sites. Orchards generate pruning waste seasonally, often in locations that are not close to industrial processing facilities. In these situations, moving a mobile biochar machine between biomass collection areas can provide greater flexibility than building a fixed facility at every location. The approach can also be useful for biomass contractors and waste management companies that serve multiple customers. Instead of relying on a single permanent processing site, operators can bring carbonization capacity closer to different biomass sources. Lower Transportation Volume, Higher Resource Value The transportation advantage is only one part of the equation. On-site carbonization can also change the value of the biomass. Raw agricultural waste may have limited commercial value because of its high moisture content, low bulk density, or limited local demand. After controlled carbonization, it becomes biochar, a stable carbon-rich material that can be used in soil management, composting, growing media, and other applications depending on its properties. This creates a potential transition from a waste-disposal cost to a resource-recovery model. Instead of asking, “How much will it cost to transport this waste?” businesses can begin asking, “Can we process this waste where it is generated and sell or use the resulting biochar?” Important Factors When Choosing Mobile Equipment Not every biomass operation requires the same mobile biochar machine. Several factors should be evaluated before investment. First, the equipment should match the actual feedstock. Moisture content, particle size, density, and composition can significantly affect carbonization performance. Second, mobility should be considered together with production capacity. A machine that is easy to relocate but has insufficient throughput may not meet the needs of a commercial operation. Third, energy efficiency is important. A well-designed system can recover combustible gases generated during carbonization and use them as a supplementary heat source, reducing external fuel consumption. Finally, automation, temperature control, sealing, cooling, and emissions management should be considered as part of the complete system rather than as optional features. Is Mobile Biochar Production Right for Your Business? A mobile biochar machine is most attractive when biomass is abundant but geographically dispersed, transportation distances are significant, and building multiple fixed processing facilities is impractical. It may not completely eliminate transportation costs, because biomass still needs to be collected and the finished biochar may need to reach its final destination. However, changing **what is transported, where it is processed, and when it is moved** can significantly improve the overall logistics model. For agricultural businesses, forestry operators, biomass contractors, and decentralized waste management projects, on-site carbonization provides a practical way to bring processing capacity closer to the feedstock. Ultimately, the value of a mobile biochar machine is not simply its ability to move from one location to another. Its real advantage is the possibility of processing biomass where it is generated, reducing the burden of transporting bulky raw materials while creating a more valuable and stable biochar product.
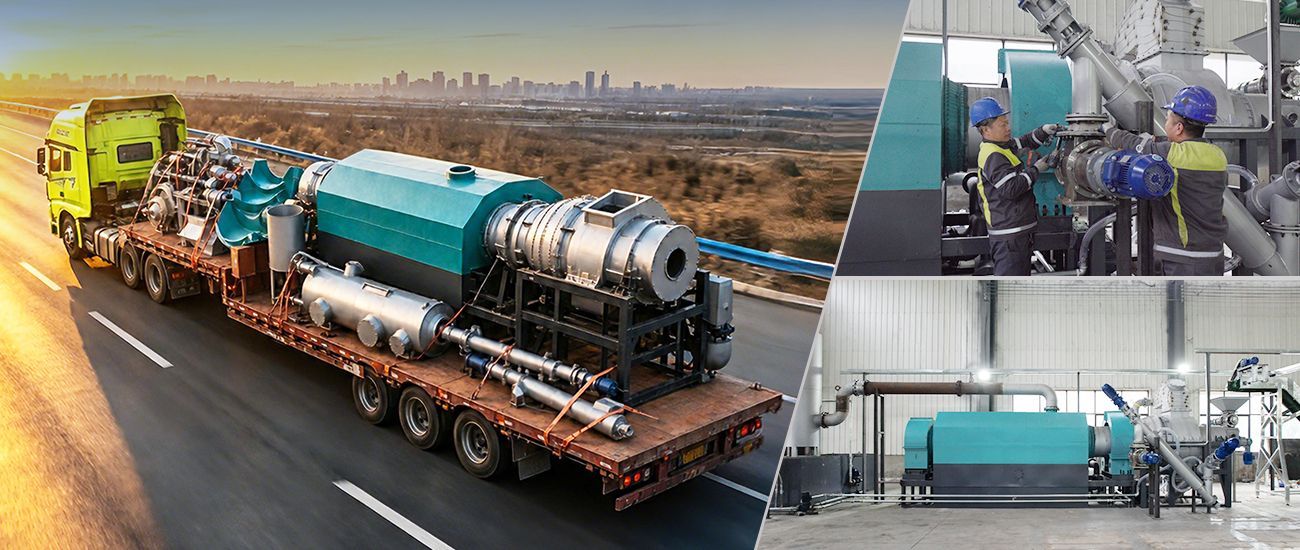
Agricultural residues are often treated as low-value by-products, yet materials such as pruning branches, nut shells, straw, and other woody biomass contain substantial quantities of carbon. A portable biochar kiln provides farmers with a practical way to convert these residues into stable carbon-rich biochar directly near the point of generation. This localized approach reduces unnecessary biomass transport while creating a material that can be returned to soil or used in other agricultural applications. Bringing Carbon Conversion Closer to the Farm Conventional biomass processing can require centralized facilities, dedicated transportation, and substantial material handling. For farms with dispersed fields or seasonal residues, these requirements may undermine the economic feasibility of carbon management. A portable biochar kiln changes this logistical equation. Its mobility allows the equipment to be positioned close to orchards, plantations, forestry plots, or crop-production areas where biomass accumulates. Instead of hauling bulky, low-density residues over long distances, operators can process feedstock nearer to its source. This is particularly relevant for pruning residues. Orchard maintenance can generate large volumes of branches within a limited harvesting period. Converting this material on-site reduces transportation requirements and transforms an agricultural liability into a carbon-rich product. Pyrolysis Converts Residues into Stable Carbon The underlying principle is controlled thermal decomposition under oxygen-limited conditions. During pyrolysis, biomass is heated while excessive oxygen exposure is restricted. Volatile compounds are released, while part of the original carbon becomes concentrated in a relatively stable solid fraction. The resulting biochar differs fundamentally from untreated biomass. Its carbon structure is more resistant to rapid biological decomposition, which allows a portion of the carbon to remain in soil for considerably longer periods than fresh plant residues. For carbon-sequestration projects, however, the kiln itself is only one component of the equation. Feedstock characteristics, operating temperature, residence time, biochar properties, and measurement procedures all influence the eventual carbon-removal performance. A More Decentralized Carbon-Removal Model Farm-scale biochar production introduces a decentralized model for agricultural carbon management. Rather than transporting biomass to a distant processing facility, the conversion step can occur close to the feedstock. This creates several potential advantages: Lower biomass transportation demand : Processing near the source can reduce the movement of bulky residues. Better residue utilization : Agricultural by-products can become a usable soil amendment instead of remaining unmanaged. Carbon retention : A fraction of biomass carbon is transformed into a more persistent form. Soil-management potential : Properly characterized biochar may contribute to soil structure, water retention, and nutrient-management strategies. Operational flexibility : A mobile unit can be relocated according to seasonal biomass availability. The significance extends beyond individual farms. When replicated across multiple agricultural operations, decentralized biochar production can form a distributed carbon-removal network. Matching the Portable Biochar Kiln to Farm Conditions Not every farm has the same feedstock or operating environment. A suitable portable biochar kiln should therefore be evaluated according to biomass type, moisture content, particle dimensions, expected throughput, available energy sources, and local operating conditions. Feedstock preparation deserves particular attention. Excessive moisture can increase thermal energy requirements, while inconsistent particle size may affect heat transfer and conversion uniformity. A well-defined feedstock specification helps stabilize operation and produce biochar with more predictable characteristics. Carbon accounting also requires discipline. If biochar is intended for a certified carbon-removal project, documentation should cover feedstock origin, processing parameters, biochar quantity, carbon content, and the eventual application pathway. Measurement, reporting, and verification are essential for distinguishing genuine carbon removal from simple biomass disposal. From Agricultural Residue to Long-Term Carbon Storage The real innovation of portable biochar technology is not simply its compactness. It is the ability to integrate biomass management, thermal conversion, and carbon sequestration closer to where agricultural residues are produced. As farms pursue lower-emission production systems, the portable biochar kiln can serve as a bridge between residue management and durable carbon storage. Its value lies in turning a geographically dispersed biomass resource into a measurable carbon-management opportunity—while potentially generating a useful agricultural product at the same time.
End-of-life tyres present a formidable municipal and industrial waste challenge due to their cross-linked vulcanized rubber matrices and resistance to natural biodegradation. Stockpiling these elastomeric wastes creates persistent fire hazards and vector-breeding habitats. Conventional disposal methods like landfilling or direct incineration fail to capture the high-value hydrocarbons embedded within synthetic and natural rubber compounds. Implementing an industrial pyrolysis plant for end-of-life tyres provides a thermochemical conversion pathway that depolymerizes scrap rubber into valuable chemical fractions, liquid fuels, and solid carbonaceous residues. Thermochemical Mechanisms of Tyre Rubber Depolymerization Tyre rubber is a complex composite consisting of polyisoprene, polybutadiene, styrene-butadiene rubber, carbon black, steel cord, and inorganic additives. Converting this complex matrix requires precise thermal cracking within an oxygen-deprived environment. A specialized waste tire pyrolysis equipment operates by breaking the strong covalent carbon-carbon and carbon-sulfur bonds that constitute the vulcanized rubber lattice. When scrap tyres are heated to temperatures between 400°C and 600°C, the organic polymer chains undergo scission without combustion. Thermal degradation initiates with the cleavage of weak polysulfidic cross-links before progressing to the random scission of the main hydrocarbon backbone. This devolatilization phase generates a complex mixture of condensable hydrocarbon vapors, non-condensable permanent gases, and a non-volatile solid fraction consisting of carbon black and inorganic fillers. Core Operational Stages of Industrial Pyrolysis Systems The transformation of whole or shredded tires into refined outputs relies on a series of integrated mechanical and thermal operations designed for safety and material stability: Feedstock Pre-Treatment: Whole tyres undergo mechanical de-beading to extract high-tensile steel wire bundles prior to shredding. The remaining rubber is processed into uniform shreds to optimize thermal conductivity and ensure steady movement through the reactor feed system. Anoxic Pyrolysis Reactor: The prepared rubber granules are fed into a sealed continuous rotary kiln. Maintaining strict hermetic sealing prevents oxygen ingress, eliminating combustion risks while ensuring the purity of the synthetic vapors generated during thermal cracking. Vapor Condensation and Fractionation: Heavy vapor fractions exit the reactor chamber and enter a multi-stage condensing system. Rapid cooling fractionates condensable hydrocarbons into liquid pyrolytic oil while separating non-condensable light gases for thermal energy recovery. Char Cooling and Magnetic Separation: The hot solid carbon residue exits through a water-jacketed cooling screw to drop the material below auto-ignition temperatures. Inline high-intensity magnetic separators recover fine steel wires before the char undergoes micro-milling. Recovery Profiles and Commercial Output Properties Thermochemical depolymerization yields four distinct, high-value resource streams that integrate directly into industrial manufacturing and energy supply chains: Pyrolytic Oil (Heavy Hydrocarbon Liquid) The primary liquid product is a dark, complex mixture of aromatic, aliphatic, and naphthenic hydrocarbons with a high gross calorific value exceeding 40 MJ/kg. Pyrolytic oil serves as a direct substitute for heavy fuel oil in industrial boilers, furnaces, and power generation systems. Advanced hydro-treating and fractional distillation can further upgrade this liquid into commercial-grade diesel substitutes or chemical feedstocks such as limonene and toluene. Recovered Carbon Black (rCB) The solid char residue remaining after devolatilization contains recovered carbon black alongside zinc sulfide and inorganic fillers. Raw pyrolytic char undergoes pulverization, de-ashing, and pelletization to produce commercial-grade rCB. This material replaces virgin carbon black derived from fossil fuels in semi-reinforcing rubber compounds, masterbatches, coatings, and printing inks, drastically reducing industrial carbon footprints. Non-Condensable Syngas Loop The non-condensable gas fraction consists predominantly of methane, ethane, propane, hydrogen, and hydrogen sulfide. Instead of venting or flaring these gases, the plant routes them through gas scrubbing units to remove sulfur compounds before directing the purified syngas back into the furnace burners. This closed-loop thermal integration makes the continuous operational cycle self-sustaining, minimizing reliance on external fuel sources. High-Tensile Steel Wire Recovery Steel wire extracted during pre-treatment and post-pyrolysis magnetic separation retains high tensile strength and structural integrity. Recovered steel is directed to scrap metal recyclers and electric arc furnace steelmakers for remelting, establishing a complete circular economy for tyre reinforcement materials. By integrating continuous thermochemical processing, modern processing units divert millions of scrap tyres from landfills while yielding essential raw materials for energy and manufacturing sectors.
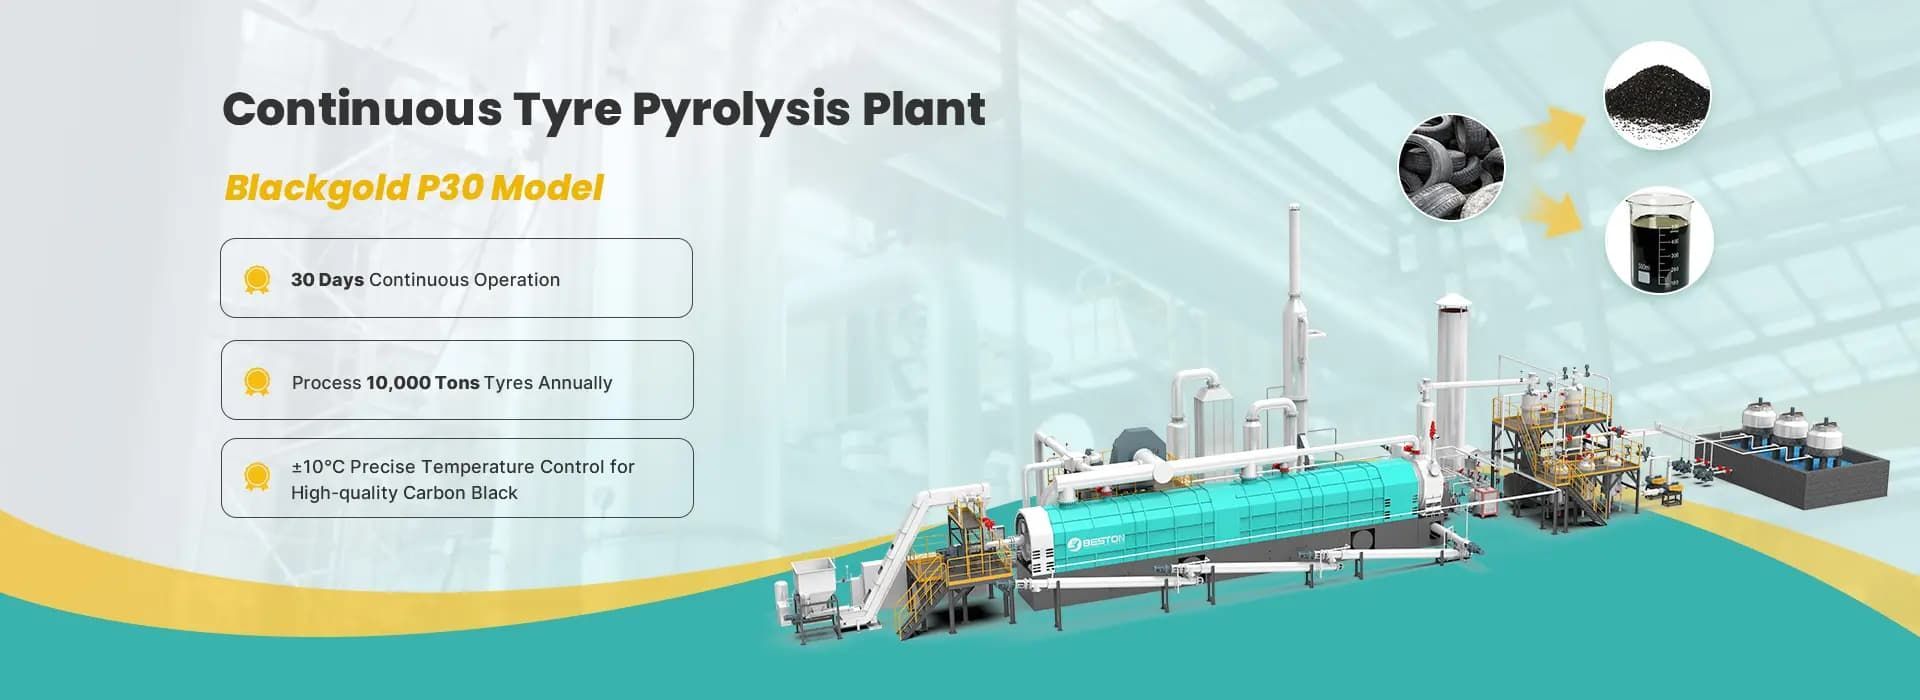
In continuous waste tire pyrolysis systems, the thermal reactor is designed to operate under stable feeding, heat transfer, and reaction conditions. Unlike batch pyrolysis equipment, continuous systems require a consistent and predictable feedstock stream to maintain long-term operation efficiency. For this reason, waste tire shredding and steel wire removal (wire drawing) are not simply pre-treatment steps — they are key processes that directly determine the stability, efficiency, and product quality of the entire pyrolysis operation. Proper size reduction and steel separation help ensure smooth feeding, uniform heating, reduced equipment wear, and improved recovery of pyrolysis products. 1. Tire Shredding Ensures Stable Continuous Feeding Whole tires have irregular shapes, high elasticity, and complex structures, making them difficult to feed into a continuous pyrolysis reactor directly. The shredding process breaks waste tires into smaller and more uniform pieces, improving material handling performance. Improved Feeding Consistency Continuous pyrolysis systems rely on a stable material flow. Properly shredded tire chips can be transported more evenly through conveyors or screw feeders, preventing: Feeding interruptions; Material bridging or blockage; Uneven reactor loading. A consistent feed rate allows the reactor to maintain stable operating parameters, including temperature and residence time. Enhanced Heat Transfer Efficiency Pyrolysis requires sufficient heat transfer from the reactor wall to the rubber material. Large tire pieces may create uneven heating because: The outer surface heats faster than the inner structure; Rubber decomposition may become incomplete; Residence time requirements may increase. After shredding, smaller tire particles provide a larger surface area, allowing heat to penetrate more efficiently and improving hydrocarbon release during pyrolysis. 2. Wire Drawing Protects Equipment and Improves System Reliability Waste tires contain steel reinforcement wires, especially in truck and passenger vehicle tires. If excessive steel enters the pyrolysis reactor, it can negatively affect continuous operation. Steel wire removal before pyrolysis helps maintain equipment reliability. Reducing Reactor Wear and Mechanical Stress Steel wires are harder and more abrasive than rubber materials. During continuous operation, excessive metal content may cause: Increased wear on internal reactor components; Damage to feeding mechanisms; Higher maintenance requirements. Removing steel in advance extends equipment service life and improves operational stability. Preventing Material Flow Problems In continuous reactors, smooth material movement is essential. Long steel wires can: Wrap around rotating components; Cause feeding system blockages; Affect the movement of tire chips inside the reactor. Wire drawing reduces these risks and allows rubber-based materials to flow more freely through the system. 3. Improving Pyrolysis Product Quality Pre-treatment also directly affects the quality of recovered products. Higher-Quality Pyrolysis Oil Uniform tire chips enable more complete thermal decomposition, helping produce stable pyrolysis oil with consistent characteristics. Cleaner Recovered Carbon Black Excessive steel contamination may reduce the purity of recovered carbon black (rCB). Effective wire separation improves downstream carbon black processing and increases its potential value in industrial applications. Efficient Steel Recovery Separated tire steel can enter conventional metal recycling channels, creating an additional recovery stream. 4. Supporting Long-Term Continuous Operation Continuous tyre pyrolysis plants are designed for industrial-scale waste tire processing. Unlike occasional treatment units, they often operate for extended periods with high throughput. Stable operation depends on: Feedstock Preparation → Continuous Feeding → Controlled Pyrolysis → Product Recovery Among these stages, shredding and wire drawing create the foundation for reliable operation. Without proper pre-treatment, even advanced pyrolysis equipment may face challenges such as: Fluctuating feed rates; Temperature instability; Reduced oil yield; Increased downtime; Higher operating costs. Conclusion For continuous waste tire pyrolysis systems, shredding and wire drawing are fundamental to achieving stable, efficient, and reliable operation. Shredding creates a uniform feedstock that improves feeding performance and heat transfer efficiency, while wire drawing protects equipment, reduces operational risks, and improves the quality of recovered products. As tire recycling moves toward large-scale industrial applications, effective pre-treatment will remain a critical factor in ensuring continuous pyrolysis systems achieve high availability, consistent output, and long-term economic performance.
The body content of your post goes here. To edit this text, click on it and delete this default text and start typing your own or paste your own from a different source.

The performance of a plastic pyrolysis system is often evaluated by production capacity and energy efficiency. However, product quality remains equally important. In a commercial operation, the composition and consistency of pyrolysis oil, combustible gas, and solid residues determine the potential value of the final products and influence downstream applications. For investors exploring a plastic to oil machine for sale , understanding the factors that affect product quality is essential for making informed technical and economic decisions. Feedstock Composition Determines Product Characteristics Plastic feedstock is the primary variable influencing pyrolysis output. Different polymers exhibit distinct thermal decomposition pathways, resulting in variations in oil composition, gas yield, and solid residue formation. Polyolefin materials such as polyethylene (PE) and polypropylene (PP) generally produce higher liquid yields because their molecular structures favor hydrocarbon generation during pyrolysis. Polystyrene (PS) can generate aromatic compounds, while plastics containing chlorine, oxygen, or other heteroatoms may require additional process control due to the formation of undesirable by-products. Feedstock purity is equally important. Metal fragments, dirt, moisture, and non-target materials can alter thermal behavior and affect the consistency of products. A stable and well-prepared feedstock stream contributes to more predictable operation and product quality. Temperature Control Influences Product Distribution Pyrolysis is fundamentally a temperature-driven process. Reactor temperature affects the extent of polymer cracking and determines the relative proportion of liquid, gas, and solid products. Lower temperatures may lead to incomplete decomposition and higher residue content. Excessively high temperatures, by contrast, can promote secondary cracking reactions, converting condensable hydrocarbons into permanent gases. Maintaining a suitable temperature window allows the system to balance liquid production with gas generation. Temperature uniformity is equally significant. Thermal gradients within the reactor can create heterogeneous reaction zones, leading to fluctuations in product composition. Continuous monitoring and automated control systems help maintain stable operating conditions. Residence Time and Vapor Management The duration that plastic and pyrolysis vapors remain inside the reactor also affects final products. Longer residence times can increase secondary reactions, altering hydrocarbon distribution and reducing the proportion of heavier liquid fractions. Vapor handling systems therefore play an important role. Efficient condensation equipment enables the recovery of condensable hydrocarbons while separating non-condensable gas for energy utilization. The design of condensers, cooling systems, and gas pipelines influences heat transfer efficiency and can affect the composition of collected oil. Insufficient cooling may result in the loss of valuable hydrocarbons, while excessive cooling can increase operational complexity. Role of Non-Condensable Gas Non-condensable gas generated during pyrolysis contains combustible components that can contribute to process heating after suitable treatment. This internal energy circulation reduces dependence on external fuel sources and improves thermal efficiency. Gas composition depends on feedstock type, reactor temperature, and operating conditions. Hydrogen, methane, and light hydrocarbons may be present in varying proportions. Their effective utilization can improve overall energy management within the plant. For buyers comparing a plastic to oil machine for sale , the ability to recover and utilize process gas should be considered alongside reactor design and production capacity. Formation and Management of Solid Residues Solid residues represent the non-volatile fraction remaining after thermal decomposition. Their quantity and characteristics are affected by feedstock composition, operating temperature, and process stability. In plastic pyrolysis, residue may contain carbonaceous material, inorganic additives, pigments, fillers, and traces of contaminants. Excessive residue generation can indicate incomplete conversion or unsuitable feedstock preparation. Residue handling systems therefore form an important part of plant design. Efficient discharge and collection support continuous operation while reducing maintenance requirements. Integrating Quality Control into Plant Operation Product quality does not depend on a single parameter. It results from the interaction of feedstock preparation, temperature management, residence time, vapor recovery, and residue control. For companies evaluating a plastic to oil machine for sale , technical assessment should extend beyond nominal production capacity. Feedstock compatibility, thermal stability, condensation efficiency, gas utilization, and residue management all influence the consistency and value of final products. A well-designed pyrolysis system combines these elements into an integrated process. Stable operation, controlled reaction conditions, and effective product recovery can improve the quality of oil, gas, and solid residues while supporting more efficient resource utilization from plastic waste.
Every year, Britain's roads consume tens of millions of tyres. When they wear out, they become one of the country's most persistent waste streams: bulky, durable, and difficult to recycle. Industry estimates put UK end-of-life tyre (ELT) arisings at roughly 500,000 tonnes a year. With landfill closed to them, how that material is handled has become a defining question for the recycling sector. The Tyre Landfill Ban: What Changed The UK has not banned landfill in general. Many wastes can still be landfilled, subject to permits and Landfill Tax. Tyres, however, are a specifically restricted category. Whole tyres were banned from landfill in 2003, and shredded tyres followed in 2006. The reasoning was sound. Tyres trap gases, tend to work their way up through landfill layers, and consume valuable void space. Stockpiles are just as problematic: tyre fires are notoriously hard to extinguish and release harmful emissions. With landfill off the table, ELTs have followed three main routes: material recovery (crumb and granulate for surfacing and infrastructure), energy recovery (chiefly cement kilns and tyre-derived fuel), and export. Each has limits. Crumb markets are finite, energy recovery does little to keep materials in circulation, and exporting shifts environmental responsibility overseas at a time when regulators and customers are asking tougher questions about where waste ends up. Enter Pyrolysis Pyrolysis heats shredded tyres in an oxygen-free reactor, breaking them down thermally rather than burning them. The process yields three principal outputs: pyrolysis oil, recovered carbon black (rCB), and steel wire. It also produces a non-condensable syngas, which is typically recycled to heat the reactor. This is why interest in the pyrolysis plant UK operators can deploy is rising. Pyrolysis converts a low-value, hard-to-handle waste into several marketable products, and it can process feedstock that is unsuitable for mechanical recycling. Because the syngas can supply much of the process heat, well-designed plants can be reasonably energy self-sufficient once running. Where the Value Lies Carbon black. Recovered carbon black is arguably the most strategically important product. Tyre and rubber manufacturers face growing pressure to increase recycled content, and rCB offers a lower-carbon alternative to virgin carbon black made from fossil feedstocks. The challenge is consistency: buyers need tightly specified material, so post-processing and quality control are critical. Pyrolysis oil. The oil can be used as an industrial fuel or upgraded as a petrochemical feedstock. Access to premium markets depends on refining and on regulatory clarity about when the material stops being classed as waste. Steel. Recovered steel is easy to sell into established scrap markets and adds useful secondary revenue. Challenges Developers Must Address The opportunity is real, but so are the hurdles: Permitting. Thermal treatment facilities need environmental permits, and regulators scrutinise emissions controls, abatement systems, and monitoring closely. Early engagement with the environmental regulator and local planning authority is essential. Feedstock security. Reliable, contracted tyre supply at predictable cost underpins any business case. Relationships with collectors and processors matter as much as reactor design. Product specification. Offtake agreements for oil and carbon black should be pursued early, with clear quality standards. Community acceptance. Thermal technologies attract public scrutiny. Transparent communication about emissions, traffic, and safety builds trust. Technology choice. Batch, semi-continuous, and continuous systems differ significantly in throughput, maintenance demands, and capital cost. Independent due diligence on reference plants is well worth the investment. Policy Tailwinds Broader trends favour recycling routes that return materials to the economy. Resource-efficiency goals, continuing discussion of producer responsibility approaches for tyres, and industry commitments to recycled content all point toward growing demand for verified, traceable secondary materials. Tyre manufacturers and fleet operators increasingly want demonstrable end-of-life solutions, and pyrolysis can offer a credible story when supported by robust carbon accounting and certification. Looking Ahead The tyre landfill ban solved one problem and created another: what to do with half a million tonnes of durable, high-energy material each year. Pyrolysis offers a technically proven answer, but success depends on execution. That means disciplined feedstock sourcing, realistic financial modelling, high-quality outputs, and open engagement with regulators and communities. For investors, waste operators, and technology providers, the message is encouraging. As the UK tightens its approach to waste and raises its circular-economy ambitions, a well-run pyrolysis plant UK projects can build is well placed to turn a regulatory constraint into a durable commercial opportunity.
